
The production of heavy-section ductile iron castings, such as hubs, presents significant challenges in foundry practice. Defects like shrinkage cavities and porosity are prevalent due to the extended solidification time and the associated difficulty in feeding the last areas to freeze. While traditional green sand molding is commonly employed, it often suffers from high scrap rates, low efficiency, and elevated costs for such components. This article details a comprehensive process optimization undertaken to successfully produce a QT500-7 ductile iron hub using the lost foam casting process, which offered a promising alternative for improved yield and dimensional consistency.
The target component was a wheel hub with a mass of 120 kg and major dimensions of Ø556 mm x 414.5 mm. Its average wall thickness was approximately 12 mm, with localized thicker sections. The material specification required a hardness range of 170-230 HB after a normalizing and tempering heat treatment, an elongation exceeding 7%, and a sound casting free from internal shrinkage defects. The initial trials using conventional methods highlighted the susceptibility of this geometry to shrinkage-related issues, prompting the shift to lost foam casting process development.
1. Component Analysis and Foundry Constraints
The first step in any lost foam casting process design is analyzing the component geometry and the constraints imposed by the process itself. A critical constraint in lost foam casting is the need for the pattern cluster to be oriented to allow unhindered sand flow during filling and compaction. For this hub, the only viable orientation was with the large open face facing upwards. This fixed the casting position, and the primary task became determining the optimal gating system to ensure complete filling, controlled pyrolysis gas evolution, and, most critically, adequate feeding to prevent shrinkage.
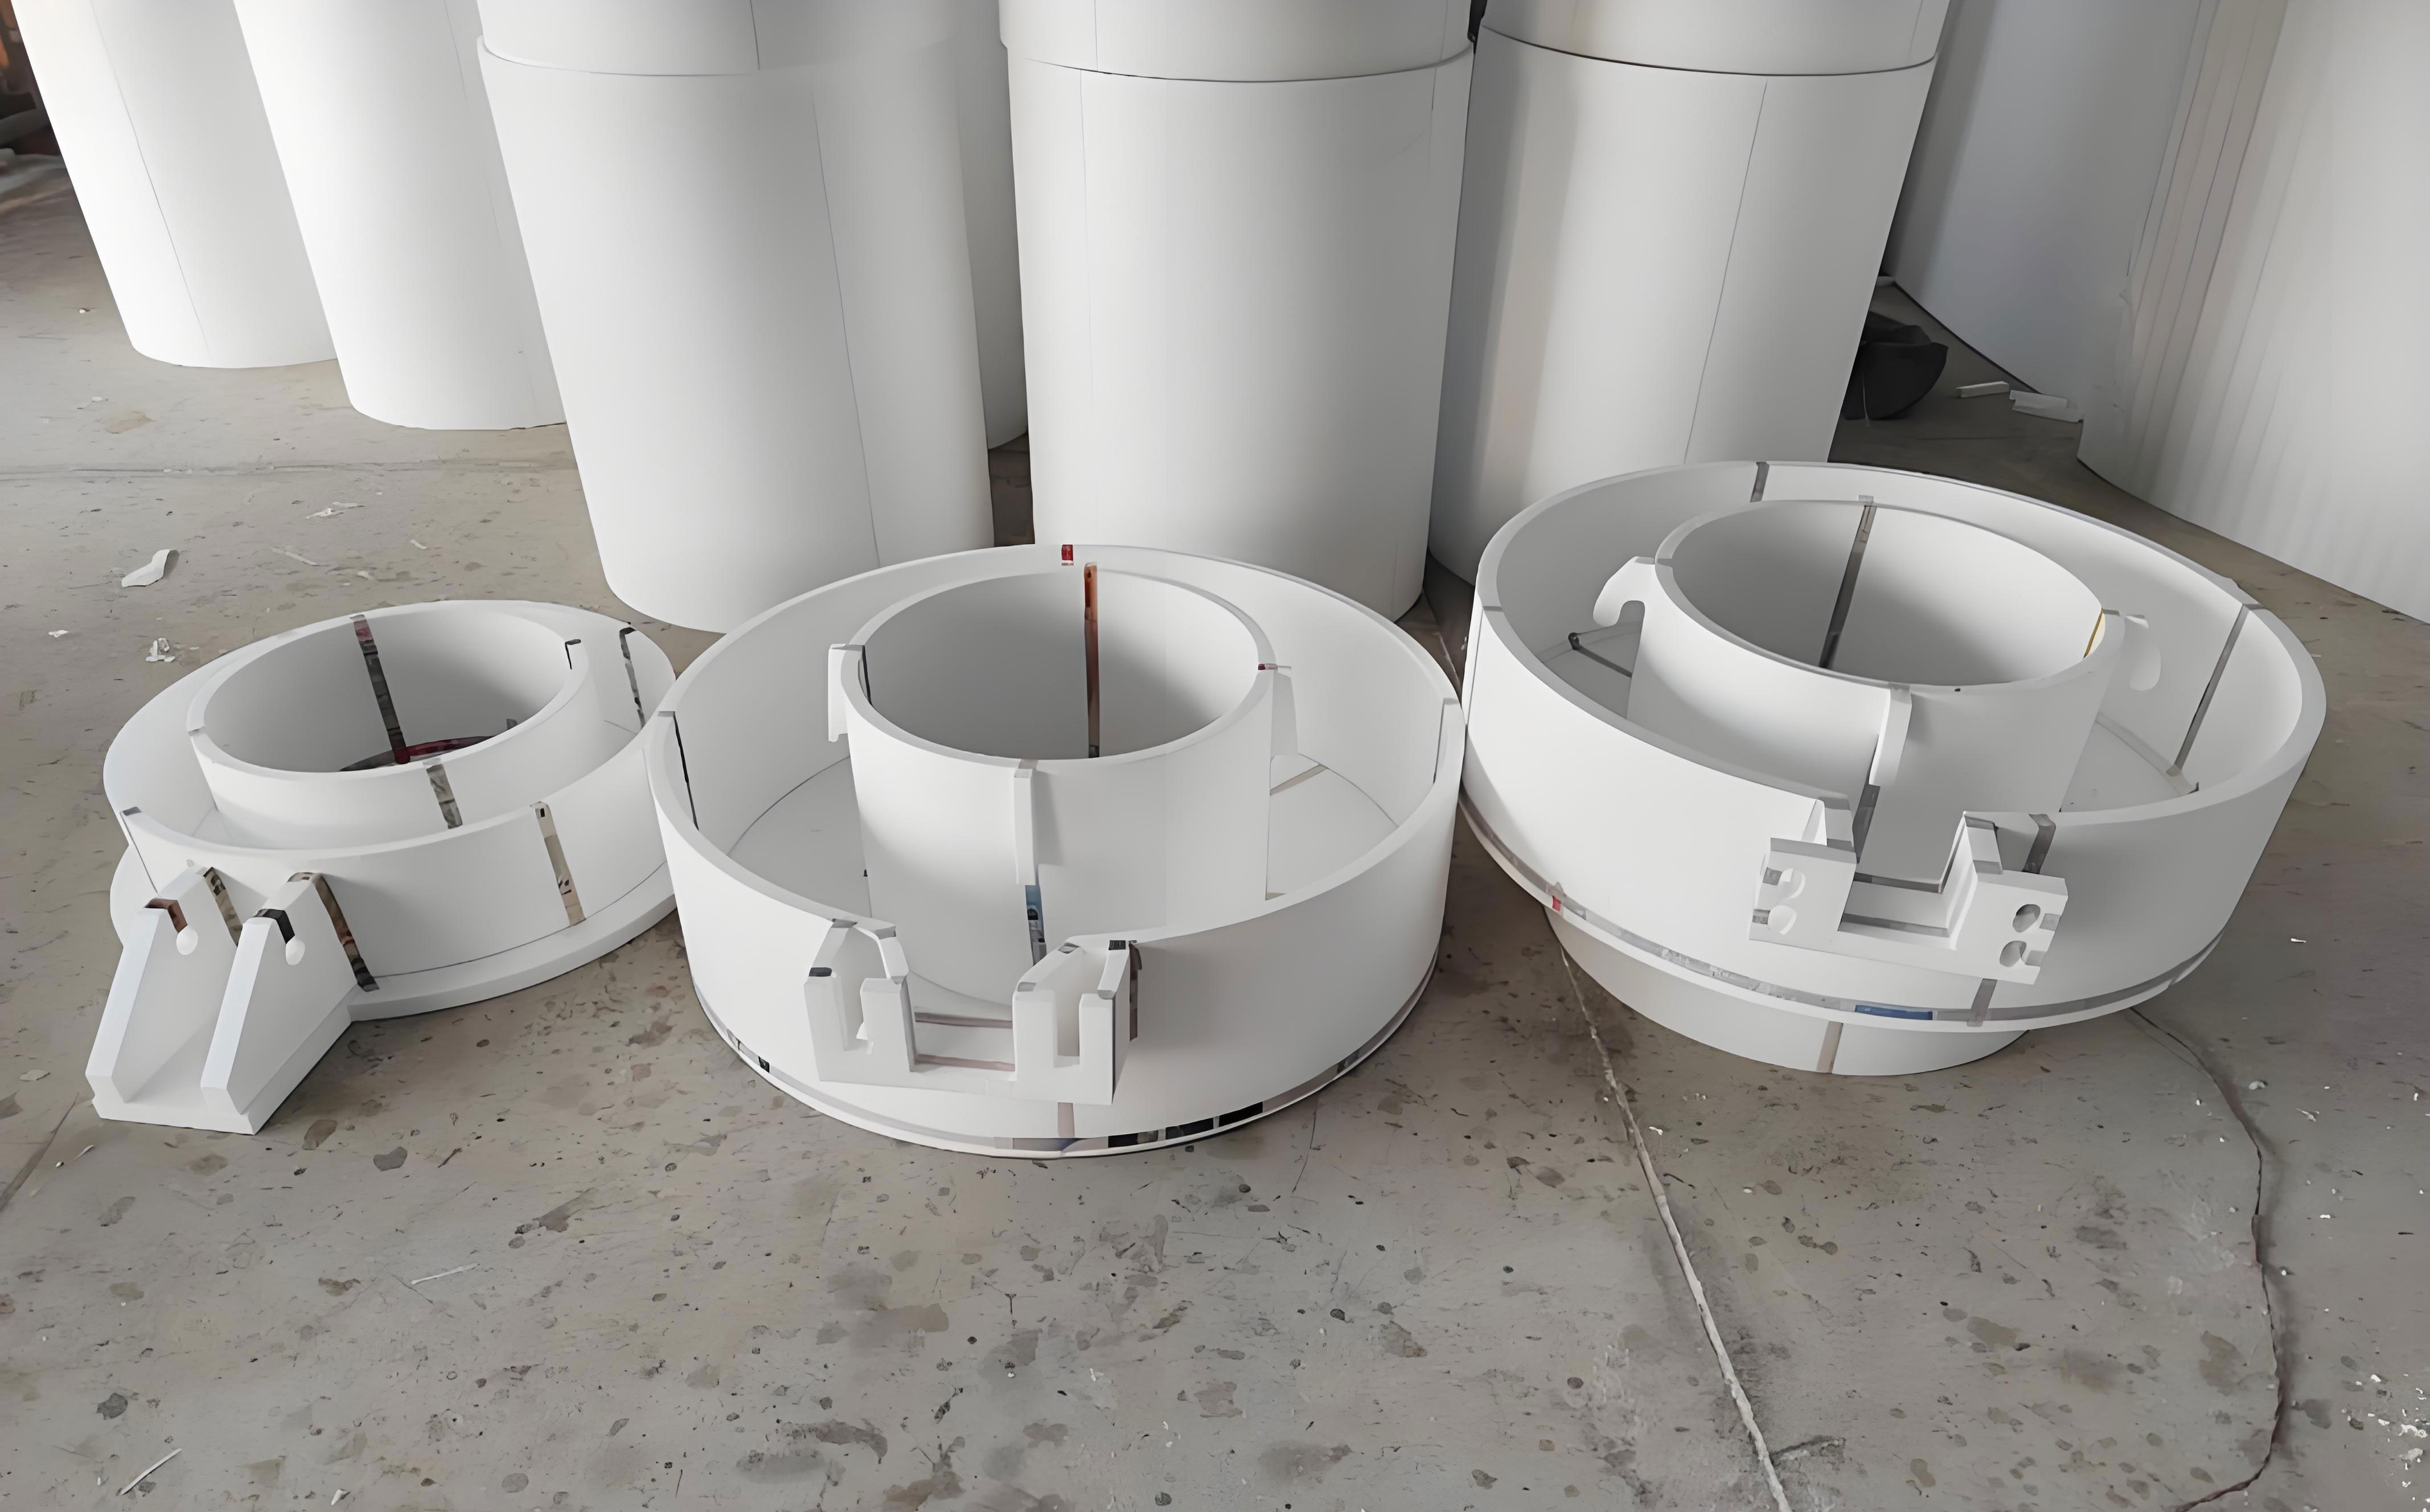
Analyzing the cross-section reveals the feeding challenge: the upper flange and central barrel sections are substantial thermal masses. Solidification will inevitably progress from the thinner walls towards these thicker sections, creating isolated hot spots that are prone to shrinkage if not properly fed. Several initial gating concepts were evaluated theoretically:
- Top Gating: Directly pouring onto the large top surface. This was quickly discarded due to the high risk of violent recoil or “back-pressure” as the descending metal front confronts a large volume of rapidly evolving foam pyrolysis gases traveling upwards. Furthermore, the long flow distance across the Ø443 mm top diameter could lead to cold shuts and unstable filling.
- Gating at the Outer Diameter of the Mid-Flange: Introducing metal around the Ø556 mm outer rim. While this avoids direct gas confrontation, the flow path to the opposite side is extremely long, creating a high probability of cold shuts and leaving the top section as a last-to-fill, poorly-fed area.
- Gating at the Inner Diameter (Bore): Introducing metal at several points around the Ø202 mm inner circle. This offers a shorter, more controlled flow path for filling the lower and central sections. However, the top flange remains a distant, heavy section that may solidify last and develop shrinkage.
- Bottom Gating: While generally promoting calm filling, the presence of internal recesses and thinner sections at the base would slow the initial rise of metal, potentially leading to mistruns and increasing the risk of shrinkage in the main body as the feeding path becomes long and tortuous.
Based on this analysis, the concepts of gating at the outer mid-flange and the inner bore were selected for experimental trials. The rationale was that while both might leave the top flange at risk, this area was a machining face, allowing for the strategic placement of feeding risers that could be removed during machining, effectively transferring the potential defect to a disposable part of the casting.
2. Detailed Process Design and Rationale
The process design for lost foam casting requires careful calculation of gating dimensions, riser placement, and process parameters to manage foam decomposition, metal flow, and solidification.
2.1 Gating System Design
The gating system must be sized to achieve a rapid but controlled fill to avoid excessive foam gas generation and to ensure thermal gradient conducive to directional solidification. The initial fill rate is estimated using the Bernoulli-Oszin (or Osann) equation, adjusted for the flow resistance of the foam and, in our case, a ceramic foam filter. For ductile iron, a typical reduction in effective flow area of 40-60% is assumed due to the filter and the back-pressure from foam decomposition.
The basic governing equation for metal flow can be simplified for initial sizing:
$$ A_g = \frac{W}{\rho \cdot t \cdot C_d \cdot \sqrt{2gH}} $$
Where:
$A_g$ = Required total choke area (typically the ingate area, m²)
$W$ = Casting weight (kg)
$\rho$ = Liquid metal density (for iron, ~7000 kg/m³)
$t$ = Desired fill time (s)
$C_d$ = Discharge coefficient (accounts for filter & foam, ~0.3-0.5 for lost foam)
$g$ = Acceleration due to gravity (9.81 m/s²)
$H$ = Effective metallostatic head (m)
For a heavy-section casting like the hub, a fill time (t) of 45-55 seconds was targeted to balance gas evolution and heat loss. Based on calculations, a sprue diameter of 50 mm (area ≈ 1960 mm²) was chosen. Following established ratios for heavy ductile iron gating (often 1.5 : 2 : 1 for Ingate : Runner : Sprue areas), the total ingate area was determined to be approximately 2450-2820 mm².
2.2 Two Experimental Designs
Design A: Four Gates on Outer Mid-Flange
The total ingate area was divided into four gates equally spaced around the Ø556 mm flange, each with an area of ~700 mm². To address the anticipated shrinkage in the top flange, ten small blind risers (20 x 100 x 100 mm) were placed on the top surface. The intent was for these risers to provide liquid feed and act as hot-spots to draw solidification.
Design B: Four Gates on Inner Bore
The total ingate area (~2820 mm²) was divided into four gates equally spaced around the Ø202 mm inner bore. This promoted very stable filling of the central core and lower sections. Anticipating the top flange as the last-to-solidify zone, four larger tapered risers were placed on the top surface. The risers were designed with a smaller contact neck (Ø40 mm) for easy removal and a larger body (Ø80 mm x 120 mm) to provide adequate feed metal volume and prolonged thermal activity.
| Design | Gating Location | Number of Ingates | Total Ingate Area (mm²) | Riser Strategy | Theoretical Advantage | Potential Risk |
|---|---|---|---|---|---|---|
| A | Outer Mid-Flange (Ø556mm) | 4 | ~2800 | 10 small top risers | Direct feeding to mid-section | Long flow to opposite side, cold shuts, top shrinkage |
| B | Inner Bore (Ø202mm) | 4 | ~2820 | 4 larger tapered top risers | Stable fill, good thermal gradient for lower section | Top flange remains a feeding challenge |
2.3 Process Parameter Window
Critical parameters for the lost foam casting process were established based on experience with ductile iron:
- Pouring Temperature: 1450°C – 1490°C. A higher temperature within this range improves fluidity for complete filling but increases the total heat to be removed during solidification, affecting shrinkage behavior.
- Vacuum Level: -0.06 to -0.08 MPa. Sufficient vacuum is required to counter gas pressure from foam decomposition and prevent mold wall movement (scabbing/expansion). Excessive vacuum increases sand compactness and can lead to severe metal penetration and burn-on.
- Pattern Material: Expanded Polystyrene (EPS) or Co-Polymer foam with a density of ~20-25 g/L to ensure adequate strength and a controlled gas evolution rate.
The solidification time ($t_f$) for a section in a sand mold can be estimated by Chvorinov’s rule, which is particularly relevant for anticipating feeding requirements:
$$ t_f = B \cdot \left( \frac{V}{A} \right)^n $$
Where:
$t_f$ = Local solidification time (s)
$V$ = Volume of the section (m³)
$A$ = Surface area of the section (m²)
$B, n$ = Mold constants (For sand molds, n is often ~2)
Calculating the modulus ($V/A$) for the top flange versus the thinner walls clearly shows why the flange solidifies last and requires feeding. The risers must have a larger modulus than the section they are intended to feed.
3. Experimental Trials and Results
3.1 First Trial Series
Three castings were poured for each gating design (A and B). Parameters were set at the upper range: pouring temperature ~1500°C, vacuum at -0.06 MPa. Holding times under vacuum after pouring were varied at 8, 9, and 10 minutes.
Results for Design A (Outer Flange Gating):
The castings exhibited severe defects. The area diametrically opposite the ingates showed extensive folds/cold shuts and internal shrinkage porosity. This confirmed the risk of the long flow path and poor thermal gradient. The multiple small risers were ineffective in feeding the large, isolated hot spot.
Results for Design B (Inner Bore Gating):
The castings showed significantly better integrity. The lower and central sections were sound. As predicted, the primary area of concern was the top flange, but the larger risers showed evidence of feeding action. One casting from the 8-minute hold showed minor mold wall expansion (“lift”), indicating possible early vacuum release.
This trial conclusively eliminated Design A. Design B showed promise, and an 8-minute hold time was provisionally selected to optimize cycle time while preventing lift.
3.2 Second Trial Series & Parameter Optimization
Focusing solely on Design B (inner bore gating), a larger batch was produced to refine parameters and solve initial issues like mild burn-on. The pouring temperature was lowered to 1460-1480°C, and vacuum control was tightened. A “slow-fast-slow” pouring sequence was implemented: initial slow pour to establish the metal front in the sprue and avoid turbulence, a fast fill to complete most of the cavity, and a final slow pour to top off the risers.
| Parameter | Optimized Value / Range | Purpose / Effect |
|---|---|---|
| Gating Design | Design B: 4 gates on Ø202mm bore | Stable filling, establishes favorable thermal gradient. |
| Riser Design | 4 tapered risers (Ø40 neck / Ø80 body) | Provides effective feed metal volume to top flange hot spot. |
| Pouring Temperature | 1470°C ± 10°C | Balances fluidity for filling with reduced total heat load. |
| Vacuum Level | -0.07 MPa ± 0.01 | Prevents mold wall movement & scabbing; minimizes burn-on. |
| Pouring Time | 48 ± 2 seconds | Controlled fill rate to manage foam gas evolution. |
| Post-Pour Vacuum Hold | 8 minutes | Ensures casting solidification under pressure, prevents lift. |
| In-Mold Time | > 60 minutes | Ensures complete solidification before shakeout. |
The results from this optimized batch were excellent. Visual inspection and non-destructive testing showed no signs of cold shuts or surface defects. Destructive sectioning of sample castings confirmed the absence of internal shrinkage cavities or porosity in the critical load-bearing sections. The risers showed significant shrinkage cavities internally, proving they functioned correctly as feeders.
4. Metallurgical Control: Achieving QT500-7 Properties
The success of a lost foam casting is not only geometrical but also metallurgical. The QT500-7 grade requires a pearlitic-ferritic matrix to achieve its strength (500 MPa UTS) while retaining good elongation (>7%). Composition control is paramount, especially given the slower cooling inherent in the unbonded sand mold of the lost foam casting process, which promotes ferrite formation.
The target chemistry was set to ensure proper graphitization, matrix control, and hardenability. Key elements and their roles are summarized below, with the final optimized range.
| Element | Target Range (wt.%) | Metallurgical Rationale |
|---|---|---|
| Carbon (C) | 3.5 – 3.7 | High carbon ensures adequate graphite precipitation, improving castability, feeding, and damping capacity. Uses high-purity graphite-based inoculants. |
| Silicon (Si) | 2.5 – 2.7 | Strong graphitizer, promotes ferrite. Balance is critical: too low risks carbide formation; too high excessively hardens ferrite and reduces ductility. |
| Manganese (Mn) | 0.40 – 0.50 | Stabilizes pearlite and strengthens the matrix. Essential for achieving the required hardness and strength in the slower-cooling lost foam casting. |
| Copper (Cu) | 0.30 – 0.35 | Mild pearlite promoter, improves uniformity of properties throughout the heavy section without significantly impacting machinability. |
| Phosphorus (P) | < 0.08 | Impurity kept low to avoid the formation of brittle phosphide eutectics at grain boundaries. |
| Sulfur (S) | < 0.03 | Kept very low to minimize the consumption of magnesium during treatment and to reduce the risk of sulfide-induced dross. |
| Magnesium (Mg)res | 0.035 – 0.050 | Residual after treatment. Critical for spheroidization of graphite. Tight control prevents degenerate graphite forms (e.g., vermicular, flake). |
The nodularity and nodule count are critical quality metrics. The relationship between cooling rate (affected by section thickness and mold media) and nodule count ($N_v$) can be described empirically. For heavy-section lost foam castings:
$$ N_v \propto \frac{1}{t_f} \cdot [\text{Inoculation Potency}] $$
Where a longer local solidification time ($t_f$) generally leads to a lower nodule count. Effective late-stream inoculation is therefore crucial to ensure a high enough nodule count even in thick sections, which refines the matrix and improves mechanical properties. The final castings consistently achieved a graphite nodularity >85% (Grade 1-2) and a nodule count suitable for the section size.
Heat treatment (normalizing at ~900°C followed by tempering at ~600°C) was applied to standardize the matrix microstructure, relieve residual stresses from the lost foam casting process, and achieve the final hardness specification of 180-210 HB. Elongation values measured from separately cast test bars exceeded 9%.
5. Conclusion
The production of a heavy-section QT500-7 ductile iron hub via the lost foam casting process was successfully realized through systematic process design and optimization. The key conclusions are:
- Gating Strategy is Paramount: For this closed-top geometry, gating at the inner bore provided a stable fill pattern and established a thermal gradient where the top flange, though last to solidify, could be effectively fed by strategically designed risers. Gating on wide external features led to uncontrolled flow and defective castings.
- Integrated Riser Design: Risers in lost foam casting must be explicitly designed to feed specific thermal centers. Their size, location, and connection (neck) are calculated based on the modulus principle, and they must be considered an integral part of the expendable pattern cluster.
- Process Parameter Synergy: Optimal results were achieved with a specific synergy of moderate pouring temperature (~1470°C), controlled vacuum (~ -0.07 MPa), a defined fill sequence, and a sufficient post-pour holding time. This combination minimized gas-related defects, controlled mold rigidity, and ensured sound solidification.
- Metallurgical Consistency: Achieving the required mechanical properties in a slower-cooling lost foam casting requires precise chemistry control, with deliberate use of pearlite-stabilizing elements like Mn and Cu, coupled with effective inoculation to ensure high graphite nodularity throughout the heavy section.
This case study demonstrates that the lost foam casting process is a viable and competitive method for producing complex, heavy-section ductile iron components. Its success hinges on a holistic approach that seamlessly integrates foam pattern design, gating and feeding principles derived from traditional foundry practice, and precise control over metallurgical and process variables. The ability to produce near-net-shape castings with minimal draft and core assembly requirements offers significant advantages in machining cost and dimensional consistency for parts like hubs.