
In my experience as an engineer specializing in advanced casting techniques, the lost foam casting process has revolutionized the production of complex components like slurry pump impellers. This method, particularly for high-chromium cast iron materials such as KmTBCr26, offers significant advantages over traditional sand casting. The lost foam casting process eliminates the need for cores and complex mold assembly, ensuring dimensional consistency and near-net shape capabilities. Throughout this article, I will delve into the technical intricacies of applying the lost foam casting process to manufacture thick-walled, abrasion-resistant impellers, emphasizing key parameters, quality control measures, and outcomes. The repeated focus on the lost foam casting process underscores its critical role in achieving superior casting quality.
The impeller is a core component in slurry pumps, operating under severe abrasive conditions. The material of choice, high-chromium white iron (e.g., KmTBCr26), possesses excellent wear resistance and hardness after heat treatment, typically reaching 58-62 HRC. However, its casting properties are challenging: poor fluidity, high melting and pouring temperatures, significant shrinkage, and low thermal conductivity. Traditional sand casting often results in issues like mold misalignment, poor surface finish, and inconsistent wall thickness, leading to variable hydraulic performance. In contrast, the lost foam casting process mitigates these problems through its unique approach of using expendable foam patterns and negative pressure pouring.
From a first-person perspective, I have overseen numerous projects where the lost foam casting process was implemented. One notable case involved a small impeller with an outer diameter of 420 mm, height of 130 mm, five twisted blades with a maximum thickness of 26.8 mm, and cover plates of 20 mm thickness. The technical requirements demanded sound castings free from defects like porosity and shrinkage, post-heat treatment hardness of 58-62 HRC, and static balance with unbalance mass ≤45 g at the maximum diameter. Meeting these specs with traditional methods was arduous, but the lost foam casting process provided a streamlined solution.
Process Parameter Design in Lost Foam Casting
The foundation of a successful lost foam casting process lies in meticulous parameter design. For this impeller, I prioritized several aspects. First, the threaded blind holes on the hub were designed as solid structures to facilitate riser placement and enable cluster molding for improved yield. Machining allowances were set at 3 mm for primary surfaces and 1 mm for inspection areas. The shrinkage rate is a critical factor, combining foam dehydration shrinkage and metallic contraction. The total linear shrinkage for high-chromium iron in the lost foam casting process can be expressed as:
$$ S_{total} = S_{foam} + S_{metal} $$
where \( S_{foam} \) is the foam drying shrinkage (0.3–0.5%) and \( S_{metal} \) is the solidification shrinkage of high-chromium iron (approximately 2.0–2.2%). Thus, the overall shrinkage ranges from 2.4% to 2.6%. This must be accounted for in pattern dimensions. To optimize feeding, riser design followed principles for malleable iron, considering thermal nodes. The hub’s hot spot diameter was 99 mm, so the riser neck diameter was calculated as \( 0.7 \times 99 = 69.3 \, \text{mm} \), rounded to 70 mm. The riser diameter, based on a factor of 2.5 and adjusted for vacuum cooling effects, was determined as:
$$ D_{riser} = 2.5 \times D_{neck} \times 1.1 = 2.5 \times 70 \times 1.1 = 192.5 \, \text{mm} \approx 200 \, \text{mm} $$
This ensures adequate补缩 in the lost foam casting process. Table 1 summarizes key parameters.
| Parameter | Value | Remarks |
|---|---|---|
| Machining Allowance (main) | 3 mm | Ensures finish machining |
| Machining Allowance (inspection) | 1 mm | Minimizes material removal |
| Foam Shrinkage (S_foam) | 0.3–0.5% | EPS dehydration |
| Metal Shrinkage (S_metal) | 2.0–2.2% | High-Cr iron solidification |
| Total Shrinkage (S_total) | 2.4–2.6% | Applied to pattern |
| Riser Neck Diameter | 70 mm | Based on hot spot |
| Riser Diameter | 200 mm | Adjusted for vacuum effect |
EPS Pattern Fabrication for Lost Foam Casting
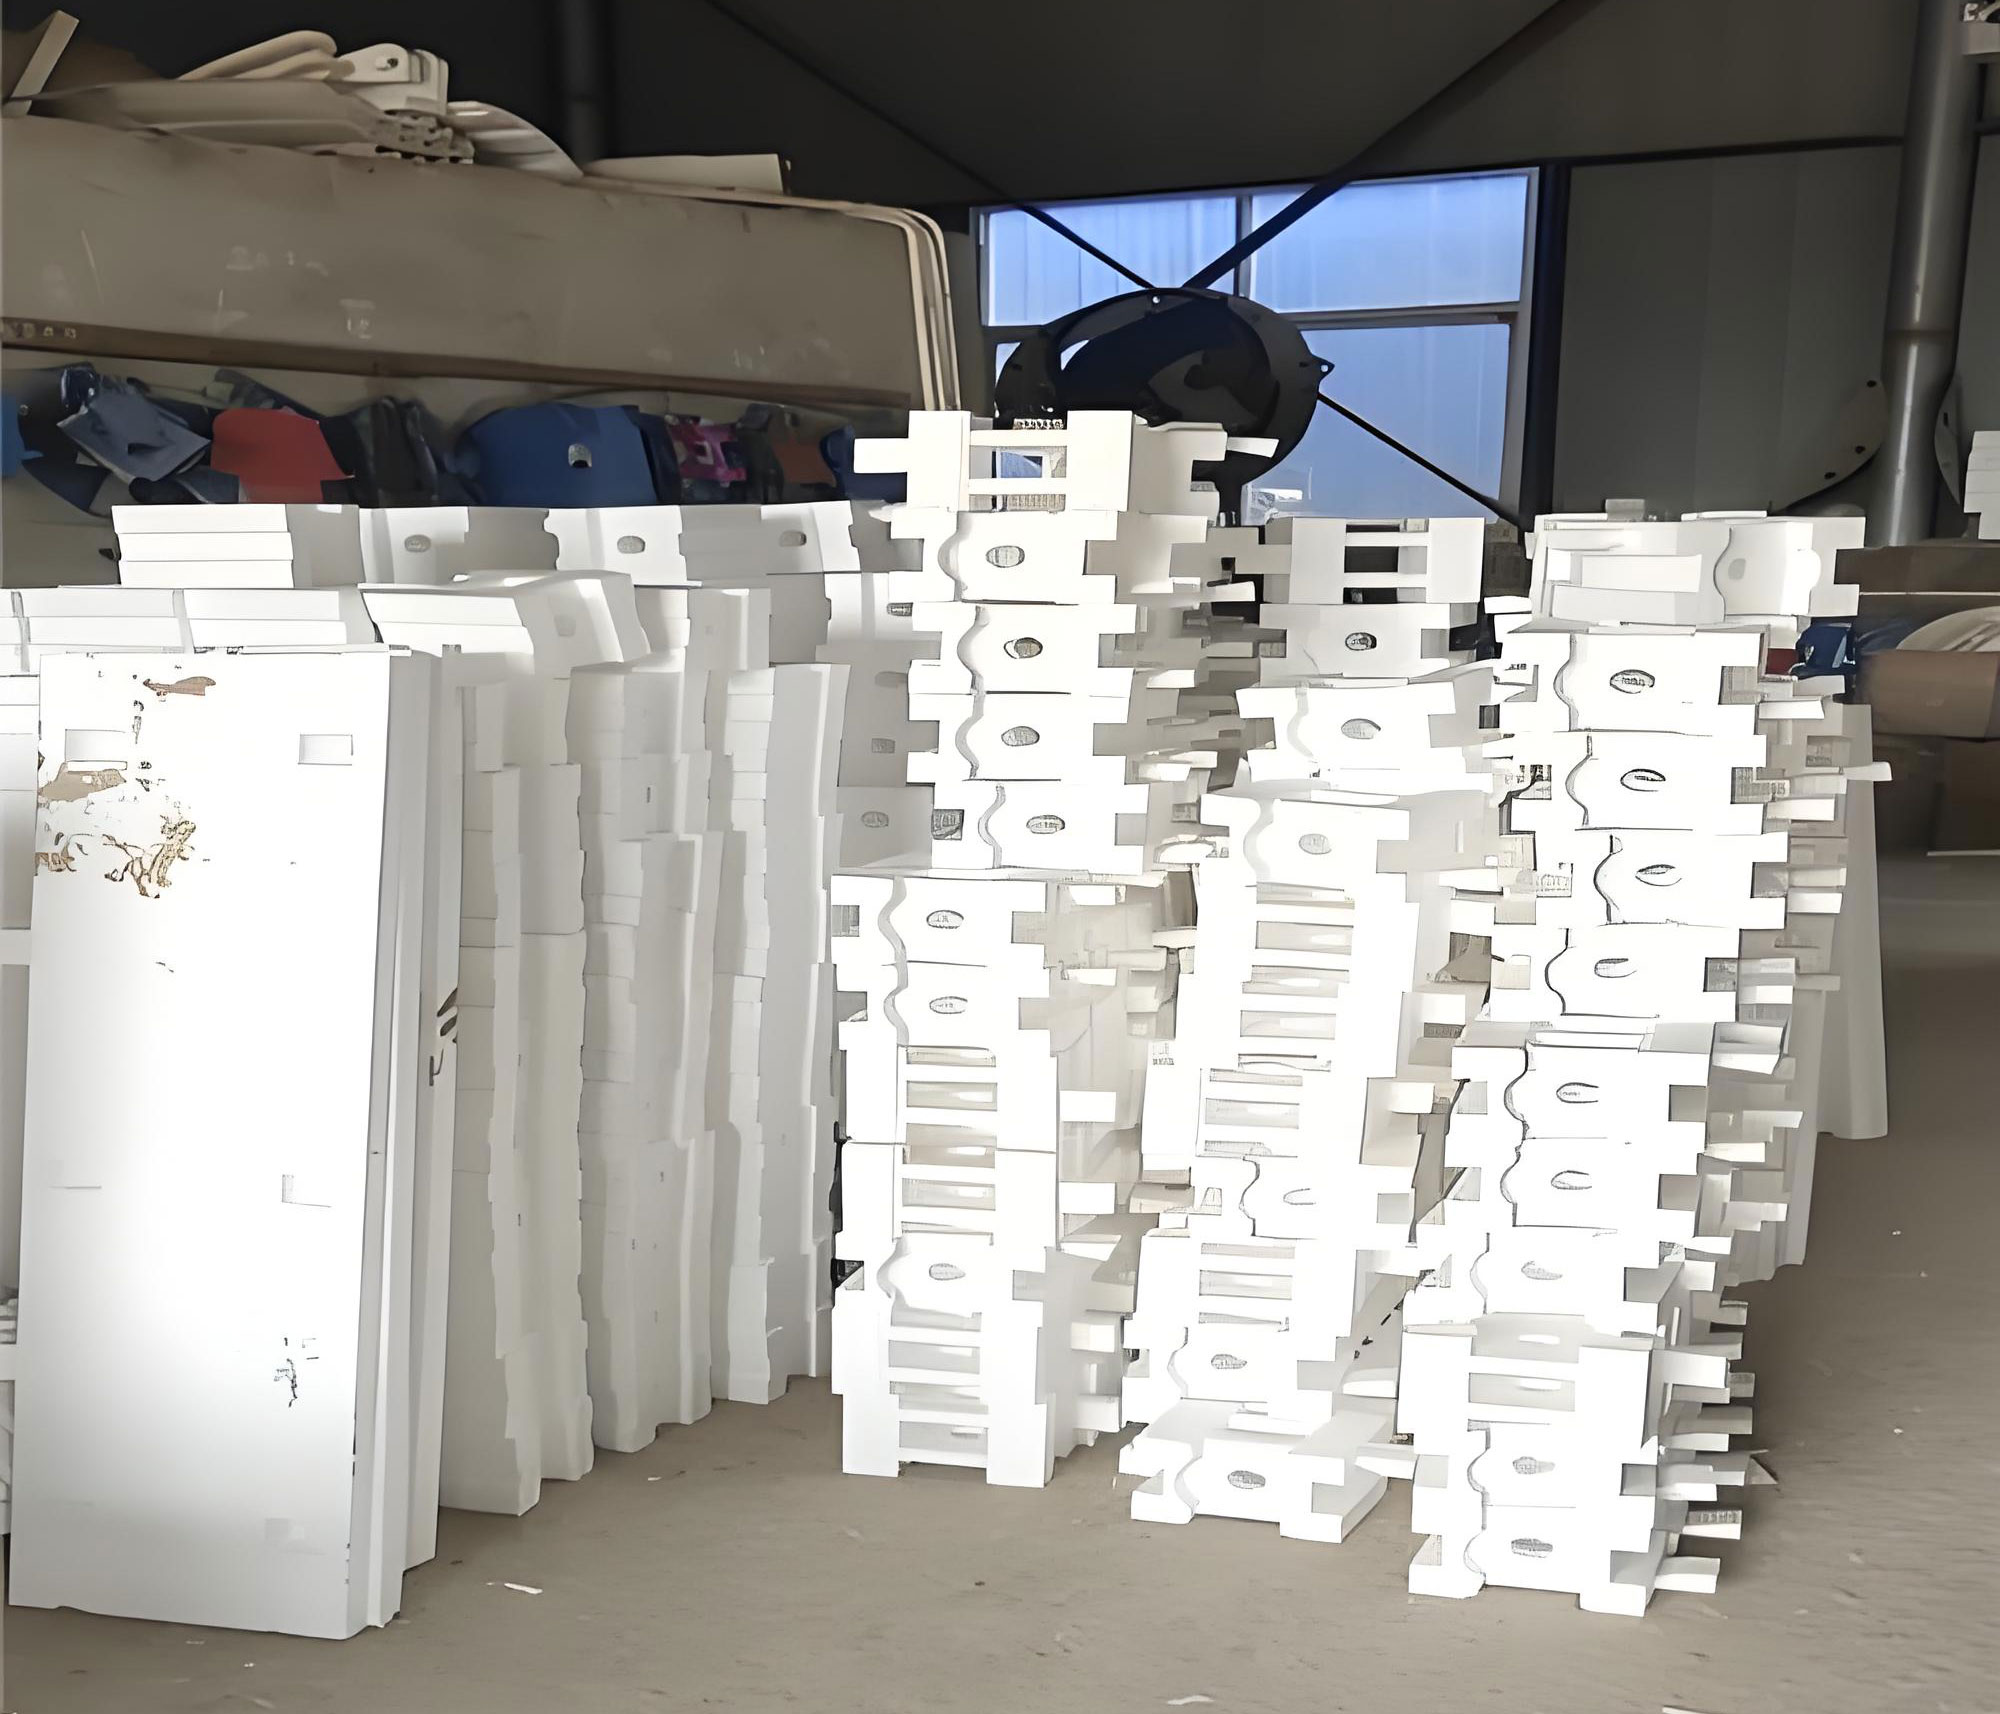
The lost foam casting process relies heavily on precise foam patterns. Given the impeller’s complex geometry with twisted blades, a multi-piece pattern approach was necessary. I used two EPS (expanded polystyrene) pattern segments molded separately and then bonded. The parting line incorporated locator pins and sockets to ensure alignment. The foam material was medium-grade EPS with an initial particle size of 0.6–0.8 mm. After pre-expansion via electric heating, the bead size reached 2.8–3.2 mm, and the bulk density was controlled at approximately 0.022 g/cm³. This density balances rigidity and surface smoothness, crucial for the lost foam casting process. The relationship between bead expansion and density can be described by:
$$ \rho = \frac{m}{V} \approx \frac{m_0}{\left( \frac{d}{d_0} \right)^3} $$
where \( \rho \) is the expanded density, \( m_0 \) is initial mass, \( d_0 \) is initial bead diameter, and \( d \) is expanded diameter. For our case, \( d/d_0 \approx 4 \), yielding low density. During molding, steam pressure and heating time were tuned to avoid under-fusion or deformation, especially in thin sections like blade edges. After demolding, patterns were carefully handled to prevent distortion, a common pitfall in the lost foam casting process.
Cluster Assembly and Gating System Design in Lost Foam Casting
A hallmark of the lost foam casting process is the ability to form pattern clusters for efficient pouring. For this impeller, I designed a cluster with one central riser feeding three impellers in series, enhancing yield. Each impeller was attached via a downsprue neck to the riser, and additional venting/ slag collectors were placed on the cover plates. The cluster orientation was optimized to avoid ” concave” regions that could hinder sand filling. Figure 1 illustrates a typical cluster setup in the lost foam casting process.
The gating system was integrated into the riser, with metal entering laterally. The riser volume was calculated to ensure adequate feeding. For high-chromium iron, the modulus method can be applied. The modulus (volume-to-surface area ratio) of the hub section was approximately 0.025 m, requiring a riser modulus about 1.2 times larger. The final riser dimensions (200 mm diameter × 300 mm height) provided a safety factor. The negative pressure during pouring in the lost foam casting process enhances metal flow, which can be modeled using Bernoulli’s principle under vacuum:
$$ P_1 + \frac{1}{2} \rho v_1^2 + \rho g h_1 = P_2 + \frac{1}{2} \rho v_2^2 + \rho g h_2 – \Delta P_{vac} $$
where \( \Delta P_{vac} \) is the vacuum pressure (0.04–0.055 MPa), aiding filling. Cluster assembly used specialized adhesives to bond patterns, ensuring integrity during coating and sand filling.
Coating Application and Drying in Lost Foam Casting
The coating is vital in the lost foam casting process, serving as a barrier between the foam and sand, providing permeability for gas escape, and resisting metal penetration. I selected a water-based coating with zircon flour and alumina as primary refractories, suitable for high-chromium iron’s acidic nature and high pouring temperatures (~1500°C). The coating slurry’s viscosity and thickness were controlled to achieve a uniform layer. The coating process involved dipping, pouring, and brushing, resulting in a thickness of about 1.5 mm on patterns and >2.5 mm on risers. The coating’s permeability \( K \) can be expressed as:
$$ K = \frac{C \cdot \phi^3}{ (1-\phi)^2} $$
where \( \phi \) is porosity and \( C \) is a constant. Higher permeability reduces gas defects. After coating, the cluster was dried in a convective oven at 50±5°C for 8–10 hours per layer, with humidity below 30%. Drying kinetics follow Fick’s law of diffusion, removing moisture without pattern warping. Proper drying is critical in the lost foam casting process to prevent steam explosions during pouring. Table 2 compares coating properties.
| Coating Property | Target Value | Importance in Lost Foam Casting |
|---|---|---|
| Viscosity | 40-50 sec (Ford cup #4) | Ensures even coverage |
| Solid Content | 65-70% | Affects layer thickness |
| Permeability | >15 GPU | Facilitates gas evacuation |
| Thermal Stability | Up to 1600°C | Withstands iron temperature |
| Drying Time | 8-10 h/layer | Prevents cracks and humidity |
Molding Sand Selection and Pouring Control in Lost Foam Casting
Initially, I used silica sand for molding in the lost foam casting process, but encountered issues like collapse and burn-on in thin passages. This was due to poor flowability and packing in complex geometries. Switching to spherical ceramsite sand (宝珠砂) improved results dramatically. Its round particles offer better flow and compaction, described by the angle of repose \( \theta \):
$$ \tan \theta = \frac{2h}{d} $$
For spherical sand, \( \theta \) is lower, enhancing fill. The sand’s thermal conductivity also affects cooling; ceramsite has lower conductivity, reducing thermal shock. For the lost foam casting process, sand properties are summarized in Table 3.
| Sand Type | Particle Shape | Angle of Repose | Thermal Conductivity (W/m·K) | Suitability for Lost Foam |
|---|---|---|---|---|
| Silica Sand | Angular | 30-35° | 1.5-2.0 | Poor in complex shapes |
| Ceramsite Sand | Spherical | 20-25° | 0.8-1.2 | Excellent, minimizes defects |
Pouring was conducted using medium-frequency melted iron at a tapping temperature of 1550°C. Final deoxidation was done with Si-Al alloy added at 2–2.5‰ of iron weight. The pouring temperature was controlled at 1470–1500°C, and negative pressure maintained at 0.04–0.055 MPa during pouring. The pouring rate followed a “slow-fast-slow” sequence to avoid backlash and sand displacement. After pouring, vacuum was reduced to 0.02–0.03 MPa for 10–15 minutes to allow controlled solidification. The heat transfer during solidification in the lost foam casting process can be modeled using Fourier’s law:
$$ q = -k \frac{dT}{dx} $$
where \( q \) is heat flux, \( k \) is thermal conductivity of sand/metal, and \( \frac{dT}{dx} \) is temperature gradient. Proper control minimizes shrinkage porosity.
Results and Analysis of Lost Foam Casting Application
Implementing the lost foam casting process yielded impressive outcomes. Castings exhibited smooth surfaces, precise dimensions, and dense internal structures without gas holes or slag inclusions. Hardness after normalizing consistently reached 60-62 HRC. Static balance unbalance mass was 60-70 g, easily corrected by light grinding to meet the ≤45 g requirement. In contrast, traditional sand castings showed higher unbalance (120-180 g), requiring milling for correction. The superiority of the lost foam casting process is evident in Table 4.
| Aspect | Lost Foam Casting Process | Traditional Sand Casting |
|---|---|---|
| Surface Finish | Smooth, near-net shape | Rough, requires more machining |
| Dimensional Consistency | High, minimal variation | Variable due to mold assembly |
| Internal Defects | Negligible porosity/shrinkage | Prone to gas and slag |
| Hardness Uniformity | 60-62 HRC, stable | 58-62 HRC, less consistent |
| Balance Unbalance Mass | 60-70 g (easily corrected) | 120-180 g (requires heavy correction) |
| Process Yield | High due to clustering | Lower, single-piece molding |
The microstructural integrity achieved through the lost foam casting process can be attributed to the vacuum-assisted filling and controlled cooling. The absence of cores eliminates core shift errors, ensuring uniform wall thickness. Moreover, the carbon pick-up typical in lost foam casting is negligible for high-chromium iron due to its high base carbon content (2.0–3.3%), preserving material properties.
Conclusion on Lost Foam Casting Process Efficacy
In summary, the lost foam casting process proves highly effective for manufacturing high-chromium iron impellers. Through careful design of parameters, pattern fabrication, cluster assembly, coating, and pouring control, I have achieved castings with excellent quality and consistency. The process leverages negative pressure to enhance metal flow, reduces reliance on cores, and enables efficient multi-piece production. For industries requiring complex, wear-resistant components, adopting the lost foam casting process offers tangible benefits in precision, efficiency, and cost-effectiveness. Future work could explore optimization via simulation software to further refine riser design and pouring parameters. Nonetheless, the success demonstrated here validates the lost foam casting process as a robust solution for advanced casting challenges.