
As a researcher in the field of metal casting, I have always been fascinated by the challenges and opportunities presented by complex geometries, particularly in shell castings. These components are critical in various industries, such as aerospace and automotive, due to their lightweight and high-strength properties. In this study, I focus on aluminum alloy shell castings, which are prone to defects like shrinkage and porosity during sand casting. To address this, I employ numerical simulation tools to analyze and optimize the casting process. The use of AnyCasting software allows for a detailed investigation of fluid flow, solidification, and defect formation. Through this work, I aim to demonstrate how simulation-driven design can enhance the quality and yield of shell castings, reducing scrap rates and improving efficiency. This article details my methodology, from 3D modeling to optimization, and presents findings that underscore the importance of iterative process refinement in modern foundry practices.
The first step in my analysis involved creating a precise 3D model of the aluminum alloy shell casting. Using UG software, I developed a digital representation of the component, which has overall dimensions of 295 mm × 262 mm × 159 mm. The geometry is intricate, with varying wall thicknesses ranging from 8 mm at the beams to 24 mm at the lug areas. This complexity is common in shell castings, where internal cavities and thin sections pose significant challenges for defect-free production. The model serves as the foundation for all subsequent simulations, ensuring accuracy in predicting material behavior. Below, I include a visual reference for the shell casting model, which highlights its key features.
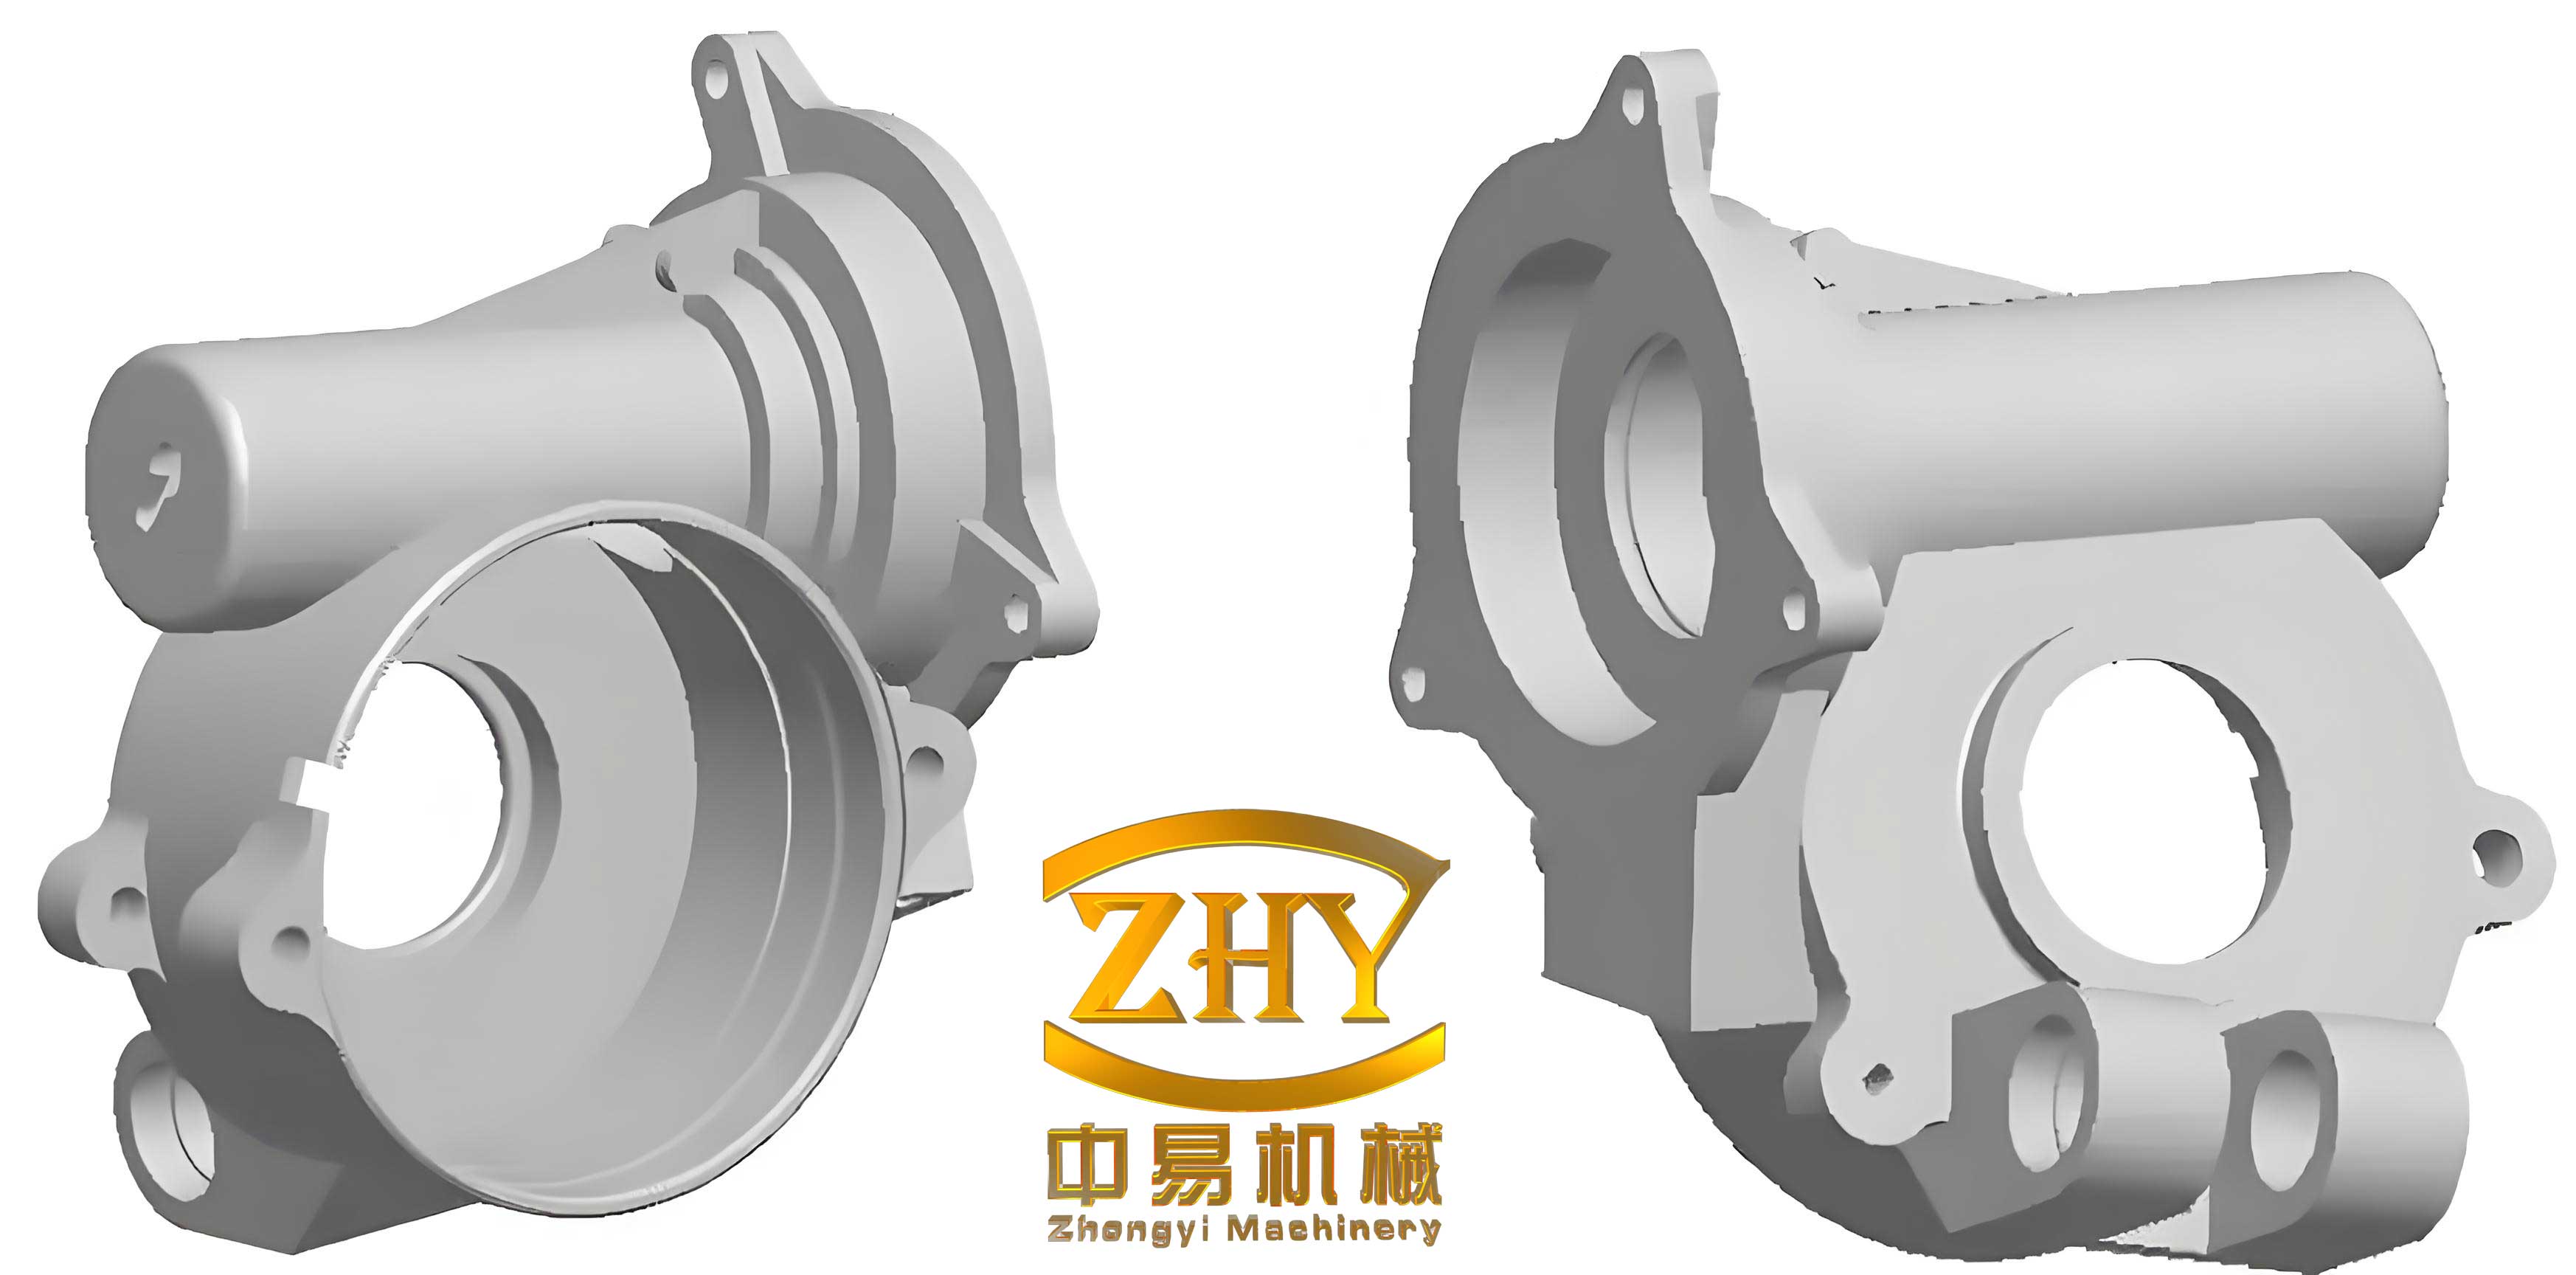
For the material, I selected ZL105A aluminum alloy due to its excellent castability, including good fluidity and low shrinkage. This alloy is well-suited for sand casting of shell castings, as it minimizes hot tearing and porosity. The chemical composition is critical for simulation accuracy, so I defined it as shown in Table 1. This data was input into AnyCasting to model the material’s thermal and physical properties during casting.
| Element | Content (%) |
|---|---|
| Si | 4.5 – 5.5 |
| Cu | 1.0 – 1.5 |
| Mg | 0.40 – 0.55 |
| Al | Balance |
Next, I designed the gating system to ensure smooth metal flow and minimize turbulence. The gating system includes a sprue, runner, and ingates, with a conical sprue design at 12° to promote gradual entry into the mold. A reservoir platform was added at the sprue base to reduce冲击 and ensure stable transition to the runner. This design is essential for shell castings, as abrupt flow can lead to defects like oxide inclusions. Two casting schemes were devised to compare different orientations of the shell casting in the mold. Scheme A positions the large planar surface at the bottom, while Scheme B places it on the side. Both schemes use a bottom-up filling approach to promote directional solidification and reduce oxidation. The pouring temperature was set at 720°C based on industrial practices, and resin sand was chosen for the mold material to achieve high precision.
To simulate the casting process, I imported the STL file from UG into AnyCasting and performed mesh generation. The mesh quality is crucial for accurate results, so I refined it in areas with thin walls, such as the beams of the shell castings. The simulation parameters included material properties, boundary conditions, and thermal parameters. For defect prediction, I used the residual melt modulus, which helps identify regions prone to shrinkage. The governing equations for fluid flow and heat transfer in AnyCasting are based on Navier-Stokes and energy conservation principles. For instance, the heat conduction equation is expressed as:
$$ \frac{\partial T}{\partial t} = \alpha \nabla^2 T $$
where \( T \) is temperature, \( t \) is time, and \( \alpha \) is thermal diffusivity. Additionally, the solidification time for shell castings can be estimated using Chvorinov’s rule:
$$ t_s = C \left( \frac{V}{A} \right)^n $$
where \( t_s \) is solidification time, \( V \) is volume, \( A \) is surface area, \( C \) is a constant dependent on mold material, and \( n \) is an exponent typically around 2. These formulas guide the simulation of thermal gradients and defect formation in shell castings.
The simulation results revealed distinct filling and solidification patterns for the two schemes. Scheme A had a total filling time of 4.5141 s, while Scheme B was faster at 3.5691 s, indicating better fluidity in Scheme B for these shell castings. However, filling time alone does not guarantee quality; defect analysis is paramount. Using AnyCasting’s defect prediction module, I identified potential shrinkage areas. Scheme A showed two defect zones: one in the internal cavity (Defect 1) and another at the beam (Defect 2). Scheme B exhibited four defects: two on the backside (Defects 3 and 4) and similar issues in the cavity and beam (Defects 5 and 6). The solidification sequence, illustrated through temperature gradients, indicated that Defect 2 in Scheme A solidified faster than surrounding areas, likely due to its thinner wall, whereas defects in Scheme B solidified slower, possibly due to proximity to the gating system.
| Scheme | Filling Time (s) | Number of Defects | Defect Locations | Solidification Characteristics |
|---|---|---|---|---|
| A | 4.5141 | 2 | Internal cavity, Beam | Fast solidification at beam |
| B | 3.5691 | 4 | Backside, Internal cavity, Beam | Slow solidification at all defect sites |
To optimize the process, I implemented modifications based on the simulation insights. For Scheme A, I added a chill made of HT200 at Defect 1 to accelerate cooling and promote directional solidification. For Defect 2, I initially increased the riser size from 10 mm to 20 mm in diameter, but this proved ineffective. Thus, I changed the riser shape from cylindrical to rectangular, reducing its height to 70% of the original to maintain manufacturability while enhancing feeding. The rectangular riser volume \( V_r \) can be calculated as:
$$ V_r = l \times w \times h $$
where \( l \), \( w \), and \( h \) are length, width, and height, respectively. For Scheme B, I placed chills at all defect locations, but this led to new defects elsewhere, indicating that excessive chilling can disrupt thermal balance. The optimized Scheme A, denoted as Improved Scheme A, included the rectangular riser and an additional chill at a newly formed defect site (Defect 7). The effectiveness of these measures was evaluated through further simulations.
| Scheme | Optimization Action | Details | Expected Outcome |
|---|---|---|---|
| A | Add chill at Defect 1 | HT200 iron chill | Accelerate cooling, eliminate shrinkage |
| A | Modify riser at Defect 2 | Change to rectangular riser, height reduced to 70% | Improve feeding, shift defect to riser |
| A | Add chill at new Defect 7 | HT200 iron chill | Prevent new defect formation |
| B | Add chills at all defects | Multiple HT200 chills | Reduce defect size, but risk new defects |
The results of Improved Scheme A showed significant improvement. The rectangular riser successfully eliminated Defect 2 by shifting the shrinkage to the riser center, thereby preserving the integrity of the shell casting. The chills at Defects 1 and 7 also removed those issues, resulting in a defect-free simulation. In contrast, Improved Scheme B reduced the size of Defects 3 and 4 and eliminated Defects 5 and 6, but introduced scattered new defects, making it less effective. This highlights the importance of targeted optimization for shell castings, where global changes can have unintended consequences. The final simulation outcomes are summarized in Table 4, which compares all schemes based on filling time and defect count.
| Scheme | Filling Time (s) | Number of Defects | Overall Evaluation | Key Insights |
|---|---|---|---|---|
| Original A | 4.5141 | 2 | Fair | Defects in critical areas |
| Original B | 3.5691 | 4 | Poor | More defects despite faster filling |
| Improved A | 4.5307 | 2 | Fair | Partial improvement, new defect formed |
| Improved B | 3.5953 | 6 | Poor | Increased defects due to chills |
| Final Improved A | 5.1686 | 0 | Excellent | Defect-free after riser and chill adjustments |
From a broader perspective, this study underscores the value of simulation in optimizing shell castings. The use of AnyCasting enabled a deep dive into the thermal and fluid dynamics of the casting process. For instance, the defect probability \( P_d \) can be modeled as a function of temperature gradient \( \nabla T \) and solidification time \( t_s \):
$$ P_d = k \cdot \exp\left(-\frac{\Delta T}{t_s}\right) $$
where \( k \) is a material constant. By manipulating risers and chills, I altered these parameters to minimize \( P_d \). The rectangular riser, in particular, improved the feeding efficiency by increasing the modulus \( M = V/A \), which is critical for shell castings with varying thicknesses. The modulus for the rectangular riser is given by:
$$ M_r = \frac{l \cdot w \cdot h}{2(lw + lh + wh)} $$
Comparing this to the cylindrical riser modulus \( M_c = r/2 \) for a cylinder of radius \( r \) and height \( h \), the rectangular design offered better control over solidification in thin-walled regions. Additionally, the chills enhanced cooling rates, as described by Fourier’s law:
$$ q = -k \frac{dT}{dx} $$
where \( q \) is heat flux, \( k \) is thermal conductivity, and \( dT/dx \) is temperature gradient. This accelerated solidification in targeted areas, reducing shrinkage in the shell castings.
In conclusion, my investigation demonstrates that numerical simulation is a powerful tool for enhancing the quality of aluminum alloy shell castings. Through iterative design and optimization, I achieved a defect-free process by combining riser modifications and strategic chill placement. The key takeaway is that each shell casting requires a tailored approach, as geometric complexities influence defect formation. Future work could explore other alloys or advanced cooling techniques to further improve shell castings. By leveraging tools like AnyCasting, foundries can reduce trial-and-error, save costs, and produce high-integrity components for demanding applications.