
In the high-voltage switchgear industry, low-pressure casting is widely employed to produce aluminum alloy shell castings with complex geometries and high-quality requirements, such as those used in Gas Insulated Switchgear (GIS). These shell castings often exhibit defects like shrinkage porosity, shrinkage cavities, and cracks due to non-uniform wall thickness and intricate structures. Traditionally, process optimization relied heavily on trial-and-error and empirical knowledge, leading to extended development cycles and increased costs. With advancements in computer simulation technology, casting simulation software like ProCAST has become instrumental in enhancing design quality, reducing production expenses, and shortening development timelines. In this study, I focus on analyzing and optimizing the solidification process of a GIS housing casting using ProCAST software. The aim is to identify the root causes of defects in the initial process and propose an optimized layout that ensures sound shell castings.
The GIS housing casting under investigation is made of ZL101A-T6 aluminum alloy, with a mass of 40 kg and a nominal wall thickness of 12 mm. The casting features a cylindrical body with flanges at both ends: one small flange and one large flange composed of eight triangular structures. The inner surface of the cylinder requires a machined roughness of 12.5 μm. The initial low-pressure sand casting process involved three ingates: one located at the small flange and two at the large flange. Chill plates with a thickness of 20 mm were placed at both ends of the casting, and a conformal chill with a thickness of 25 mm was positioned around the large flange plane. The production process included melting aluminum in a natural gas furnace, refining and modifying the melt, transferring it to a low-pressure casting holding furnace, and then pouring into prepared molds. After casting, the rough shell castings underwent cleaning, shot blasting, heat treatment, machining, and inspection. However, post-machining revealed pinhole-sized gas-slag pores or shrinkage defects on the cylinder wall, particularly near the large flange, compromising the integrity of the shell castings.
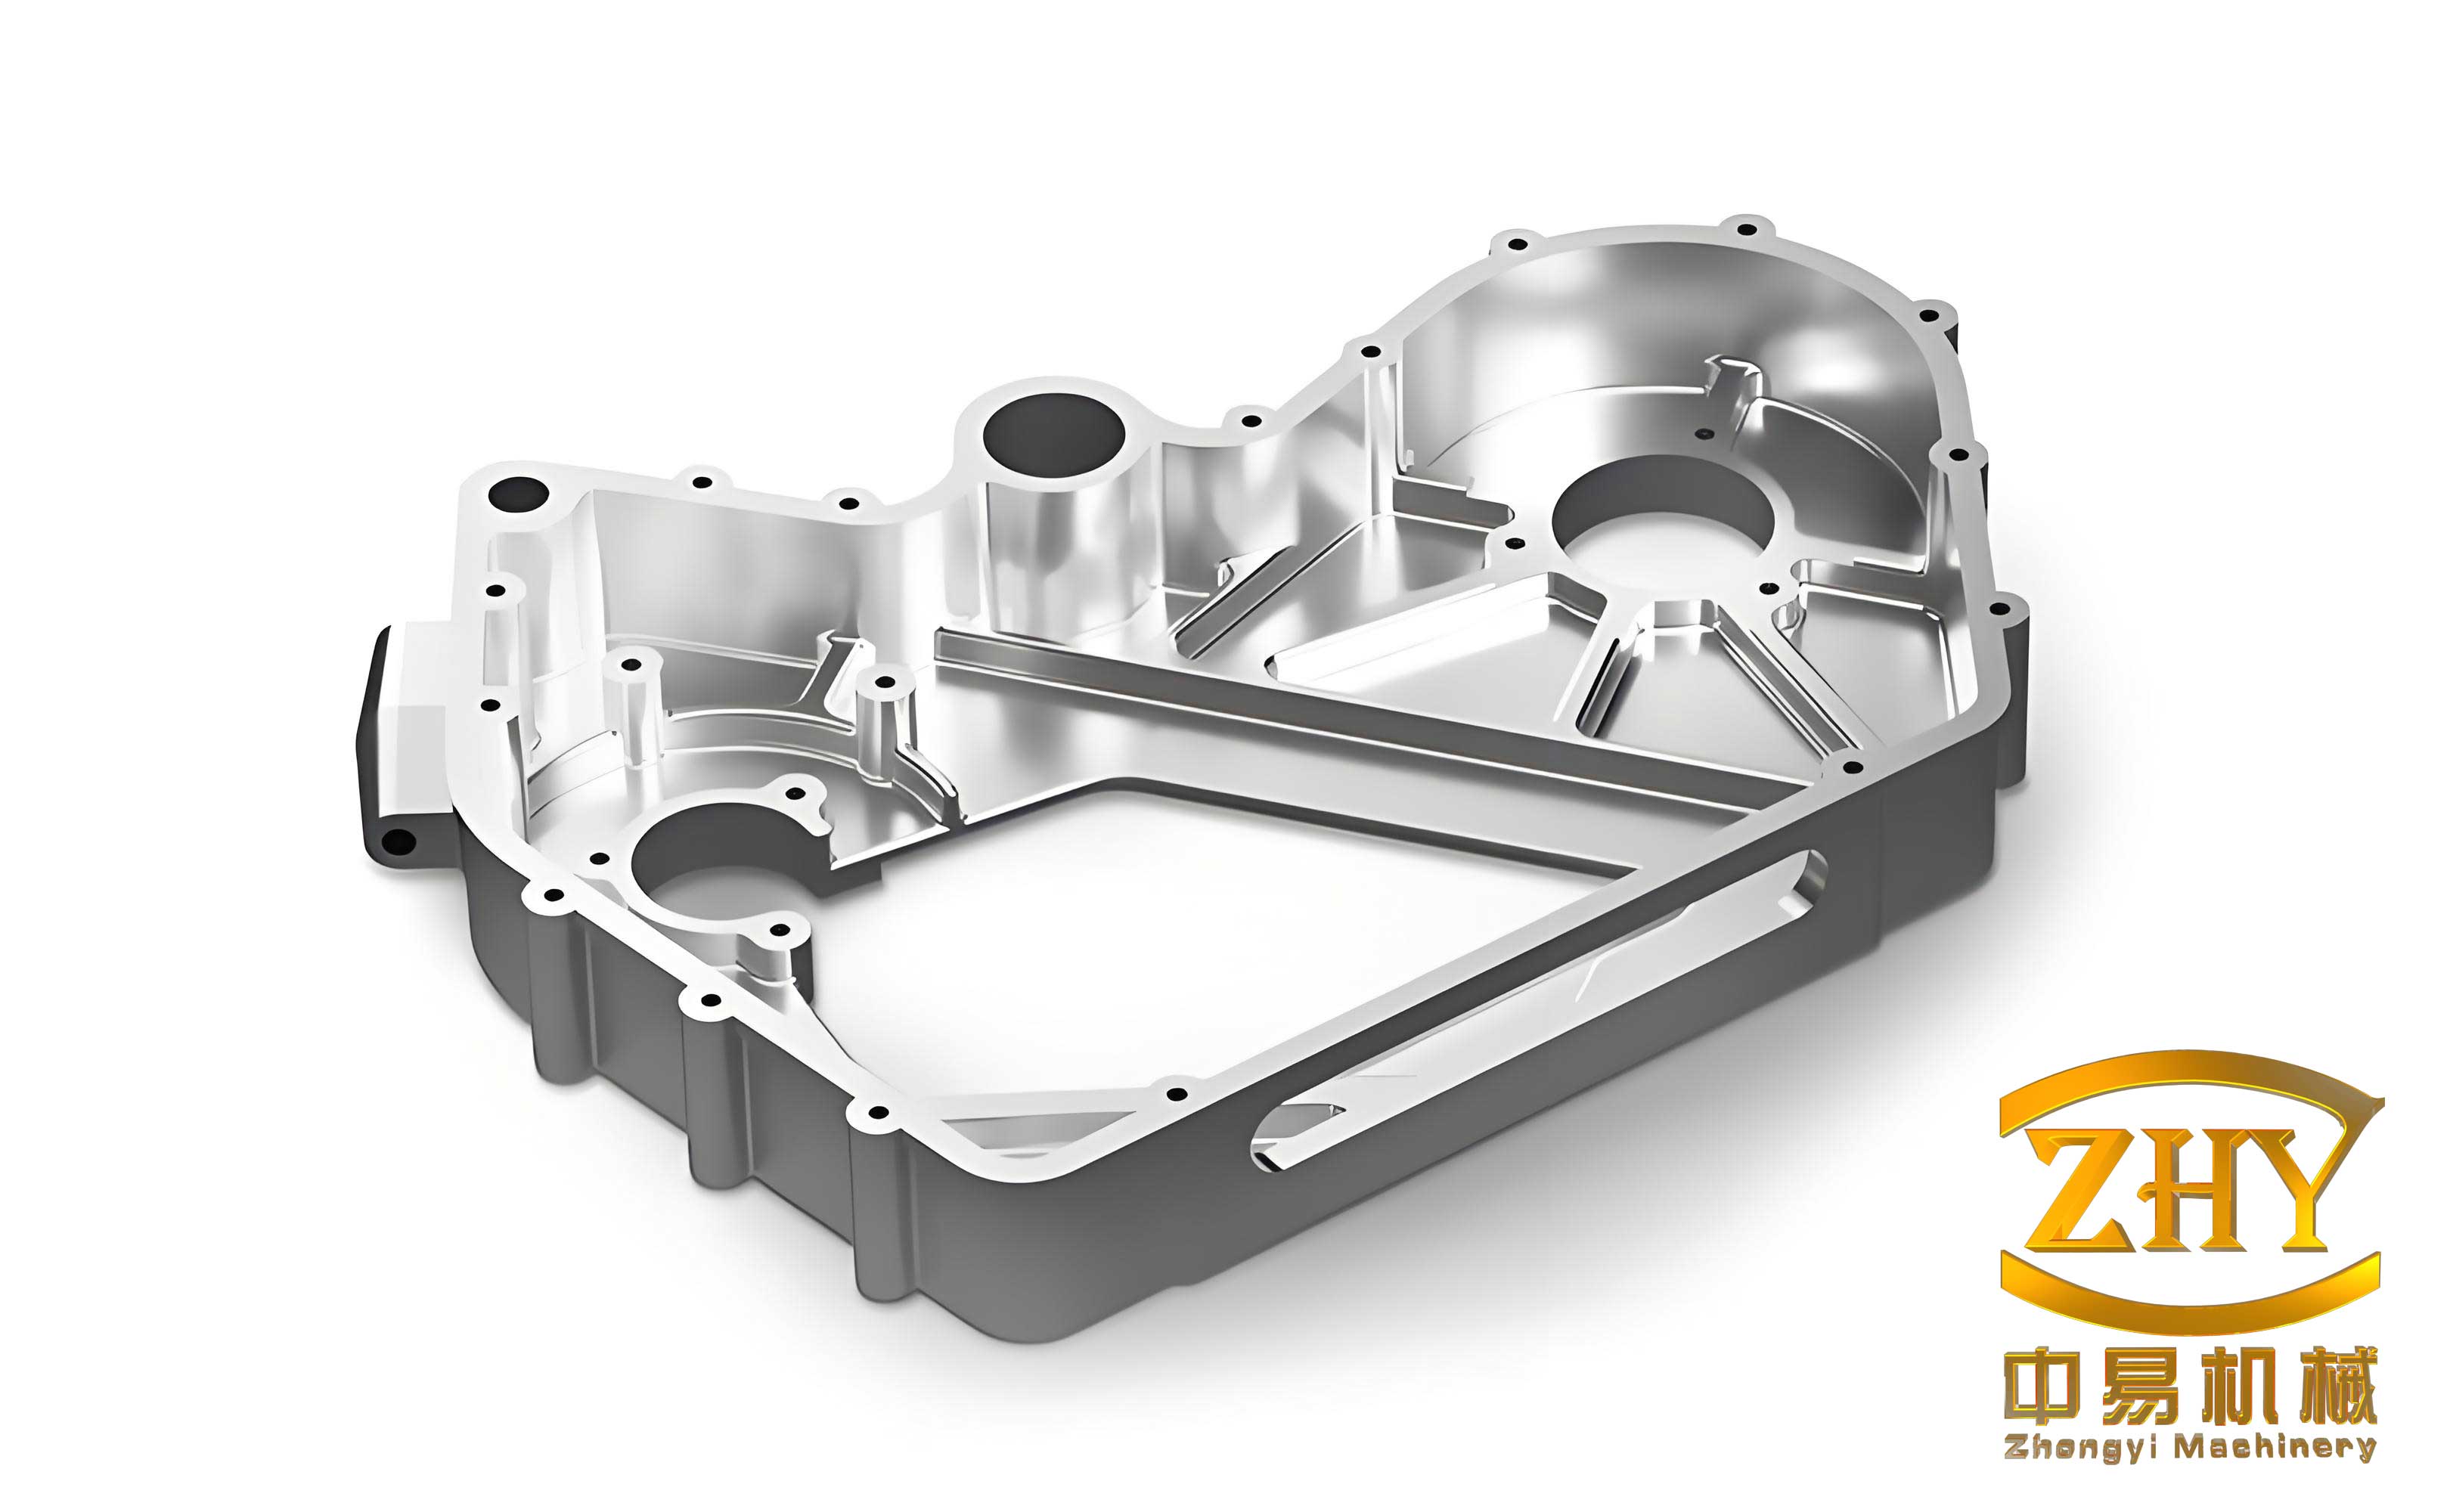
To understand the defect formation, I conducted a solidification simulation using ProCAST software. The geometry of the shell casting and the initial process layout were modeled, meshed, and simulated with key parameters summarized in Table 1. The heat transfer coefficients were set based on typical values for sand molds and chill plates. The simulation encompassed filling and solidification stages, with defect prediction utilizing the Niyama criterion, which relates shrinkage porosity to thermal parameters during solidification. The Niyama criterion is expressed as:
$$ N = \frac{G}{\sqrt{R}} $$
where \( G \) is the temperature gradient (K/m) and \( R \) is the cooling rate (K/s). Regions with \( N \) values below a critical threshold indicate a high risk of shrinkage defects. This criterion is integral to evaluating the quality of shell castings.
| Parameter | Value | Unit |
|---|---|---|
| Casting Material | ZL101A-T6 | – |
| Pouring Temperature | 700 | °C |
| Mold Material | SiO₂ Sand | – |
| Mold Temperature | 50 | °C |
| Cooling Method | Air Cooling | – |
| Heat Transfer Coefficient (Casting-Sand Core) | 500 | W/(m²·K) |
| Heat Transfer Coefficient (Chill-Mold) | 500 | W/(m²·K) |
| Heat Transfer Coefficient (Casting-Chill) | 1000 | W/(m²·K) |
The chemical composition of the ZL101A alloy, crucial for the material properties in simulation, is provided in Table 2. This alloy is commonly used for such shell castings due to its good castability and mechanical properties.
| Element | Min | Max | Typical |
|---|---|---|---|
| Ti | 0.08 | 0.20 | 0.14 |
| Mg | 0.25 | 0.45 | 0.35 |
| Si | 6.50 | 7.50 | 7.00 |
| Fe | – | 0.20 | 0.10 |
| Mn | – | 0.10 | 0.05 |
| Zn | – | 0.10 | 0.05 |
| Cu | – | 0.20 | 0.10 |
| Other Impurities | – | 0.15 | – |
| Al | Balance | ||
The simulation of the initial process revealed that the filling stage was relatively smooth, with no significant gas entrapment, as indicated by a continuous color gradient representing filling time. This suggested that the defects were not primarily due to gas-related issues. However, the solidification analysis showed shrinkage porosity and cavities around the cylinder wall, especially near the ingates at the large flange. The Niyama criterion plot highlighted these risk zones, aligning with the actual defects observed in the shell castings. The solidification time distribution further indicated that regions around the ingates solidified earlier than the adjacent cylinder wall, creating isolated liquid zones. This premature solidification blocked the feeding channels, preventing molten metal from compensating for volumetric shrinkage during the later stages of solidification. The formation of isolated liquid zones can be described by the thermal dynamics equation:
$$ \frac{\partial T}{\partial t} = \alpha \nabla^2 T + S $$
where \( T \) is temperature, \( t \) is time, \( \alpha \) is thermal diffusivity, and \( S \) represents heat sources or sinks. In this case, the intense cooling from the 25 mm thick conformal chill at the large flange acted as a heat sink, accelerating solidification near the ingates and disrupting sequential solidification. The critical solidification time \( t_c \) for defect formation can be estimated from the thermal modulus, which for shell castings is often related to the wall thickness \( d \) and cooling conditions:
$$ t_c \propto \frac{d^2}{\alpha} $$
For the cylinder wall with \( d = 12 \) mm, the computed solidification times exceeded 350 s in isolated patches, correlating with defect locations. This non-uniform solidification pattern was a direct consequence of the chill design, leading to shrinkage defects in the shell castings.
To address these issues, I optimized the process layout by modifying the chill configuration at the large flange. The optimized design involved replacing the 25 mm thick conformal chill with a 15 mm thick chill that was offset from the ingate locations. Specifically, the chill was positioned to avoid the ingates, and its inner circumference was maintained at a distance of 10 mm from the cylinder wall. This adjustment aimed to reduce the excessive cooling near the ingates while still promoting directional solidification. Other aspects of the process, such as the chill plates at the ends, remained unchanged. The goal was to ensure that the solidification of the shell castings proceeded sequentially from the remote sections toward the ingates, allowing adequate feeding throughout the process.
Simulating the optimized process confirmed significant improvements. The filling stage remained stable, and the solidification analysis showed no shrinkage defects. The Niyama criterion values were above the critical threshold across the casting, indicating a sound structure. The solidification time distribution demonstrated a sequential pattern, with the cylinder wall and ingate regions solidifying in a continuous manner. This can be quantified by the temperature gradient \( G \) and cooling rate \( R \) along the casting. For sequential solidification, the ratio \( G/R \) should be sufficiently high to avoid isolated liquid zones. In the optimized case, the computed values met this requirement, as summarized in Table 3 for key regions of the shell castings.
| Process | Region | Temperature Gradient \( G \) (K/m) | Cooling Rate \( R \) (K/s) | Niyama Criterion \( N \) (K·s1/2/m) | Defect Risk |
|---|---|---|---|---|---|
| Initial | Cylinder Wall near Ingates | 50 | 0.5 | 70.7 | High |
| Isolated Liquid Zone | 30 | 0.3 | 54.8 | High | |
| Optimized | Cylinder Wall | 80 | 0.4 | 126.5 | Low |
| Ingate Region | 70 | 0.6 | 90.5 | Low |
The improvement can also be analyzed using the Chvorinov’s rule for solidification time \( t_s \):
$$ t_s = C \left( \frac{V}{A} \right)^n $$
where \( V \) is volume, \( A \) is surface area, \( C \) is a constant dependent on mold material and casting conditions, and \( n \) is an exponent typically around 2. For the shell castings, the modified chill reduced the effective cooling area near the ingates, adjusting the \( V/A \) ratio to favor sequential solidification. The thermal history \( T(t) \) at critical points can be modeled with an exponential decay function:
$$ T(t) = T_0 e^{-kt} $$
where \( T_0 \) is initial temperature and \( k \) is a cooling constant. In the optimized layout, the cooling constant near the ingates was lowered, preventing premature solidification.
To validate the simulation results, the optimized process was implemented in actual production. Over ten shell castings were produced using the modified chill design. Post-machining inspection revealed that the inner surface defects were eliminated, with a qualification rate exceeding 95%. This confirms the accuracy of the ProCAST simulation and the effectiveness of the optimization for producing high-quality shell castings. The success of this approach underscores the value of computer simulation in refining casting processes for complex components like GIS housing castings.
In conclusion, the defects in the low-pressure cast GIS housing were identified as shrinkage porosity and cavities caused by isolated liquid zones due to premature solidification near the ingates. The initial process used a 25 mm thick conformal chill at the large flange, which led to excessive cooling and blocked feeding channels. Through simulation-based optimization, the chill was redesigned to a 15 mm thickness, offset from the ingates and spaced 10 mm from the cylinder wall. This promoted sequential solidification, eliminated shrinkage defects, and ensured sound shell castings. The production validation aligned perfectly with the simulation predictions, demonstrating the robustness of this methodology. Future work could explore further optimizations, such as varying chill materials or integrating advanced feeding systems, to enhance the performance and reliability of shell castings in critical applications.
Additionally, the principles applied here can be extended to other types of shell castings with similar geometric challenges. The use of ProCAST software enables a detailed analysis of thermal parameters, allowing for precise control over the solidification process. For instance, the heat flux \( q \) across the chill-casting interface can be calculated using Fourier’s law:
$$ q = -k \frac{\partial T}{\partial x} $$
where \( k \) is thermal conductivity and \( \frac{\partial T}{\partial x} \) is the temperature gradient. By optimizing this heat flux through chill design, defects in shell castings can be minimized. Moreover, statistical methods like design of experiments (DOE) could be coupled with simulation to systematically explore process variables, further improving the quality of shell castings.
In summary, this study highlights the critical role of solidification simulation in optimizing casting processes for GIS housing components. The iterative approach of simulating, analyzing, and refining led to a reliable process that produces defect-free shell castings, ultimately reducing costs and development time. As casting technologies evolve, such simulation-driven methodologies will become increasingly vital for manufacturing high-integrity shell castings in the energy and transportation sectors.