
In my assessment of modern wind power manufacturing, the combination of carbon-reduction policy pressure and grid-parity electricity pricing has made competition in the wind sector much more intense. Product technology now iterates at high speed, and offshore medium- and large-capacity turbines, especially those rated at 7 MW and above, have become a mainstream direction. In this setting, semi-direct-drive and doubly fed generator architectures demand increasingly robust structural components. Typical ductile iron casting components in a wind turbine include the hub, the nacelle elbow, and the cast iron main shaft. A single ductile iron casting can weigh from 10 t to 50 t, and both the dimensions and the weight of these iron components continue to increase. When I examine heavy-section ductile iron casting production, I see that multiple defects can appear during manufacturing and processing, and these defects strongly affect the final comprehensive performance. Therefore, the quality of raw materials and the control of melting, nodularization, inoculation, molding, cooling, and heat treatment are extremely important for successful ductile iron casting.
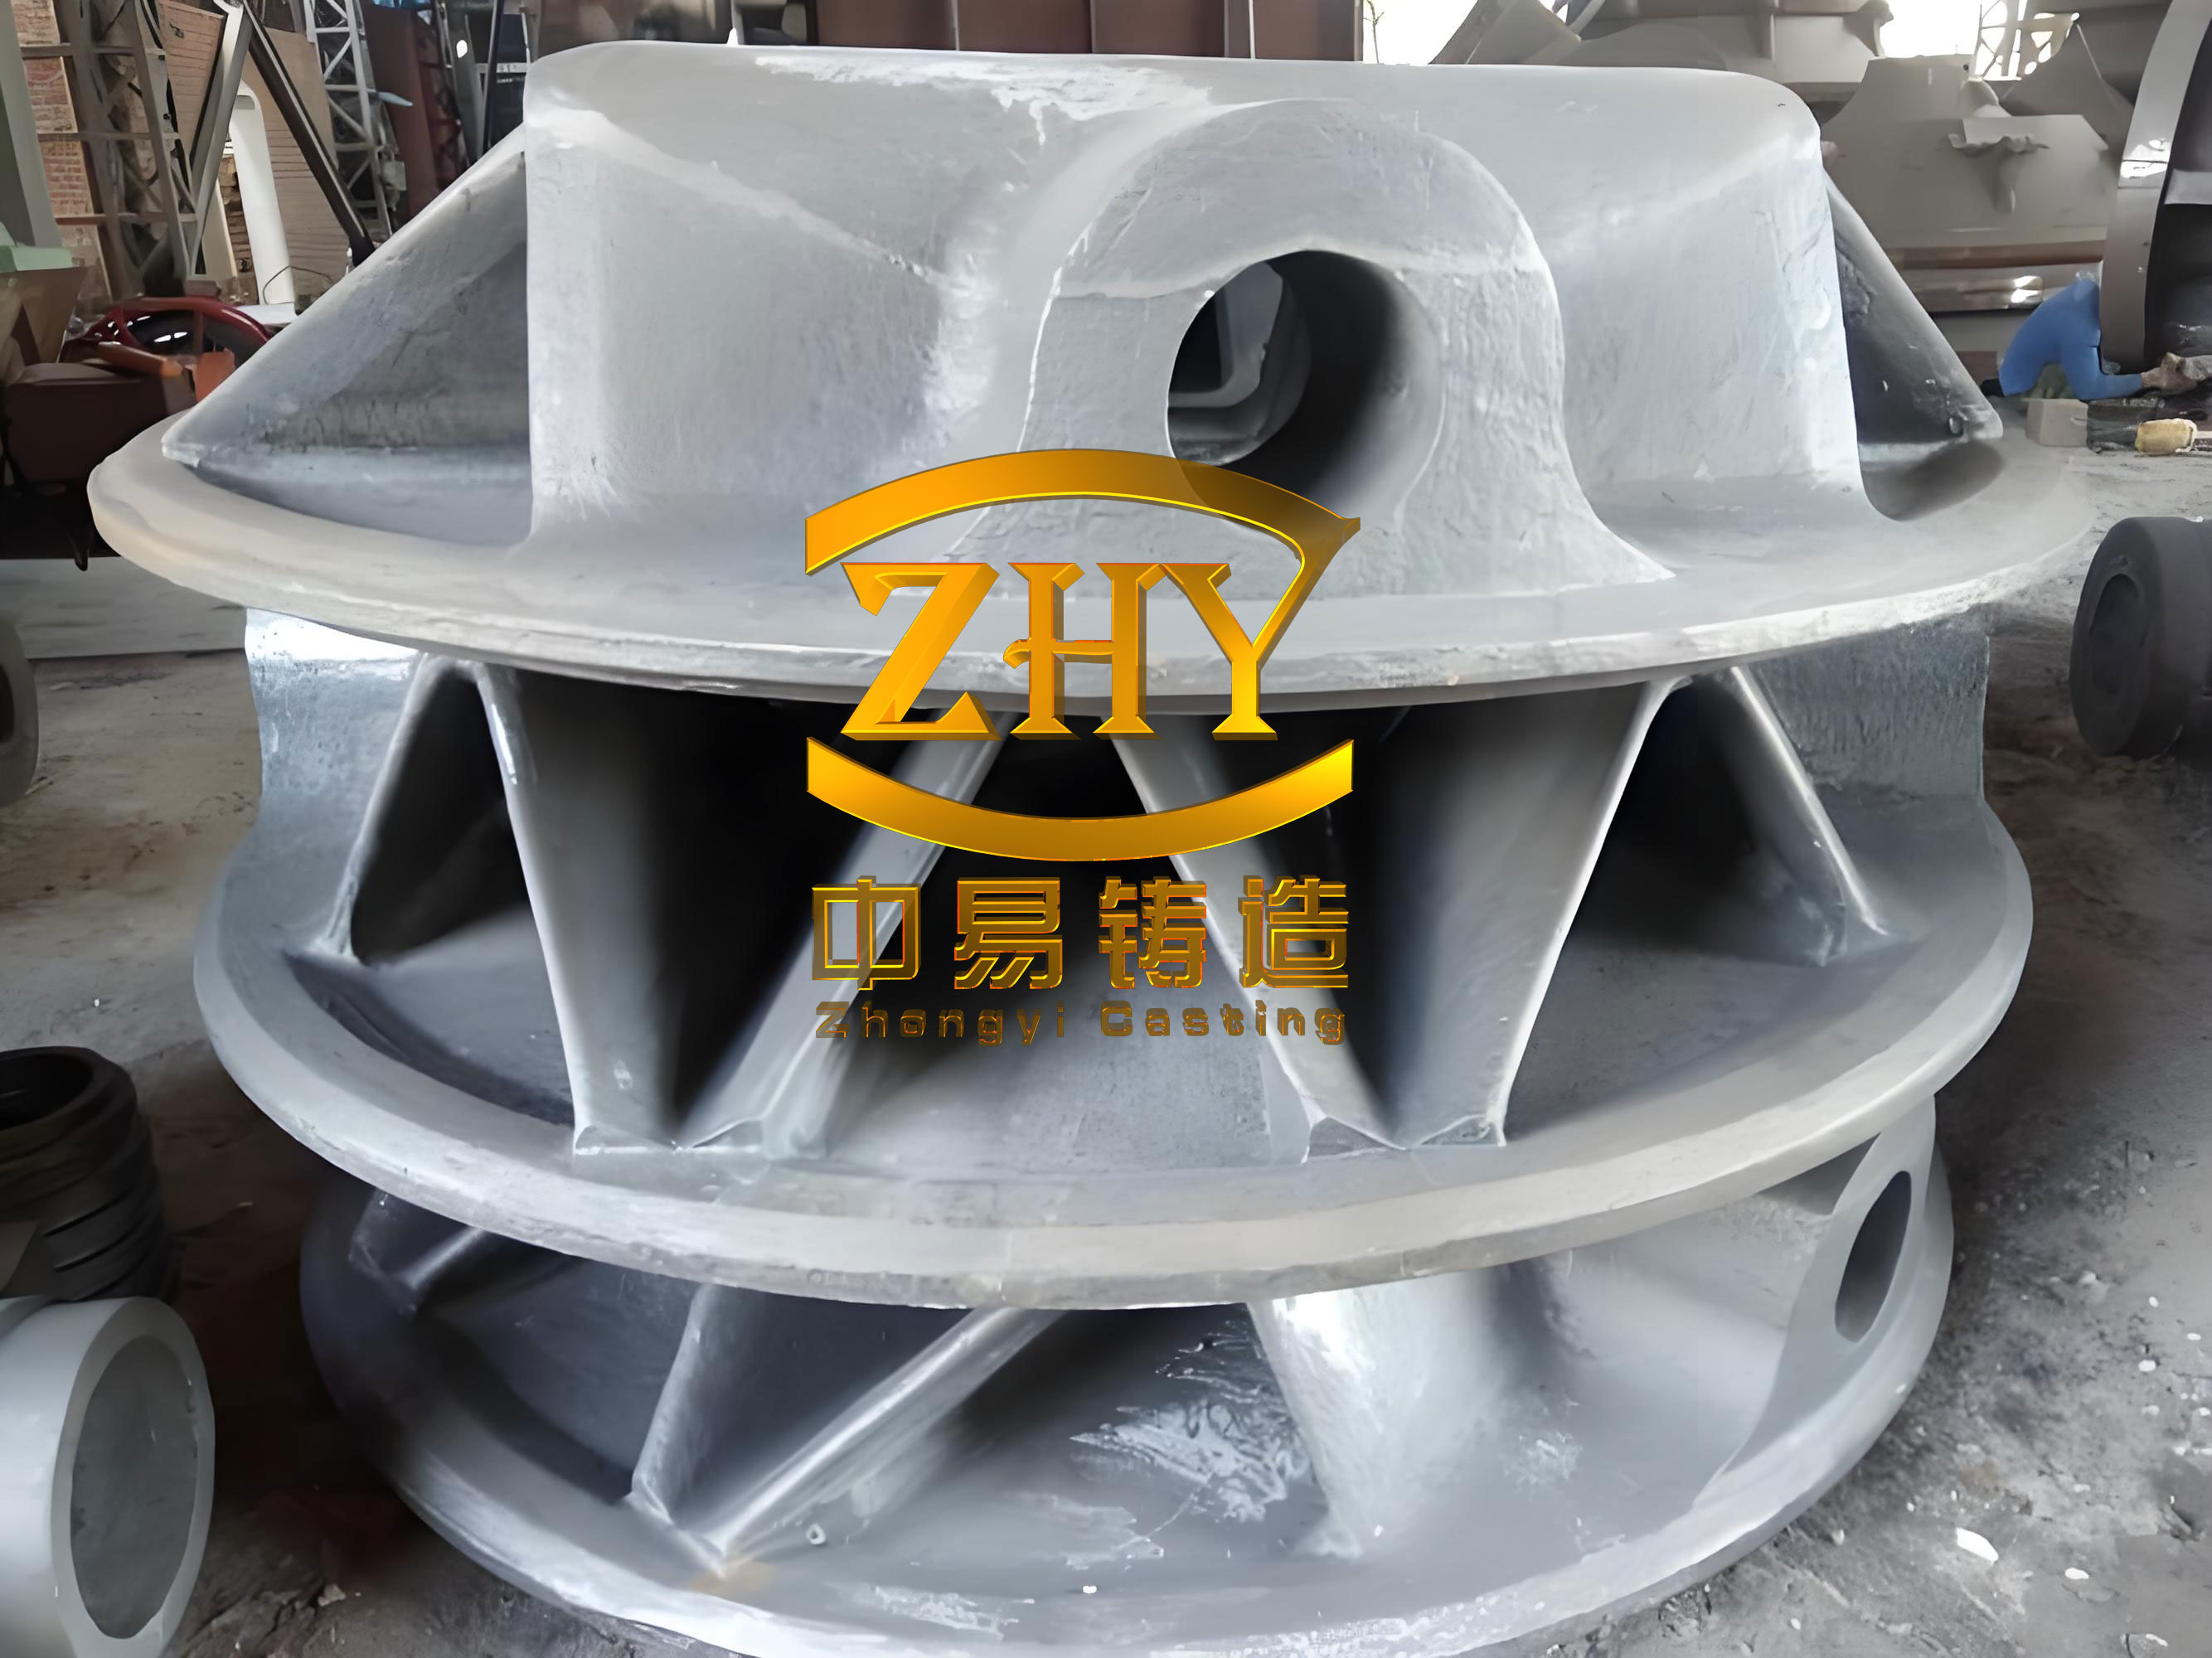
From my first-person perspective, the service environment of an offshore wind turbine is unusually severe. Large-capacity offshore units form wind turbine clusters in coastal waters, and the nacelle body is often more than one hundred meters above the sea surface. The working environment is demanding: unit weight increases substantially, and the load conditions of key structural parts become complex; extreme operating temperatures can fall to between -20 °C and -60 °C; offshore wind speed is high and changes rapidly, so the unit experiences complex alternating loads; hurricanes, thunderstorms, and salt-laden moisture are common, so corrosion protection, lightning protection, waterproofing, and fire protection requirements are stricter; and component installation, transportation, lifting, and maintenance are difficult. As a result, system reliability must be improved. Offshore wind turbines therefore place extremely strict requirements on the mechanical properties, low-temperature toughness, fatigue life, safety protection, and reliability of key structural ductile iron casting parts such as hubs, elbows, and main shafts. At the same time, heavy-section ductile iron is difficult to produce and its process is complex, which creates a high bottleneck in research, design, and manufacturing technology. For this reason, the application of ductile iron casting material in low-temperature offshore units has been constrained.
I have observed that heavy-section ductile iron casting commonly suffers from several defect families. The factors that push these defects above or below acceptable limits can be summarized systematically. In my own process reasoning, I treat carbon equivalent, residual rare earth content, silicon content, inoculant amount and fading, spheroidizing agent condition, trace element contamination, pouring temperature, cooling rate, mold rigidity, and melt cleanliness as the dominant variables. The following table summarizes the defect patterns I consider most relevant to low-temperature high-toughness ductile iron casting.
| Defect pattern | Excess or over-high factor | Deficiency or under-low factor |
|---|---|---|
| Graphite flotation | Carbon equivalent, carbon content, pouring temperature | Inoculant content and inoculation effectiveness, cooling rate |
| Chunky graphite | Residual rare earth, silicon content, inoculant content, cooling rate | Inoculation effectiveness, antinodularizing elements such as Sn and Te |
| Nodularization fading | Melt purity | Residual Mg and rare earth, treatment-to-pouring time |
| Exploded graphite | Carbon equivalent, carbon content, residual rare earth | Nodularization treatment temperature, pouring time, inoculant content, inoculation effectiveness |
| Vermicular graphite | Antinodularizing elements such as Sn and Te, sulfur and oxygen impurities | Residual Mg and rare earth, nodularization effectiveness |
| Flake graphite | Pb, Ti, Bi, Sb, and Te content, residual Mg, O, and rare earth | Melt purity, nodularization effectiveness |
| Segregation and inclusions | V, Ti, Cr, Mn and other trace elements | Cooling rate, melt cleanliness |
| Inverse chill | Chemical segregation, V, Ti, Cr content | Inoculation effect, cooling rate, pouring temperature |
| Shrinkage porosity | Sand mold yield, carbon equivalent | Nodularization and inoculation effect, cooling rate |
| Slag inclusion | S, Si, O impurity content, residual Mg and rare earth | Pouring temperature, gating system slag removal |
| Nodularization and inoculation fading | S and O impurity content | Tap temperature, pouring temperature, pouring time, holding time after treatment |
When I design a low-temperature high-toughness ductile iron casting, I first calculate the carbon equivalent because it affects graphite morphology, shrinkage behavior, and low-temperature impact toughness. For ductile iron, the commonly used carbon equivalent expression is:
$$CE = C + \frac{Si + P}{3}$$
A more complete expression that I sometimes use for practical estimation is:
$$CE = C + \frac{Si}{3} + \frac{P}{3} + \frac{Mn}{6} + \frac{Cu}{12} + \frac{Ni}{15} + \frac{Cr}{9}$$
In my experience, the carbon equivalent must be controlled within a narrow window. If it is too high, graphite flotation and exploded graphite become more likely in a heavy-section ductile iron casting. If it is too low, shrinkage porosity and inverse chill become more likely. I also use the thermal modulus concept to assess solidification time and feeding behavior:
$$M = \frac{V}{A}$$
$$t_s = k M^n$$
Here, \(M\) is the thermal modulus, \(V\) is the volume of the ductile iron casting section, \(A\) is the heat-transfer surface area, \(t_s\) is the local solidification time, and \(k\) and \(n\) are empirical constants. For a heavy-section ductile iron casting, a large local thermal modulus means slow cooling, coarse graphite, possible chunky graphite, and a greater risk of nodularization fading. I therefore combine thermal modulus calculations with simulation and with chill design rather than relying on a single rule of thumb.
In my raw material strategy, I begin with the principle that the chemical composition of low-temperature high-toughness ductile iron casting must be stable. Trace elements and impurities have a hereditary influence, so I control the purity of every charge component. The main charge usually consists of pig iron, steel scrap, returns, ferrosilicon, and graphite carburizer, with inoculants and nodularizers added later. A typical charge window that I consider is shown below.
| Charge component | Typical proportion | Primary function and control point |
|---|---|---|
| Pig iron | 50%–90% | Provides stable carbon and silicon; high-purity nodular iron grade is preferred; total trace elements should not exceed about 0.1% |
| Steel scrap | 5%–30% | Adjusts carbon and silicon; low-silicon and high-purity carbon steel scrap is preferred; V, Cr, Ti, and other carbide-forming or antinodularizing elements must be strictly limited |
| Returns | 10%–30% | Improves economic efficiency; must be clean, non-welded, and free of rust, oil, sand, and coatings |
| Ferrosilicon | 0.4%–0.6% | Deoxidation and silicon adjustment; FeSi75, SiC, or SiCa can be used, but excessive addition raises silicon and harms low-temperature toughness |
| Graphite carburizer | Balance | Adjusts carbon content; must be low in sulfur and ash |
| Nodularizer | 1.4%–1.6% of melt mass | Provides Mg and rare earth for spheroidization; grade and particle size depend on treatment temperature and section size |
| Inoculant | 0.7%–1.5% of melt mass | Controls graphite nucleation, refines grains, stabilizes ferrite, and reduces chill; short-time and multiple inoculation are preferred |
For pig iron, I prefer high-purity grades dedicated to ductile iron production because the charge proportion is high and the influence is large. For scrap and returns, I avoid materials that contain antinodularizing or carbide-stabilizing elements. I also require surface cleaning by chemical pickling, physical shot blasting, or grinding, followed by removal of oil, grease, and weld seams. These steps may appear simple, but in my experience they are essential for a reliable low-temperature ductile iron casting.
For ferrosilicon and silicon-bearing additives, I use FeSi75, SiC, and SiCa for deoxidation and to reduce excessive carbon loss caused by boiling. However, I never allow the silicon content to drift upward without control. Excess silicon promotes chunky graphite and reduces low-temperature impact toughness. In a low-temperature high-toughness ductile iron casting, silicon is a powerful graphitizing element, but it also changes the ductile-to-brittle transition behavior. I therefore treat silicon as a tightly bounded alloying element rather than as a simple deoxidizer.
Nodularization is one of the most important stages in my process route. Because wind turbine heavy-section ductile iron casting components are large and heavy, the pouring and solidification time is long, and nodularization fading is a serious risk. I therefore prefer rare-earth silicon-magnesium alloys. A high-temperature tap may use FeSiMg6RE2, while a lower-temperature tap may use FeSiMg8RE3. The total nodularizer addition is usually about 1.4% to 1.6% of the melt mass. I also control the particle size, generally in the range of 10 mm to 30 mm, and I control the effective Mg and rare earth content. The treatment method may be the sandwich method, wire feeding, secondary nodularization, or composite nodularization. In my judgment, the choice depends on melt sulfur, treatment temperature, equipment accuracy, and the required reproducibility of the ductile iron casting.
| Parameter | Typical range or choice | Reason for control |
|---|---|---|
| Nodularizer alloy | FeSiMg6RE2 for high-temperature tap; FeSiMg8RE3 for lower-temperature tap | Balances Mg reactivity, rare earth recovery, and fading resistance |
| Nodularizer addition | 1.4%–1.6% of melt mass | Ensures spheroidization while avoiding excess Mg and rare earth |
| Nodularizer particle size | 10–30 mm | Controls reaction rate and recovery in heavy-section treatment |
| Treatment temperature | 1365–1375 °C | Promotes reaction without excessive Mg vaporization |
| Reaction time | 90–170 s | Matches melt mass, composition, and temperature |
| Inoculant base | FeSi75 with Ba, Mn, or other elements as needed | Provides heterogeneous nuclei and stabilizes graphite |
| Inoculant addition | 0.7%–1.5% of melt mass | Refines graphite, increases ferrite stability, and lowers chill |
| Inoculation timing | Short-time, few additions, and near-final pouring | Reduces fading and avoids excessive slag and dross |
I also use simple mass-balance formulas to set additions. For nodularizer mass:
$$M_{nod} = \left(1.4\% \text{ to } 1.6\%\right) M_{iron}$$
For inoculant mass:
$$M_{inoc} = \left(0.7\% \text{ to } 1.5\%\right) M_{iron}$$
If I target a specific residual magnesium level, I estimate recovery with:
$$M_{Mg,residual} = \eta_{Mg} \frac{M_{nod} C_{Mg}}{M_{iron}}$$
Here, \(\eta_{Mg}\) is the magnesium recovery coefficient, \(C_{Mg}\) is the magnesium content in the nodularizer, and \(M_{iron}\) is the iron melt mass. In my practice, I do not rely only on calculation; I verify with spectrometer analysis and with microstructure evaluation of the ductile iron casting.
Melting equipment and melting method also shape the final ductile iron casting. To meet green production and energy-saving requirements, I prefer induction melting furnaces for higher efficiency and better composition control. Some operations use a cupola plus induction duplex melting route. In either case, I insist on rigorous furnace-front element testing and real-time composition adjustment. The goals are controllable melting, reduced element loss, stronger desulfurization, and uniform melt composition. For low-temperature high-toughness ductile iron casting, sulfur and oxygen control are especially important because they consume Mg and rare earth, increase inclusions, and destabilize spheroidization.
I have found that pretreatment before nodularization is highly beneficial. Early practice sometimes transferred the melt directly from melting to nodularization and inoculation, but research and production experience show that a pretreatment agent can remove oxygen and sulfur before the main nodularization reaction. A silicon-ferroalloy pretreatment can reduce cost and, to a certain extent, improve graphite count and graphitization degree, thereby enhancing the subsequent nodularization and inoculation effect. However, I always remember that pretreatment has a fading period. I therefore coordinate pretreatment reagent type, dosage, and the time before nodularization and inoculation. If I delay too long, the benefit declines and the ductile iron casting quality becomes less predictable.
For nodularization treatment, I evaluate both the sandwich method and wire feeding. The sandwich method requires simple equipment and is flexible, but at high temperature the reaction can become too violent, causing Mg loss and nodularization fading. Operators sometimes add SiCa alloy or build a reaction delay barrier, but this can increase cost and side effects. Wire feeding requires professional equipment and has a relatively higher cost, yet it gives a better nodularization effect, better quality control, and greater flexibility. The wire type, wire feed speed, and nodularizer amount can be controlled online according to the real-time sulfur content of the melt. For low-temperature high-toughness ductile iron casting, I prefer wire feeding when the production scale justifies it because it helps reduce excess nodularizer and limits the harmful effects of residual Mg and rare earth.
I also see increasing use of dynamic control systems for nodularization and inoculation. Such systems integrate research conclusions and production experience into software models. They can predict whether the base iron is metallurgically suitable, calculate the precise additions of nodularizer and inoculant according to production conditions, and provide early prediction and adjustment of the nodularization and inoculation effect. In my view, this is one of the most practical paths toward shorter production cycles, lower cost, lower resource consumption, and higher ductile iron casting quality. Reaction speed and time should be matched to treatment mass, composition, and treatment temperature. A reaction time of 90 s to 170 s and a treatment temperature of 1365 °C to 1375 °C are reasonable windows for many heavy-section ductile iron casting operations.
Inoculation is the next critical step. I use inoculation for deoxidation, desulfurization, melt purification, and heterogeneous nucleation. The purpose is to promote graphite nucleation, refine grains, increase graphitization degree, stabilize ferrite content, and reduce chill tendency. Silicon-based composite inoculants containing calcium, barium, manganese, or other elements are common. The inoculant composition, amount, time, temperature, and number of additions all affect the result. In heavy-section ductile iron casting, the total inoculant addition is often 0.7% to 1.5%. For ladle inoculation, a coarser particle size of about 3 mm to 5 mm can help reduce chunky graphite tendency, while stream inoculation requires a smaller particle size. I pay close attention to the melting state of the inoculant and its matching with the pouring process. The principle is nearest-neighbor pouring, which reduces slag and dross from inoculation. In-mold inoculation, pouring cup inoculation, and stream inoculation can effectively refine grains, prevent graphite distortion, stabilize ferrite, and improve the comprehensive properties of the ductile iron casting. For heavy-section parts, I select long-acting inoculants and use instantaneous inoculation, multiple inoculation, or combined inoculation with more than one inoculant.
| Inoculation route | Preferred condition | Main benefit | Risk to control |
|---|---|---|---|
| Ladle inoculation | General heavy-section production | Simple, flexible, and effective for initial nucleation | Fading, slag, uneven distribution |
| In-mold inoculation | Complex thin-to-thick transitions and high-quality surfaces | Refined graphite and reduced chill | Reaction product accumulation and mold erosion |
| Pouring cup inoculation | Large castings with controlled pouring rate | Late nucleation and reduced fading | Incomplete dissolution |
| Stream inoculation | Final-stage nucleation before cavity filling | Strong chilling reduction and fine graphite | Particle size and flow-rate matching |
| Multiple or combined inoculation | Low-temperature high-toughness ductile iron casting | Stable ferrite and high impact toughness | Over-inoculation and silicon increase |
For molding and casting, I use gravity casting and parted mold methods for wind power heavy-section ductile iron casting. The sand mold must have high stiffness, high compactness, low yield, good thermal conductivity, and good permeability. Because ductile iron melt has high thermal expansion during cooling, and because a single pour can involve a large mass, high speed, and high temperature, the mold experiences strong impact, compression, and thermal action. I therefore require a high-quality mold surface, hard and permeable coating materials, a high-stiffness flask, and a well-designed riser and venting system to improve feeding and exhaust. This is not only a matter of surface quality; it directly influences shrinkage porosity, graphite flotation, and dimensional accuracy in the ductile iron casting.
Pouring temperature control is another area where I apply strict discipline. To avoid excessive tap temperature weakening nodularization and inoculation, and to prevent sulfur and carbon from exceeding specification, I keep the tap temperature below 1460 °C. Nodularization and inoculation treatment are performed at 1365 °C to 1375 °C. After treatment, pouring should be completed within 20 min to prevent nodularization and inoculation fading, which can cause graphite distortion. For heavy-section ductile iron casting, I follow the principle of high-temperature tapping and low-temperature pouring. A pouring temperature below 1350 °C can effectively reduce shrinkage cavity, shrinkage porosity, and graphite flotation tendency. These limits can be summarized as:
$$T_{tap} \le 1460^\circ C$$
$$T_{treatment} = 1365^\circ C \text{ to } 1375^\circ C$$
$$T_{pour} \le 1350^\circ C$$
$$t_{pour} \le 20 \text{ min}$$
I also use simulation to design the gating and cooling system. Software such as ProCast, Magma, CAE, CAE/CAM, and ANSYS allows me to model filling and solidification, locate misruns, shrinkage porosity, and hot spots, and optimize the gating and cooling system for stable filling and faster cooling. In many large low-temperature high-toughness ductile iron casting parts, feeding is achieved by the self-expansion of graphite during solidification, which supports an advanced riserless or reduced-riser pouring process. At the same time, I place filters in the gating system and venting strips in heavy sections. These measures have a measurable effect on slag inclusion and gas porosity. I have seen that a well-balanced gating system reduces turbulence, prevents reoxidation, and improves the internal quality of the ductile iron casting.
| Control item | Recommended range or practice | Effect on ductile iron casting |
|---|---|---|
| Tap temperature | ≤ 1460 °C | Limits Mg loss, sulfur increase, and carbon fluctuation |
| Treatment temperature | 1365–1375 °C | Balances nodularization reaction and recovery |
| Pouring temperature | ≤ 1350 °C for heavy sections | Reduces shrinkage, graphite flotation, and chunky graphite |
| Pouring time after treatment | ≤ 20 min | Prevents nodularization and inoculation fading |
| Gating design | Simulation-optimized, filtered, nonturbulent | Reduces slag, gas, reoxidation, and misrun risk |
| Venting | Vents at heavy-section and hot-spot locations | Reduces gas porosity and pressure defects |
| Feeding strategy | Graphite self-expansion plus selective risers | Controls shrinkage porosity and yield |
Cooling environment improvement is essential because large-tonnage ductile iron casting cools slowly. Slow cooling promotes graphite flotation, morphological distortion, and coarse grains. I target a cooling time within 2 h for large castings where feasible. Chill thickness is often set to 50% to 100% of the local wall thickness. The two main cooling methods I use are chill cooling and forced cooling. For chill cooling, low-cost cast iron chills with good thermal conductivity and heat storage are common. Graphite chills have lower heat storage but high thermal conductivity, so they can be used for thinner walls or where directional cooling is required. For larger sections and higher cooling requirements, forced cooling by air, water, spray, or liquid nitrogen may be necessary. I calculate the chill thickness as:
$$t_{chill} = \left(50\% \text{ to } 100\%\right) t_{wall}$$
$$t_{cool} \le 2 \text{ h}$$
For low-temperature high-toughness ductile iron casting, the matrix requirements are strict. Pearlite and phosphide content should be below 10%, but because they strongly affect low-temperature toughness, the ferrite content in the matrix should exceed 95%. Heavy-section ductile iron casting often solidifies unevenly. The core may contain cementite and phosphide eutectic in the as-cast structure, and ferrite boundaries may coexist with some pearlite. Therefore, when cementite and phosphide content exceed about 3% to 4%, I apply graphitizing and ferritizing annealing for parts with high low-temperature performance requirements. A proven heat treatment cycle is to austenitize at 920 °C to 950 °C for 2 h to 5 h, then hold at 720 °C to 750 °C for 3 h to 6 h to promote austenite decomposition and graphitization, followed by furnace cooling to 600 °C and air cooling. This can eliminate cementite, phosphide eutectic, and pearlite, transform the matrix to ferrite, and significantly improve low-temperature toughness. The key expressions are:
$$T_{austenitize} = 920^\circ C \text{ to } 950^\circ C,\quad t = 2 \text{ h to } 5 \text{ h}$$
$$T_{graphitize} = 720^\circ C \text{ to } 750^\circ C,\quad t = 3 \text{ h to } 6 \text{ h}$$
$$T_{stress-relief} = 550^\circ C \text{ to } 650^\circ C,\quad t = 2 \text{ h to } 8 \text{ h}$$
$$v_{heat} \le 60^\circ C/h \text{ to } 100^\circ C/h$$
$$v_{furnace} \approx 40^\circ C/h$$
$$v_{air} \ge 120^\circ C/h$$
I also avoid the temper embrittlement range of approximately 400 °C to 600 °C during cooling. When I specify heat treatment for a low-temperature ductile iron casting, I combine the graphitizing anneal with a stress-relief step when the geometry is complex or when dimensional stability is critical. The following table summarizes the heat treatment logic I use.
| Stage | Temperature | Time | Purpose |
|---|---|---|---|
| High-temperature graphitization | 920–950 °C | 2–5 h | Austenitization, dissolution of carbides, homogenization |
| Low-temperature graphitization | 720–750 °C | 3–6 h | Austenite decomposition, graphite precipitation, ferrite formation |
| Furnace cooling to 600 °C | 600 °C endpoint | Controlled rate | Prevents residual stress and avoids air-cooling shock |
| Stress relief | 550–650 °C | 2–8 h | Relaxes casting and machining stresses |
| Final cooling | Air cooling | ≥ 120 °C/h when appropriate | Restores ambient condition without embrittlement |
I use quantitative microstructure targets to judge whether a ductile iron casting is acceptable for low-temperature service. Nodularity, graphite count, ferrite fraction, pearlite fraction, phosphide content, and cementite content are all important. I express nodularity as:
$$N = \frac{A_{nodular}}{A_{total}} \times 100\%$$
I express ferrite fraction as:
$$F_{\alpha} = \frac{A_{\alpha}}{A_{total}} \times 100\%$$
For low-temperature high-toughness ductile iron casting, I often target:
$$F_{\alpha} \ge 95\%$$
$$F_{P+Ph} \le 10\%$$
$$F_{cementite+phosphide} \le 3\% \text{ to } 4\%$$
These targets are not arbitrary. They reflect the fact that ferrite is tough and ductile at low temperature, while pearlite, cementite, and phosphide eutectic act as brittle phases and crack initiation sites. In my view, a low-temperature ductile iron casting cannot be judged only by tensile strength. Impact energy at low temperature, fatigue resistance, and defect tolerance must be considered together.
I also rely on software simulation to integrate composition design, solidification, cooling, and heat treatment. JMatPro is useful for composition design of steel, aluminum, magnesium, and other metallic materials. It can simulate phase transformations and property changes based on theoretical composition, melting temperature, and cooling conditions, and it can predict as-cast microstructure and mechanical properties. However, it does not directly predict mold filling and casting defects. For filling and solidification, I use ProCast, Magma, Flow3D, Anycasting, CAE/CAM, and ANSYS. These tools allow precise modeling from CAD systems, meshing with tools such as Abaqus, assignment of material properties, and simulation of liquid metal filling and cooling. They help me find casting defects early and optimize gating, parting surfaces, chills, and process parameters. Magma is highly specialized, while domestic software such as Huazhu is also used in some production environments. Physical simulation is another effective method for analyzing graphite formation and predicting microstructure and properties. In my experience, simulation is most valuable when it is calibrated with actual ductile iron casting trials and microstructure data.
| Tool category | Example functions | Main output for ductile iron casting |
|---|---|---|
| Thermodynamic and property simulation | JMatPro and related models | Phase transformation, equilibrium phases, as-cast microstructure, mechanical property estimates |
| Filling and solidification simulation | ProCast, Magma, Flow3D, Anycasting | Misrun, cold shut, shrinkage porosity, hot spots, filling velocity, temperature field |
| CAD and CAE integration | CAD, CAE/CAM, ANSYS | Geometry optimization, meshing, stress analysis, cooling channel design |
| Physical simulation | Thermal-physical experiments and graphite analysis | Graphite nucleation, growth, nodularity prediction, process window validation |
| Dynamic process control | Online sulfur measurement and addition models | Nodularizer and inoculant dosing, treatment effect prediction, quality traceability |
In the wind energy field, heavy-section ductile iron casting is already widely applied. Many foundries have mature experience with medium- and small-size, lower-power hubs, base plates, and nacelle covers, and they also have some experience with low-temperature ferritic ductile iron. However, for large-power offshore wind turbine components, the technical barrier remains high. I have observed that the most demanding parts are the hub, nacelle elbow, and main shaft because they combine large section size, complex geometry, high fatigue loading, and low-temperature toughness requirements. The production capability for these parts depends on tight control of raw materials, melting, nodularization, inoculation, molding, cooling, heat treatment, and inspection. In my first-person assessment, the difference between an ordinary ductile iron casting and a reliable low-temperature offshore ductile iron casting lies in the consistency of every step, not in a single miracle additive.
Looking forward, I believe that intelligent software and equipment will become more important. I want to see stronger integration among industry, universities, and research institutes, and I want advanced numerical simulation and software simulation to be used more widely in product design and production. Examples include quantitative analysis of graphite state, prediction of as-cast microstructure and properties, and precise control of composition design, microstructure prediction, and production process for low-temperature high-toughness heavy-section ductile iron casting. High-precision, intelligent production and inspection systems can help achieve scientific, accurate, and efficient quantitative and qualitative analysis, which will raise the quality level of ductile iron casting.
I also expect innovation in the production process for ultra-large wall thickness components. There is an urgent need and potential value in producing ultra-large-tonnage, ultra-large-wall-thickness low-temperature tough ductile iron casting parts. I would combine simulation and physical experiments to study the fundamental theory of heavy-section ductile iron casting, including graphite nucleation, growth, degeneration, segregation, shrinkage, and cooling-rate effects. New theoretical understanding should support the next generation of ductile iron casting materials and processes.
Finally, green production and recycling must guide the future. I respond to carbon-reduction policy by promoting green and environmentally friendly melting and production technologies. I want to improve conventional casting methods, increase process economy, reduce material and energy waste, and use advanced green and intelligent production concepts to guide development. For me, the future of low-temperature high-toughness ductile iron casting is not only about higher strength or lower temperature toughness; it is about producing complex, heavy, reliable, and sustainable ductile iron casting components with predictable quality and lower environmental burden.
To summarize my first-person technical position, I treat low-temperature high-toughness ductile iron casting for wind turbines as a system problem. The charge must be pure, the carbon equivalent must be balanced, the nodularizer and inoculant must be precisely controlled, the pouring temperature and time must be disciplined, the mold and cooling design must be robust, and the heat treatment must stabilize a ferrite-rich matrix. I verify the result through microstructure quantification, mechanical testing, simulation, and production data. When these elements are aligned, a heavy-section ductile iron casting can meet the demanding requirements of offshore wind service; when any one element is neglected, defects such as graphite flotation, chunky graphite, nodularization fading, shrinkage porosity, and brittle phases can degrade the final ductile iron casting. This is why I continue to emphasize integrated process control, digital simulation, and green manufacturing for every critical ductile iron casting.