
I began this work with a practical production problem in large steel castings. In my lost foam casting route, the pattern is made from foam blocks that are cut, glued, assembled, coated, and then placed in a flask. Resin sand flows around the pattern, is compacted, and hardens into a mold. The lost foam casting pattern is intended to support the sand, maintain dimensional accuracy, and later be extracted so that the mold cavity can receive liquid steel. However, during resin sand molding, the lost foam casting pattern experiences mechanical pressure, exothermic heat, adhesive drag, and vacuum or suction-like effects. When the pattern strength is insufficient, the lost foam casting pattern deforms, burns, delaminates, or breaks during extraction. The result is a semi-finished sand mold with dimensional deviation, poor surface quality, and a higher risk of casting defects. I therefore used TRIZ as a structured method to convert this shop-floor problem into a set of TRIZ problem models and to develop a robust solution for improving lost foam casting pattern strength.
My first-person approach was deliberately systematic. I did not begin with a preferred technical answer. Instead, I treated the lost foam casting system as a function system, then used cause-and-effect chain analysis, technical contradiction analysis, and substance-field modeling. I evaluated the resulting ideas with weighted criteria covering implementation cycle, difficulty, cost, and effect. The final combined solution was not a single change but a family of coordinated measures applied to the lost foam casting pattern and the resin sand molding process. The central aim was to increase the effective strength of the lost foam casting pattern while reducing heat damage and extraction resistance.
Functional Analysis of the Lost Foam Casting System. I defined the technical system as the complete set of elements that transform resin sand into a semi-finished sand mold around a lost foam casting pattern. The main components are the flask, the resin sand, the lost foam casting pattern, the compaction tool, the sand mixer, and the operator. The principal object being changed is the resin sand. The lost foam casting pattern acts as a temporary shape former and support body. The flask contains the sand, the mixer delivers sand, the operator compacts the sand, and the compaction tool transmits force into the sand mass. After the resin sand cures, the lost foam casting pattern is extracted, leaving a cavity that represents the desired casting shape.
| Component | Function in Lost Foam Casting | Useful Effect | Harmful Effect |
|---|---|---|---|
| Flask | Contains and supports resin sand | Maintains mold shape | Restricts access during extraction |
| Resin sand | Forms the mold cavity after curing | Transfers shape and supports liquid steel | Exerts pressure and heat on the lost foam casting pattern |
| Lost foam casting pattern | Defines mold cavity geometry | Lightweight, low-cost, easy to machine | Low strength, heat-sensitive, adhesive to sand |
| Compaction tool | Compacts resin sand | Increases mold density and stability | Creates local high pressure on the lost foam casting pattern |
| Sand mixer | Mixes and delivers resin sand | Provides consistent sand flow | Can deliver sand with high temperature |
| Operator | Controls sand flow and compaction | Adjusts process to mold geometry | Method variation can increase damage risk |
I represented the main useful function of the system as a transformation from resin sand to a cured mold:
$$F_{\mathrm{system}}: S_{\mathrm{sand}} \xrightarrow{F_{\mathrm{cure}}} S_{\mathrm{mold}}$$
I also represented the harmful interactions that degrade the lost foam casting pattern. The mechanical pressure from resin sand acts on the pattern surface:
$$F_{\mathrm{mech}}^{\mathrm{harmful}} = p_{\mathrm{contact}} A_{\mathrm{contact}}$$
The thermal load from resin sand and resin reaction acts through conduction, convection, and chemical heat:
$$Q_{\mathrm{thermal}} = h A \left(T_{\mathrm{sand}} – T_{\mathrm{pattern}}\right) + \dot{q}_{\mathrm{resin}} V_{\mathrm{sand}}$$
The extraction force that must be overcome when removing the lost foam casting pattern can be written as a sum of normal friction, adhesion, and suction:
$$F_{\mathrm{ext}} = \mu N + F_{\mathrm{adhesion}} + F_{\mathrm{suction}}$$
From the functional model, I identified three high-priority problem statements. First, resin sand pressure is harmful to the lost foam casting pattern. Second, the pattern material has insufficient resistance to compression, bending, and heat. Third, resin sand curing and temperature variation are not stable enough, which affects the semi-finished mold quality. These statements guided the next TRIZ step.
Cause-and-Effect Chain Analysis. I used cause-and-effect chain analysis to move from the visible failure, insufficient strength of the lost foam casting pattern, to the underlying causes. The visible failures included deformation of the lost foam casting pattern, surface burning, coating unevenness, block separation, and extraction damage. I traced these failures backward and found several key causes. The pattern receives high pressure from resin sand. The sand cooling system has limited capacity, so sand temperature remains high. The glued joints between foam blocks have insufficient clamping force. The pattern density is not high enough in some regions. The pattern structure is not uniform, especially where curved surfaces and thin walls meet. The coating thickness is uneven. The extraction resistance is high because resin sand adheres to the pattern.
| Observed Failure | Intermediate Cause | Key Root Cause | TRIZ Direction |
|---|---|---|---|
| Lost foam casting pattern deformation | High compressive pressure | Resin sand pressure is large | Reduce harmful force or add counter-support |
| Surface burning and charring | High sand temperature | Cooling capacity is low | Local quality, thermal insulation, heat removal |
| Block opening or delamination | Weak glued joints | Clamping force is insufficient | Add mechanical fastening and clamping fixtures |
| Local collapse or crushing | Low local density | Foam density is insufficient | Increase local density or add rigid inserts |
| Uneven coating and weak skin | Nonuniform structure | Curved and complex geometry | Segmentation, asymmetry, vibration-assisted coating |
| Extraction breakage | High friction and adhesion | Resin sand grips the pattern | Introduce release layers, smooth panels, lifting aids |
I expressed the strength condition of the lost foam casting pattern as a comparison between allowable stress and demand stress:
$$\sigma_{\mathrm{demand}} = \frac{F_{\mathrm{mech}}}{A_{\mathrm{load}}} + \frac{M c}{I} + \sigma_{\mathrm{thermal}}$$
$$\sigma_{\mathrm{allow}} = \frac{\sigma_{\mathrm{foam}}(T,t)}{FS}$$
Failure occurs when:
$$\sigma_{\mathrm{demand}} > \sigma_{\mathrm{allow}}$$
The thermal degradation of the lost foam casting pattern can be approximated by an Arrhenius-type relationship:
$$k_{\mathrm{decomp}} = A \exp\left(-\frac{E_a}{RT}\right)$$
This means that even a moderate increase in sand temperature can sharply increase the decomposition rate and reduce the effective strength of the lost foam casting pattern. I also used a transient heat conduction expression to understand how quickly heat reaches the pattern surface:
$$T(x,t) = T_0 + \left(T_s – T_0\right)\mathrm{erfc}\left(\frac{x}{2\sqrt{\alpha t}}\right)$$
In this expression, \(x\) is depth from the surface, \(t\) is time, and \(\alpha\) is thermal diffusivity. The slower the heat penetration, the more strength remains in the lost foam casting pattern during molding and extraction. These equations helped me see that improving lost foam casting strength is not only a matter of material density. It is also a matter of reducing thermal load, interrupting heat paths, adding local reinforcement, and lowering extraction resistance.
Technical Contradiction One: Structure Stability versus Shape. I formulated the first technical contradiction from the need to make the coating more uniform. If I change the lost foam casting pattern structure to a simpler shape, then the coating becomes more stable and uniform. However, the product shape is changed, which is unacceptable. If I do not change the structure, then the product shape remains correct, but the coating on the lost foam casting pattern remains unstable. In TRIZ terms, I was improving the stability of the structure while worsening the shape parameter.
$$TC_1: P_{13} \uparrow \Rightarrow P_{12} \downarrow$$
| Contradiction Statement | Improving Parameter | Worsening Parameter | Selected Inventive Principles |
|---|---|---|---|
| If the lost foam casting pattern structure is changed, coating stability improves but product shape is altered | Stability of structure | Shape | Segmentation, turning harm into benefit, vibration, asymmetry |
| If the structure is not changed, shape is correct but coating stability remains poor | Shape | Stability of structure | Local quality, composite, porous material |
Using the segmentation principle, I developed the idea of separating the lost foam casting pattern into curved regions and flat side regions. The curved regions can be supported by strike boards or sand forms, while the flat regions can still use lost foam casting pattern blocks. This reduces the unsupported foam area and improves local strength. Using the vibration principle, I proposed vibrating the lost foam casting pattern during coating so that the coating spreads more evenly over complex surfaces. Using the asymmetry principle, I accepted that not all regions need the same treatment. Critical regions can receive thicker coating, extra ribs, or local inserts, while noncritical regions remain lightweight. This is important because overbuilding the entire lost foam casting pattern would increase cost and weight without solving the local failure modes.
Technical Contradiction Two: Strength versus Material Loss. I formulated the second technical contradiction from the high sand temperature problem. If I lower the resin sand temperature, then the lost foam casting pattern suffers less burning and retains higher strength. However, lowering the temperature reduces the amount of reclaimed sand that can be reused. If I do not lower the temperature, then sand reuse remains high, but the lost foam casting pattern is burned and weakened. In TRIZ terms, I was improving strength while worsening material loss.
$$TC_2: P_{14} \uparrow \Rightarrow P_{23} \downarrow$$
| Contradiction Statement | Improving Parameter | Worsening Parameter | Selected Inventive Principles |
|---|---|---|---|
| If sand temperature is reduced, lost foam casting pattern strength increases but sand reuse decreases | Strength | Loss of substance | Local quality, merging, mechanical substitution, porous material, composite |
| If sand temperature is not reduced, sand reuse remains high but lost foam casting pattern burns and weakens | Loss of substance | Strength | Thermal insulation, local reinforcement, pre-compensation |
Using the local quality principle, I proposed adding extra thickness allowance to regions of the lost foam casting pattern that are prone to burning and collapse. The pattern is intentionally made slightly thicker or pre-shaped in the opposite direction so that after thermal and mechanical deformation it arrives at the required shape. I also proposed a special hardening layer on heat-sensitive regions. This layer increases surface strength and reduces heat transfer into the foam. Using the porous material principle, I proposed local holes or porous inserts in the lost foam casting pattern. The holes can be filled with pre-cured resin sand or a lightweight insulating material, creating local support columns and interrupting direct thermal pathways. These measures improve lost foam casting pattern strength without requiring a full change of the sand reclamation system.
Substance-Field Modeling for Mechanical Pressure. I modeled the mechanical problem as a harmful interaction between the lost foam casting pattern and resin sand. The pattern is \(S_1\), the resin sand is \(S_2\), and the mechanical field is \(F_{\mathrm{mech}}\). The basic harmful model is:
$$S_1 \xrightarrow{F_{\mathrm{mech}}} S_2$$
In this model, the mechanical field from resin sand acts on the lost foam casting pattern and produces deformation, local crushing, and extraction resistance. The standard TRIZ direction is to introduce a third substance \(S_3\) or a second field \(F_2\) to redirect or counteract the harmful effect. I therefore considered adding a rigid skeleton, a release layer, a smooth surface panel, or a lifting structure to the lost foam casting pattern.
| Substance-Field Problem | Harmful Interaction | Introduced Substance or Field | Solution Direction |
|---|---|---|---|
| Resin sand presses on lost foam casting pattern | Mechanical pressure | Smooth panel or pressure plate | Distribute load and reduce surface damage |
| Thin walls deform under sand pressure | Bending and buckling | Extraction auxiliary belt | Add local stiffness and balanced extraction force |
| Extraction force breaks the pattern | Friction, adhesion, suction | Lifting pad or rigid skeleton | Increase extraction strength and reduce local stress |
| Pattern collapses during sand filling | Compressive instability | Internal reinforcement | Carry load internally and protect geometry |
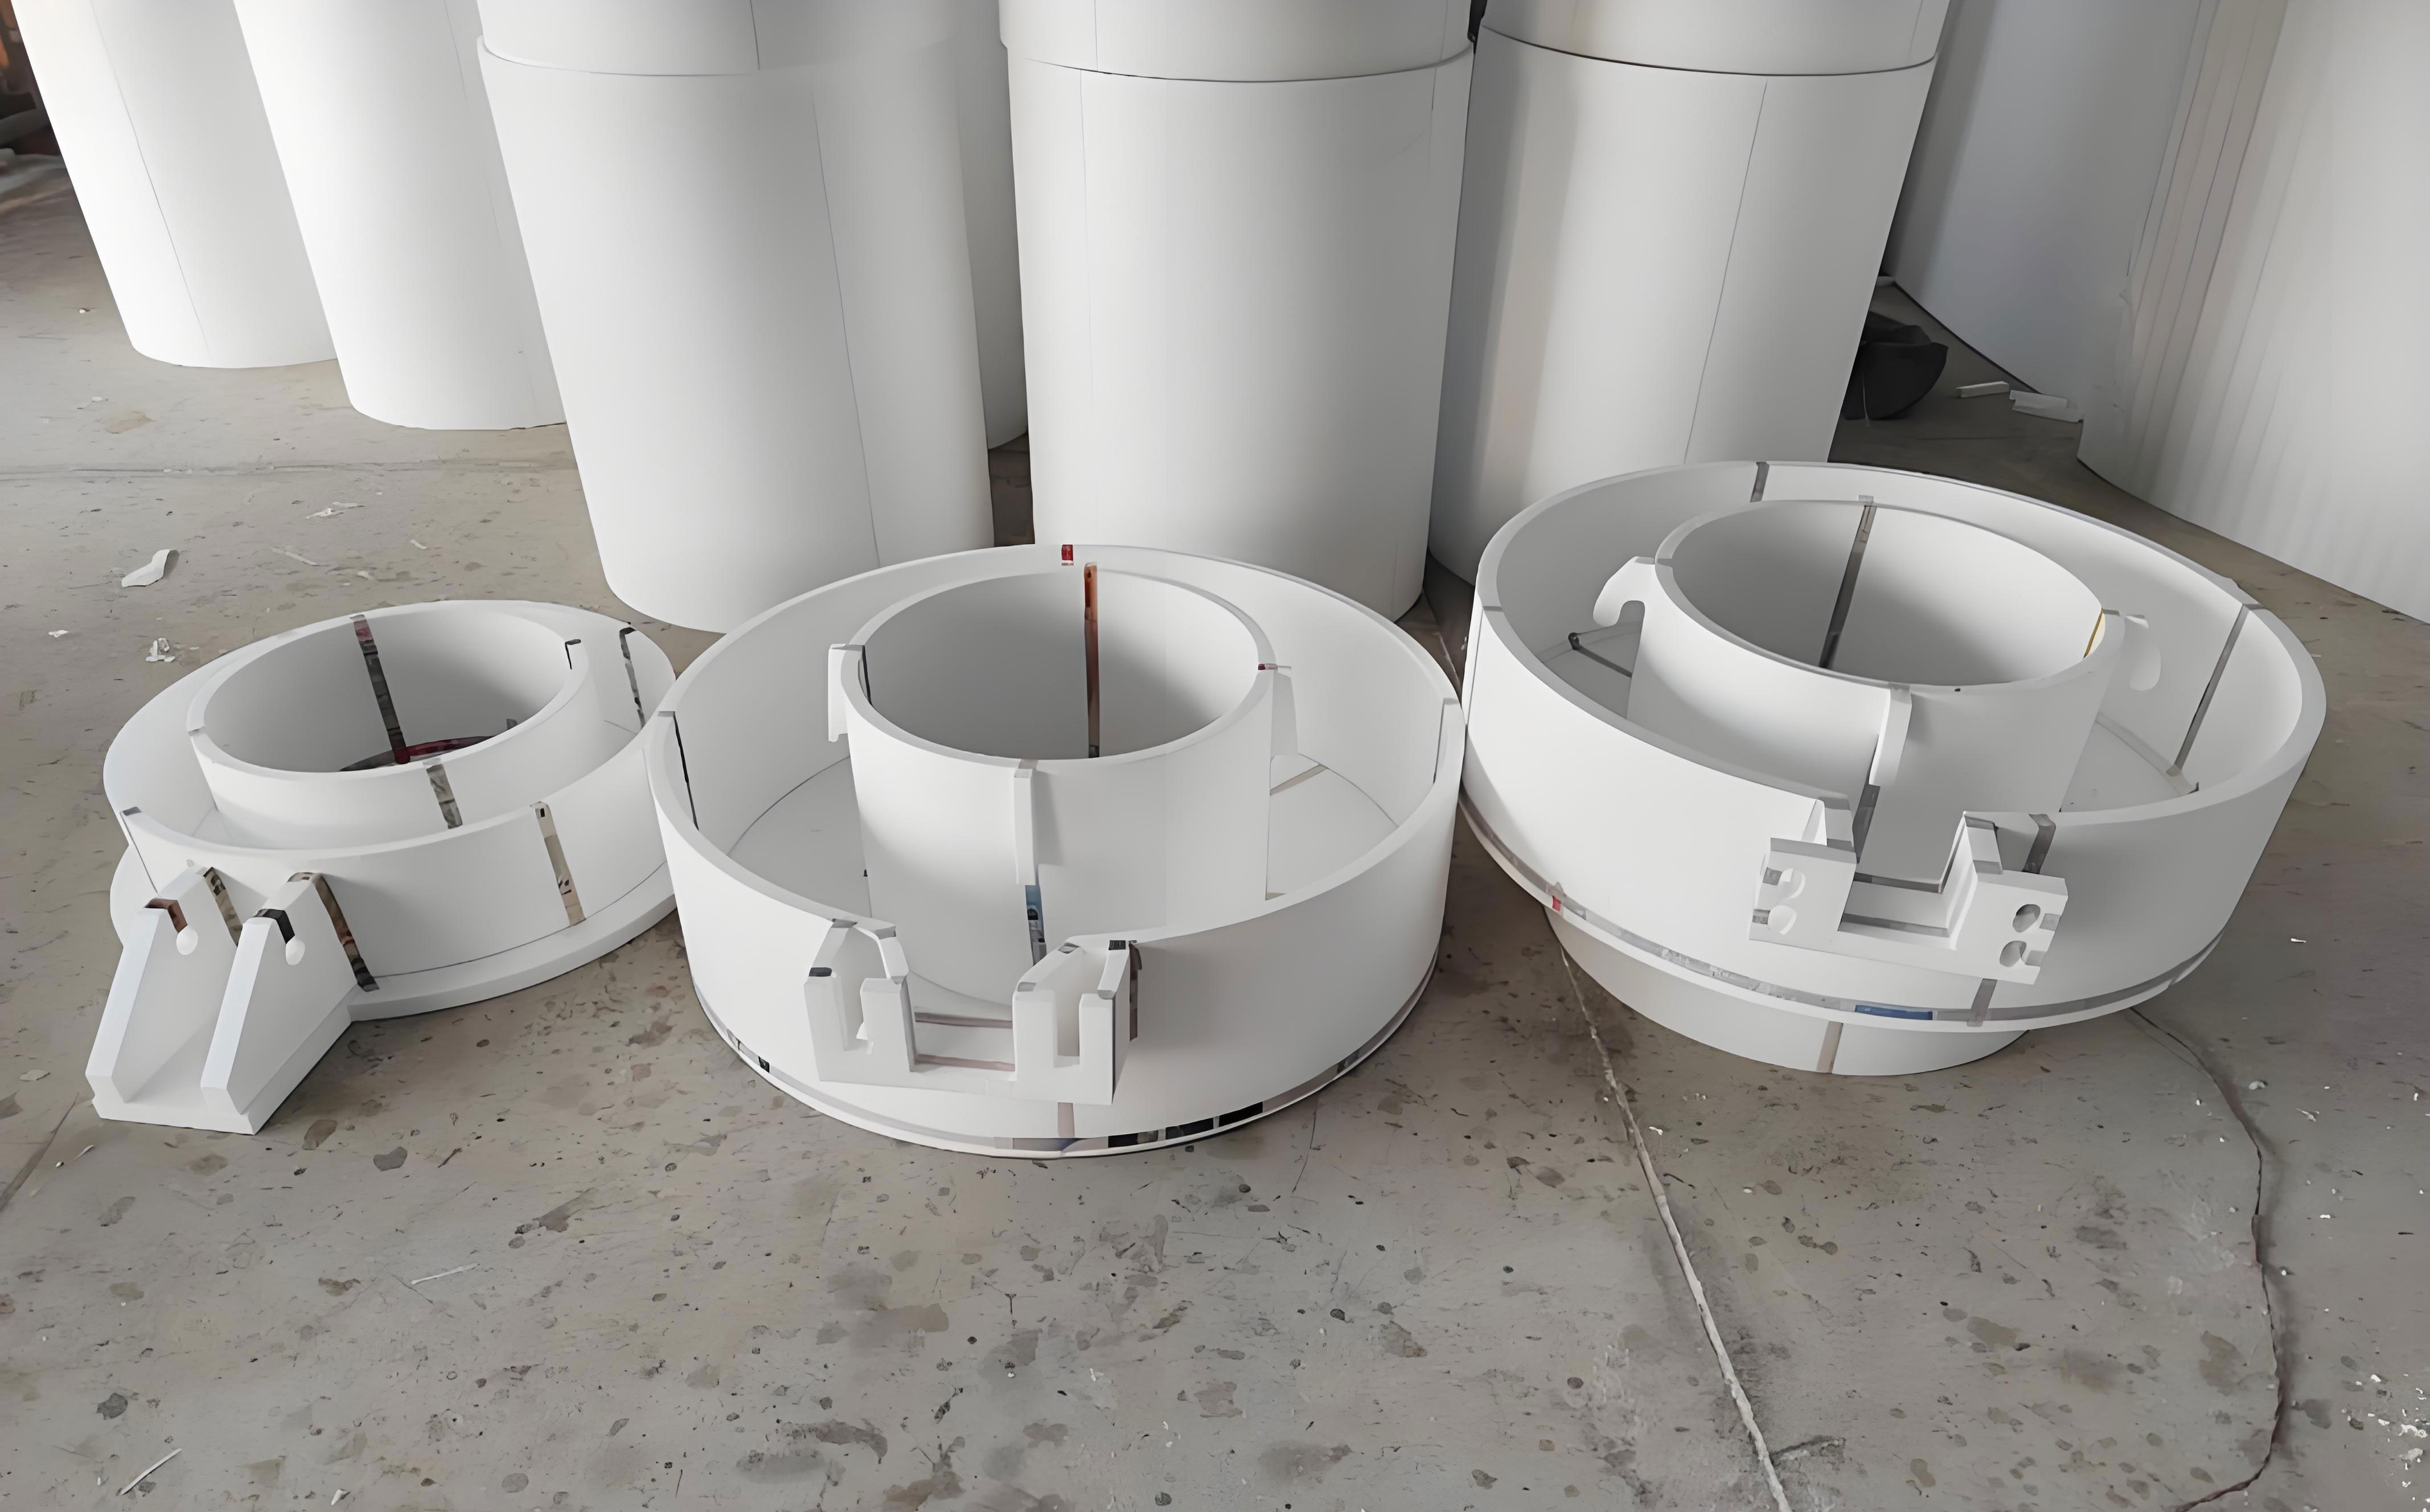
For the mechanical model, I developed several concrete solution ideas. The first was to replace critical flat surfaces with removable pressure plates. A high-density wooden board or composite plate can be placed on high-pressure regions of the lost foam casting pattern. The plate distributes the sand load and can be easily replaced when worn. The second idea was to add an extraction auxiliary belt to thin-walled cylinder-like structures. This belt acts as a local rib and balances the extraction force so that the lost foam casting pattern is less likely to tear. The third idea was to add lifting pads at extraction points. These pads increase the local cross-section and provide a strong point for lifting. After extraction, the pad impression can be filled with sand or repaired. The fourth idea was to add a rigid internal skeleton. The skeleton supports the lost foam casting pattern against sand pressure and provides an attachment point for extraction devices. The skeleton must be designed so that it does not interfere with the final casting shape and can be removed or left in a controlled way.
Substance-Field Modeling for Thermal Load. I modeled the thermal problem as a harmful interaction between resin sand and the lost foam casting pattern. The resin sand is \(S_2\), the lost foam casting pattern is \(S_1\), and the thermal field is \(F_{\mathrm{thermal}}\). The basic harmful model is:
$$S_1 \xrightarrow{F_{\mathrm{thermal}}} S_2$$
To reduce the harmful effect, I introduced an insulating or heat-resistant substance \(S_3\) between the pattern and the sand, or I introduced a cooling field \(F_2\) to remove heat. The most practical local solution was to insert wooden wedges or insulating inserts at multi-face regions where sand contact is high and burning is likely. The wedge reduces heat transfer and adds local surface strength. Another option was a special coating that reflects or absorbs heat, delays temperature rise, and hardens the surface of the lost foam casting pattern. I also considered local cooling by using pre-cooled sand or by improving sand cooling before molding. However, because sand reclamation and reuse are economically important, I did not rely only on global sand cooling. I combined local thermal protection with local mechanical reinforcement.
| Thermal Problem | Harmful Effect | Local TRIZ Solution | Expected Result |
|---|---|---|---|
| High resin sand temperature | Burning and charring of lost foam casting pattern | Insulating coating and wooden inserts | Lower surface temperature and less strength loss |
| Exothermic resin reaction | Local hot spots and glue failure | Local cooling and heat-resistant adhesive | Stable joints and reduced delamination |
| Heat concentration at thick sand sections | Uneven thermal load | Porous inserts and sand-filled cavities | Interrupted heat path and local support |
| Thermal deformation during curing | Shape deviation | Pre-compensation allowance | Final shape after deformation matches target |
Solution Register. I collected the TRIZ-generated ideas into a solution register. Each solution addresses one or more root causes and can be combined with others. I deliberately kept the register broad at first, then narrowed it through evaluation.
| Solution ID | Description | Main TRIZ Tool | Target Problem |
|---|---|---|---|
| S1 | Add replaceable pressure plates on high-load surfaces of the lost foam casting pattern | Technical contradiction | High sand pressure and surface damage |
| S2 | Add low-density foam material into resin sand to reduce bulk pressure | Technical contradiction | High sand pressure |
| S3 | Add clamping fixtures, wooden wedges, or bolts to foam block joints | Technical contradiction | Weak glued joints and block separation |
| S4 | Split curved regions and planar regions; use strike boards for curved regions | Segmentation principle | Nonuniform structure and coating |
| S5 | Vibrate the lost foam casting pattern during coating | Vibration principle | Uneven coating thickness |
| S6 | Add pre-deformation allowance at hot and high-pressure zones | Local quality principle | Thermal and mechanical deformation |
| S7 | Apply a special hardening and heat-blocking coating on vulnerable regions | Local quality principle | Burning and low surface strength |
| S8 | Create local holes or porous inserts filled with pre-cured sand for support and heat interruption | Porous material principle | Thermal load and local collapse |
| S9 | Replace parting-line surfaces with smooth panels to reduce extraction friction | Substance-field model | Extraction resistance |
| S10 | Add an extraction auxiliary belt to thin-walled structures | Substance-field model | Extraction damage and wall deformation |
| S11 | Add lifting pads at extraction points to increase local cross-section | Substance-field model | Extraction breakage |
| S12 | Add a rigid internal skeleton with an extraction device | Substance-field model | Collapse and extraction weakness |
| S13 | Insert wooden wedges at multi-face heat-prone regions | Substance-field model | Thermal burning and surface strength |
Weighted Evaluation. I evaluated the solutions using four criteria: implementation cycle, difficulty, cost, and effect. The weights were set as 10 percent for cycle, 20 percent for difficulty, 30 percent for cost, and 40 percent for effect. I scored each criterion from 1 to 10, where higher is better. The weighted score is:
$$S_j = 10\left(0.10 S_{\mathrm{cycle}} + 0.20 S_{\mathrm{difficulty}} + 0.30 S_{\mathrm{cost}} + 0.40 S_{\mathrm{effect}}\right)$$
The multiplication by 10 converts the result to a 100-point scale. I used this evaluation not to find a single perfect idea, but to identify the strongest combination of ideas that could be implemented in the lost foam casting process.
| Solution | Cycle | Difficulty | Cost | Effect | Score | Rank |
|---|---|---|---|---|---|---|
| S10 extraction auxiliary belt | 5 | 8 | 8 | 10 | 85 | 1 |
| S7 special hardening coating | 4 | 6 | 9 | 10 | 83 | 2 |
| S11 lifting pads | 7 | 8 | 8 | 7 | 75 | 3 |
| S1 pressure plates | 3 | 9 | 6 | 9 | 75 | 3 |
| S8 porous inserts | 5 | 7 | 8 | 8 | 75 | 3 |
| S6 pre-deformation allowance | 5 | 8 | 9 | 6 | 72 | 4 |
| S12 rigid skeleton | 3 | 6 | 7 | 9 | 72 | 4 |
| S4 curved and planar split | 5 | 7 | 4 | 8 | 63 | 5 |
| S9 smooth panels | 8 | 8 | 7 | 4 | 61 | 6 |
| S3 clamping fixtures | 4 | 5 | 6 | 7 | 60 | 7 |
| S13 wooden wedges | 3 | 6 | 5 | 7 | 58 | 8 |
| S5 vibration-assisted coating | 5 | 4 | 6 | 6 | 55 | 10 |
| S2 low-density foam in sand | 2 | 5 | 6 | 6 | 54 | 11 |
The top-ranked solutions were S10, S7, S11, S1, and S8. I then formed a combined solution because the failure modes are not independent. A thin wall that is protected by coating but not supported during extraction may still tear. A pressure plate that distributes sand load may still allow heat damage at an unprotected region. A lifting pad that increases extraction strength may be ineffective if the surrounding lost foam casting pattern is already burned and weak. Therefore, the best result came from combining local reinforcement, thermal protection, and extraction aids.
Combined Solution for Lost Foam Casting Pattern Strength. The combined solution I selected included the following elements. First, I added an extraction auxiliary belt to thin-walled and tall structures. This belt acts as a temporary local rib. It increases the section modulus and distributes extraction force. Second, I applied a special hardening and heat-blocking coating to vulnerable regions. This coating raises surface strength and delays heat penetration into the lost foam casting pattern. Third, I added lifting pads at extraction points. These pads provide a strong lifting location and reduce local stress concentration. Fourth, I installed replaceable pressure plates on high-load flat surfaces. These plates distribute sand pressure and can be replaced when worn. Fifth, I added local porous inserts or sand-filled support columns where heat and pressure are concentrated. Sixth, I used pre-deformation allowance at known hot and high-pressure zones so that the final mold cavity remains within tolerance after the lost foam casting pattern deforms.
| Combined Measure | Primary Function | Secondary Benefit | Applied Region |
|---|---|---|---|
| Extraction auxiliary belt | Increase local stiffness | Balance extraction force | Thin walls, cylinders, deep cavities |
| Hardening and heat-blocking coating | Increase surface strength | Reduce burning and charring | Heat-prone and wear-prone surfaces |
| Lifting pads | Provide strong extraction points | Reduce local tearing | Extraction lugs and corners |
| Pressure plates | Distribute sand load | Reduce surface damage and friction | Large flat surfaces, parting planes |
| Porous inserts or sand-filled supports | Support local geometry | Interrupt heat path | Thick sand sections and hot spots |
| Pre-deformation allowance | Compensate thermal and mechanical deformation | Improve final dimensional accuracy | Known hot and high-pressure zones |
I expressed the combined strength of the improved lost foam casting pattern as the sum of the base foam strength and the contributions of the added features:
$$\sigma_{\mathrm{eff}}(T,t) = \sigma_{\mathrm{foam}}(T,t) + \Delta\sigma_{\mathrm{plate}} + \Delta\sigma_{\mathrm{rib}} + \Delta\sigma_{\mathrm{coating}} + \Delta\sigma_{\mathrm{support}}$$
The safety factor of the improved design is then:
$$FS_{\mathrm{new}} = \frac{\sigma_{\mathrm{eff}}(T,t)}{\sigma_{\mathrm{demand}}}$$
I required \(FS_{\mathrm{new}} \ge 1.5\) for critical regions and \(FS_{\mathrm{new}} \ge 1.2\) for noncritical regions. This gave a clear engineering target rather than a subjective judgment. The thermal protection effect can be approximated by a thermal resistance network:
$$q” = \frac{T_{\mathrm{sand}} – T_{\mathrm{pattern}}}{R_{\mathrm{coating}} + R_{\mathrm{plate}} + R_{\mathrm{contact}}}$$
If the allowable heat flux into the lost foam casting pattern is \(q”_{\mathrm{allow}}\), the required insulation thickness can be estimated by:
$$t_{\mathrm{ins}} = k\left(\frac{T_{\mathrm{sand}} – T_{\mathrm{pattern}}}{q”_{\mathrm{allow}}} – R_{\mathrm{other}}\right)$$
These equations helped me select coating thickness and insert dimensions. I did not need a perfect numerical model to make progress, but the formulas made the trade-offs visible. Increasing coating thickness improves thermal protection but can increase coating drying time and cost. Increasing plate thickness improves mechanical support but can increase weight and handling difficulty. Increasing extraction belt size improves extraction strength but can affect local mold geometry. The final dimensions were therefore chosen as a balance, not as an extreme.
Extraction Force Reduction. Extraction damage was one of the most serious failure modes in the lost foam casting pattern. I modeled the extraction force as a combination of friction, adhesion, and suction. The new design reduces each component:
$$F_{\mathrm{ext,new}} = F_{\mathrm{ext,old}} – \Delta F_{\mathrm{release}} – \Delta F_{\mathrm{belt}} – \Delta F_{\mathrm{pad}} – \Delta F_{\mathrm{smooth}}$$
The release coating and smooth panels reduce friction and adhesion. The extraction belt and lifting pads do not necessarily reduce the total extraction force, but they increase the ability of the lost foam casting pattern to withstand that force. This distinction is important. Sometimes the best solution is not to eliminate the force but to make the structure strong enough to carry it. In other cases, the best solution is to reduce the force itself. I used both strategies together.
| Extraction Force Component | Reduction Method | Strength Increase Method | Combined Effect |
|---|---|---|---|
| Friction \(\mu N\) | Smooth panels and release coating | Lifting pads and belts | Lower force and higher resistance |
| Adhesion \(F_{\mathrm{adhesion}}\) | Hardening coating and surface treatment | Local reinforcement | Less sticking and less tearing |
| Suction \(F_{\mathrm{suction}}\) | Venting and porous inserts | Rigid skeleton | Pressure equalization and support |
| Normal load \(N\) | Pressure plates and sand flow control | Extraction auxiliary belt | Lower local pressure and higher stiffness |
Process Implementation. In implementation, I changed the lost foam casting pattern workflow in several stages. During digital design, I identified high-risk regions using historical defects, sand flow simulation, and thermal maps. During foam block programming, I added local thickness allowance for pre-deformation. During foam machining, I created slots and recesses for pressure plates, lifting pads, and support inserts. During assembly, I combined adhesive bonding with mechanical clamping. Wooden wedges and bolts were used at highly stressed joints. During coating, I applied a base coating and then a hardening and heat-blocking coating on vulnerable regions. I also used vibration assistance when the coating needed to flow into complex corners.
During flasking, I placed the lost foam casting pattern in the flask and positioned pressure plates and support inserts before sand filling. I controlled sand flow to avoid direct impact on thin walls. The operator used compaction tools with care around extraction belts and lifting pads. After resin sand curing, I extracted the lost foam casting pattern using the lifting pads and extraction belt. The pressure plates were removed and inspected. The pattern was cleaned and prepared for the next use. Because the lost foam casting pattern could be reused, the cost benefit increased over multiple cycles.
| Process Stage | Original Practice | Improved Practice | Expected Benefit |
|---|---|---|---|
| Design | Uniform foam pattern | Risk-based local reinforcement | Targeted strength improvement |
| Machining | Simple foam blocks | Slots for plates, pads, and inserts | Easy assembly and replacement |
| Assembly | Glue only | Glue plus mechanical clamping | Higher joint strength |
| Coating | Single manual coating | Base coat plus hard heat-blocking coat | Better surface strength and thermal protection |
| Flasking | Direct sand filling | Plates and inserts installed before filling | Lower pressure damage |
| Extraction | Manual pull on foam | Lifting pads and auxiliary belt | Less extraction damage |
| Reuse | Limited reuse | Inspection, repair, and replacement of local parts | Longer pattern life |
Quantitative Validation. I compared the original and improved lost foam casting pattern performance using several indicators. Deformation rate, surface burn rate, extraction damage rate, dimensional deviation, and reuse count were the main measures. The improved design did not eliminate all variation, but it reduced the severe failure modes. I expressed the improvement ratio for each indicator as:
$$R_i = \frac{M_{\mathrm{old}} – M_{\mathrm{new}}}{M_{\mathrm{old}}} \times 100\%$$
I also used a cost-benefit expression to evaluate whether the combined solution was worth implementing:
$$ROI = \frac{\Delta C_{\mathrm{scrap}} + \Delta C_{\mathrm{rework}} + \Delta C_{\mathrm{reuse}} – \Delta C_{\mathrm{implementation}}}{\Delta C_{\mathrm{implementation}}}$$
| Indicator | Original Condition | Improved Condition | Improvement Direction |
|---|---|---|---|
| Pattern deformation rate | High in thin walls and hot zones | Reduced by local support and pre-compensation | Lower |
| Surface burning rate | High at multi-face sand contact | Reduced by coating and inserts | Lower |
| Extraction damage rate | High for deep cavities | Reduced by belts and lifting pads | Lower |
| Dimensional deviation | Moderate to high | Better controlled | Lower |
| Pattern reuse count | Low | Increased by local repair and replacement | Higher |
| Mold surface quality | Uneven | More uniform | Better |
| Scrap and rework cost | High | Reduced | Lower |
I also monitored the resin sand process. The sand temperature was not reduced globally, because that would have reduced reclaimed sand reuse. Instead, I reduced the thermal load on the lost foam casting pattern locally. This is a classic TRIZ outcome: instead of accepting a global trade-off between strength and material loss, I introduced local quality and local protection. The lost foam casting pattern now has a stronger surface where heat is concentrated and a stronger structure where extraction stress is concentrated. The rest of the pattern remains lightweight and economical.
Why the Combined Solution Works. The combined solution works because it addresses multiple failure mechanisms at the same time. The pressure plates reduce contact pressure and surface friction. The hardening coating increases surface strength and reduces heat penetration. The extraction auxiliary belt increases section modulus. The lifting pads provide a strong extraction point. The porous inserts and sand-filled supports interrupt heat paths and carry local compressive load. The pre-deformation allowance compensates for the remaining deformation. Together, these measures raise the effective strength of the lost foam casting pattern and lower the demand stress.
I expressed the ideal final result of the TRIZ process as a ratio between useful functions and harmful functions plus cost:
$$IFR = \frac{\sum U_i}{\sum H_i + \sum C_i}$$
The goal is not to maximize complexity. The goal is to increase useful functions, reduce harmful effects, and keep cost under control. In my case, the useful functions included shape retention, sand support, thermal protection, and easy extraction. The harmful effects included deformation, burning, adhesion, and extraction damage. The combined solution improved the ratio by adding only local features, not by rebuilding the entire lost foam casting system.
Lessons from the TRIZ Application. I learned that lost foam casting pattern strength is a system property, not only a material property. A higher-density foam may help, but it also increases cost and weight. A lower sand temperature may help, but it reduces sand reuse. A stronger coating may help, but it can crack if the underlying pattern deforms. A larger lifting pad may help, but it can alter local mold geometry. TRIZ helped me avoid a single-variable mindset. By using functional analysis, cause-and-effect chain analysis, technical contradictions, and substance-field modeling, I could see the conflict behind each obvious solution and then find a local, combined answer.
I also learned that the best solution in lost foam casting is often a removable or replaceable solution. Pressure plates, lifting pads, auxiliary belts, and inserts can be removed, replaced, or repaired. This is important because the lost foam casting pattern is used more than once. If the reinforcement is permanent and damaged, the whole pattern may be scrapped. If the reinforcement is modular, only the damaged local element is replaced. This reduces maintenance cost and extends pattern life.
| TRIZ Principle | Application in Lost Foam Casting | Result |
|---|---|---|
| Segmentation | Separate curved and planar regions; use local modules | Simpler coating and targeted reinforcement |
| Local quality | Reinforce only hot and high-load regions | Lower cost and lower weight |
| Porous material | Use inserts or sand-filled cavities | Support and thermal interruption |
| Composite | Combine foam, coating, wood, and plates | Higher effective strength |
| Mechanical substitution | Use lifting pads, belts, and fixtures | Better extraction control |
| Vibration | Vibrate during coating | More uniform coating |
| Turning harm into benefit | Use sand-filled cavities as local supports | Harmful sand becomes support |
Further Optimization and Control. I continued to optimize the combined solution by tracking three variables: local sand pressure, local pattern temperature, and extraction force. These variables can be estimated or measured. The local sand pressure can be approximated by:
$$p_{\mathrm{local}} = \rho_s g h + q_{\mathrm{ram}} + p_{\mathrm{contact}}$$
The local pattern temperature can be estimated from the heat conduction equation. The extraction force can be monitored indirectly by observing damage, or directly by using load cells in the extraction fixture. I used this information to adjust coating thickness, insert size, and pad location. Over time, the lost foam casting pattern design became more standardized. High-risk regions were classified by geometry and process condition, and the corresponding reinforcement was selected from a standard library.
| Control Variable | Estimation or Measurement Method | Adjustment Action |
|---|---|---|
| Local sand pressure | Sand depth, compaction pattern, and historical damage | Increase plate thickness or add support insert |
| Local pattern temperature | Thermal mapping and sand temperature records | Increase coating thickness or add insulating wedge |
| Extraction force | Lifting load, damage observation, and operator feedback | Add lifting pad, belt, or smooth panel |
| Deformation after molding | Dimensional inspection of semi-finished mold | Adjust pre-deformation allowance |
| Surface burning | Visual inspection and pattern reuse count | Modify coating and local insert |
Economic and Environmental Effects. The original lost foam casting route was attractive because foam is low cost and easy to machine. However, when the lost foam casting pattern fails, the cost advantage disappears. Rework, scrap, mold repair, and lost production time create hidden costs. The combined solution improved the economics by extending pattern life, reducing mold repair, and increasing reuse. It also reduced burning and decomposition of the foam, which lowers smoke and fume generation during pouring. Better mold dimensional quality also reduced casting defects and downstream cleaning.
I expressed the total cost of a lost foam casting pattern as:
$$C_{\mathrm{total}} = C_{\mathrm{material}} + C_{\mathrm{machining}} + C_{\mathrm{assembly}} + C_{\mathrm{coating}} + C_{\mathrm{molding}} + C_{\mathrm{repair}} + C_{\mathrm{scrap}}$$
The combined solution increases \(C_{\mathrm{coating}}\), \(C_{\mathrm{assembly}}\), and \(C_{\mathrm{molding}}\) slightly, but it reduces \(C_{\mathrm{repair}}\) and \(C_{\mathrm{scrap}}\) substantially. It also increases the number of reuse cycles \(n\), so the effective cost per mold is:
$$C_{\mathrm{per\,mold}} = \frac{C_{\mathrm{total}}}{n}$$
When \(n\) increases, \(C_{\mathrm{per\,mold}}\) decreases even if the initial pattern cost is higher. This is the economic reason why local reinforcement is valuable in lost foam casting. It is not about making the pattern indestructible. It is about making the pattern reusable, repairable, and dimensionally reliable.
Final Combined Design Logic. The final design logic can be summarized as a sequence. First, identify the high-pressure and high-temperature regions of the lost foam casting pattern. Second, reduce the harmful mechanical effect by pressure plates, smooth panels, and controlled sand flow. Third, reduce the harmful thermal effect by hardening coating, insulating wedges, and porous inserts. Fourth, increase the local strength by extraction belts, lifting pads, and rigid supports. Fifth, compensate for remaining deformation by pre-deformation allowance. Sixth, evaluate the result by dimensional inspection, damage rate, and reuse count. Seventh, standardize the best local solution and apply it to similar lost foam casting patterns.
| Step | Action | Purpose | Output |
|---|---|---|---|
| 1 | Identify risk regions | Focus resources | Risk map of lost foam casting pattern |
| 2 | Reduce mechanical harm | Lower pressure and friction | Pressure plates and smooth panels |
| 3 | Reduce thermal harm | Lower burning and strength loss | Hardening coating and inserts |
| 4 | Increase local strength | Resist extraction and compaction | Belts, pads, and supports |
| 5 | Compensate deformation | Maintain final dimensions | Pre-deformation allowance |
| 6 | Evaluate performance | Verify improvement | Inspection and reuse data |
| 7 | Standardize | Repeat success | Design library for lost foam casting |
Conclusion of My TRIZ Work. I used TRIZ to improve the strength of a lost foam casting pattern in a resin sand molding process. The original problem was that the lost foam casting pattern deformed, burned, delaminated, and broke during molding and extraction. I converted the problem into functional models, cause-and-effect chains, technical contradictions, and substance-field models. I generated a broad solution register and evaluated the ideas with weighted criteria. The highest-value combined solution included an extraction auxiliary belt, a special hardening and heat-blocking coating, lifting pads, replaceable pressure plates, porous or sand-filled support inserts, and pre-deformation allowance. This combined solution increased the effective strength of the lost foam casting pattern, reduced thermal damage, lowered extraction resistance, improved mold dimensional accuracy, and extended pattern reuse.
The most important result is that the improvement came from a structured contradiction-solving process, not from a single material change. The lost foam casting pattern is a temporary tool, but its strength determines the quality of the mold and the final casting. By applying TRIZ, I was able to improve the lost foam casting pattern without losing the economic advantages of low-cost foam. The method can be repeated for other lost foam casting patterns with complex geometry, thin walls, large dimensions, and high sand pressure. It also provides a practical example of how TRIZ can be used in foundry process improvement and casting mold design.