
In my extensive experience with vacuum-assisted lost foam casting (LFC), I have focused on refining processes for thin-wall gray iron shell castings, particularly transmission housings used in automotive and agricultural machinery. These shell castings are critical components that demand high dimensional accuracy, pressure tightness, and lightweight design, making LFC an ideal manufacturing method due to its advantages in reducing defects like sand inclusion and uneven wall thickness compared to traditional sand casting. However, producing high-integrity shell castings with consistent pressure-tightness presents significant challenges, necessitating a systematic optimization of key process parameters. Through orthogonal experimentation and iterative testing, I have developed optimized protocols that enhance the quality and reliability of these thin-wall shell castings.
The production environment for these shell castings involves specific conditions that influence process outcomes. The base sand has a grain size primarily of 20-40 mesh (over 85%), with a mud content ≤0.3%. Coating thickness for the foam patterns ranges from 1.0 to 1.5 mm, with moisture content kept below 1%. We utilize a vacuum-negative pressure production line with 70 sandboxes, each measuring 2050 mm × 1500 mm × 1300 mm, equipped with ventilation on five sides and a vacuum source at the bottom. Pouring is performed using an automatic teapot ladle pouring machine with a maximum capacity of 2100 kg per ladle. These conditions set the stage for producing complex shell castings with wall thicknesses as thin as 5-7 mm.
The shell castings under investigation include three types of transmission housings, designated here for reference. All are made of HT300 gray iron and require hydraulic pressure testing at 3 kg/cm² to ensure leak-proof performance. The first type, a larger housing, has overall dimensions of approximately 780 mm × 450 mm × 440 mm and a weight of 100 kg. The second type measures about 680 mm × 320 mm × 245 mm, also weighing 100 kg. The third is smaller at 440 mm × 420 mm × 380 mm, weighing 68 kg. Common to all these shell castings is a uniform wall thickness of 5-7 mm across the main body, excluding flanges and bosses, which presents challenges in achieving complete filling and dense microstructure without defects.
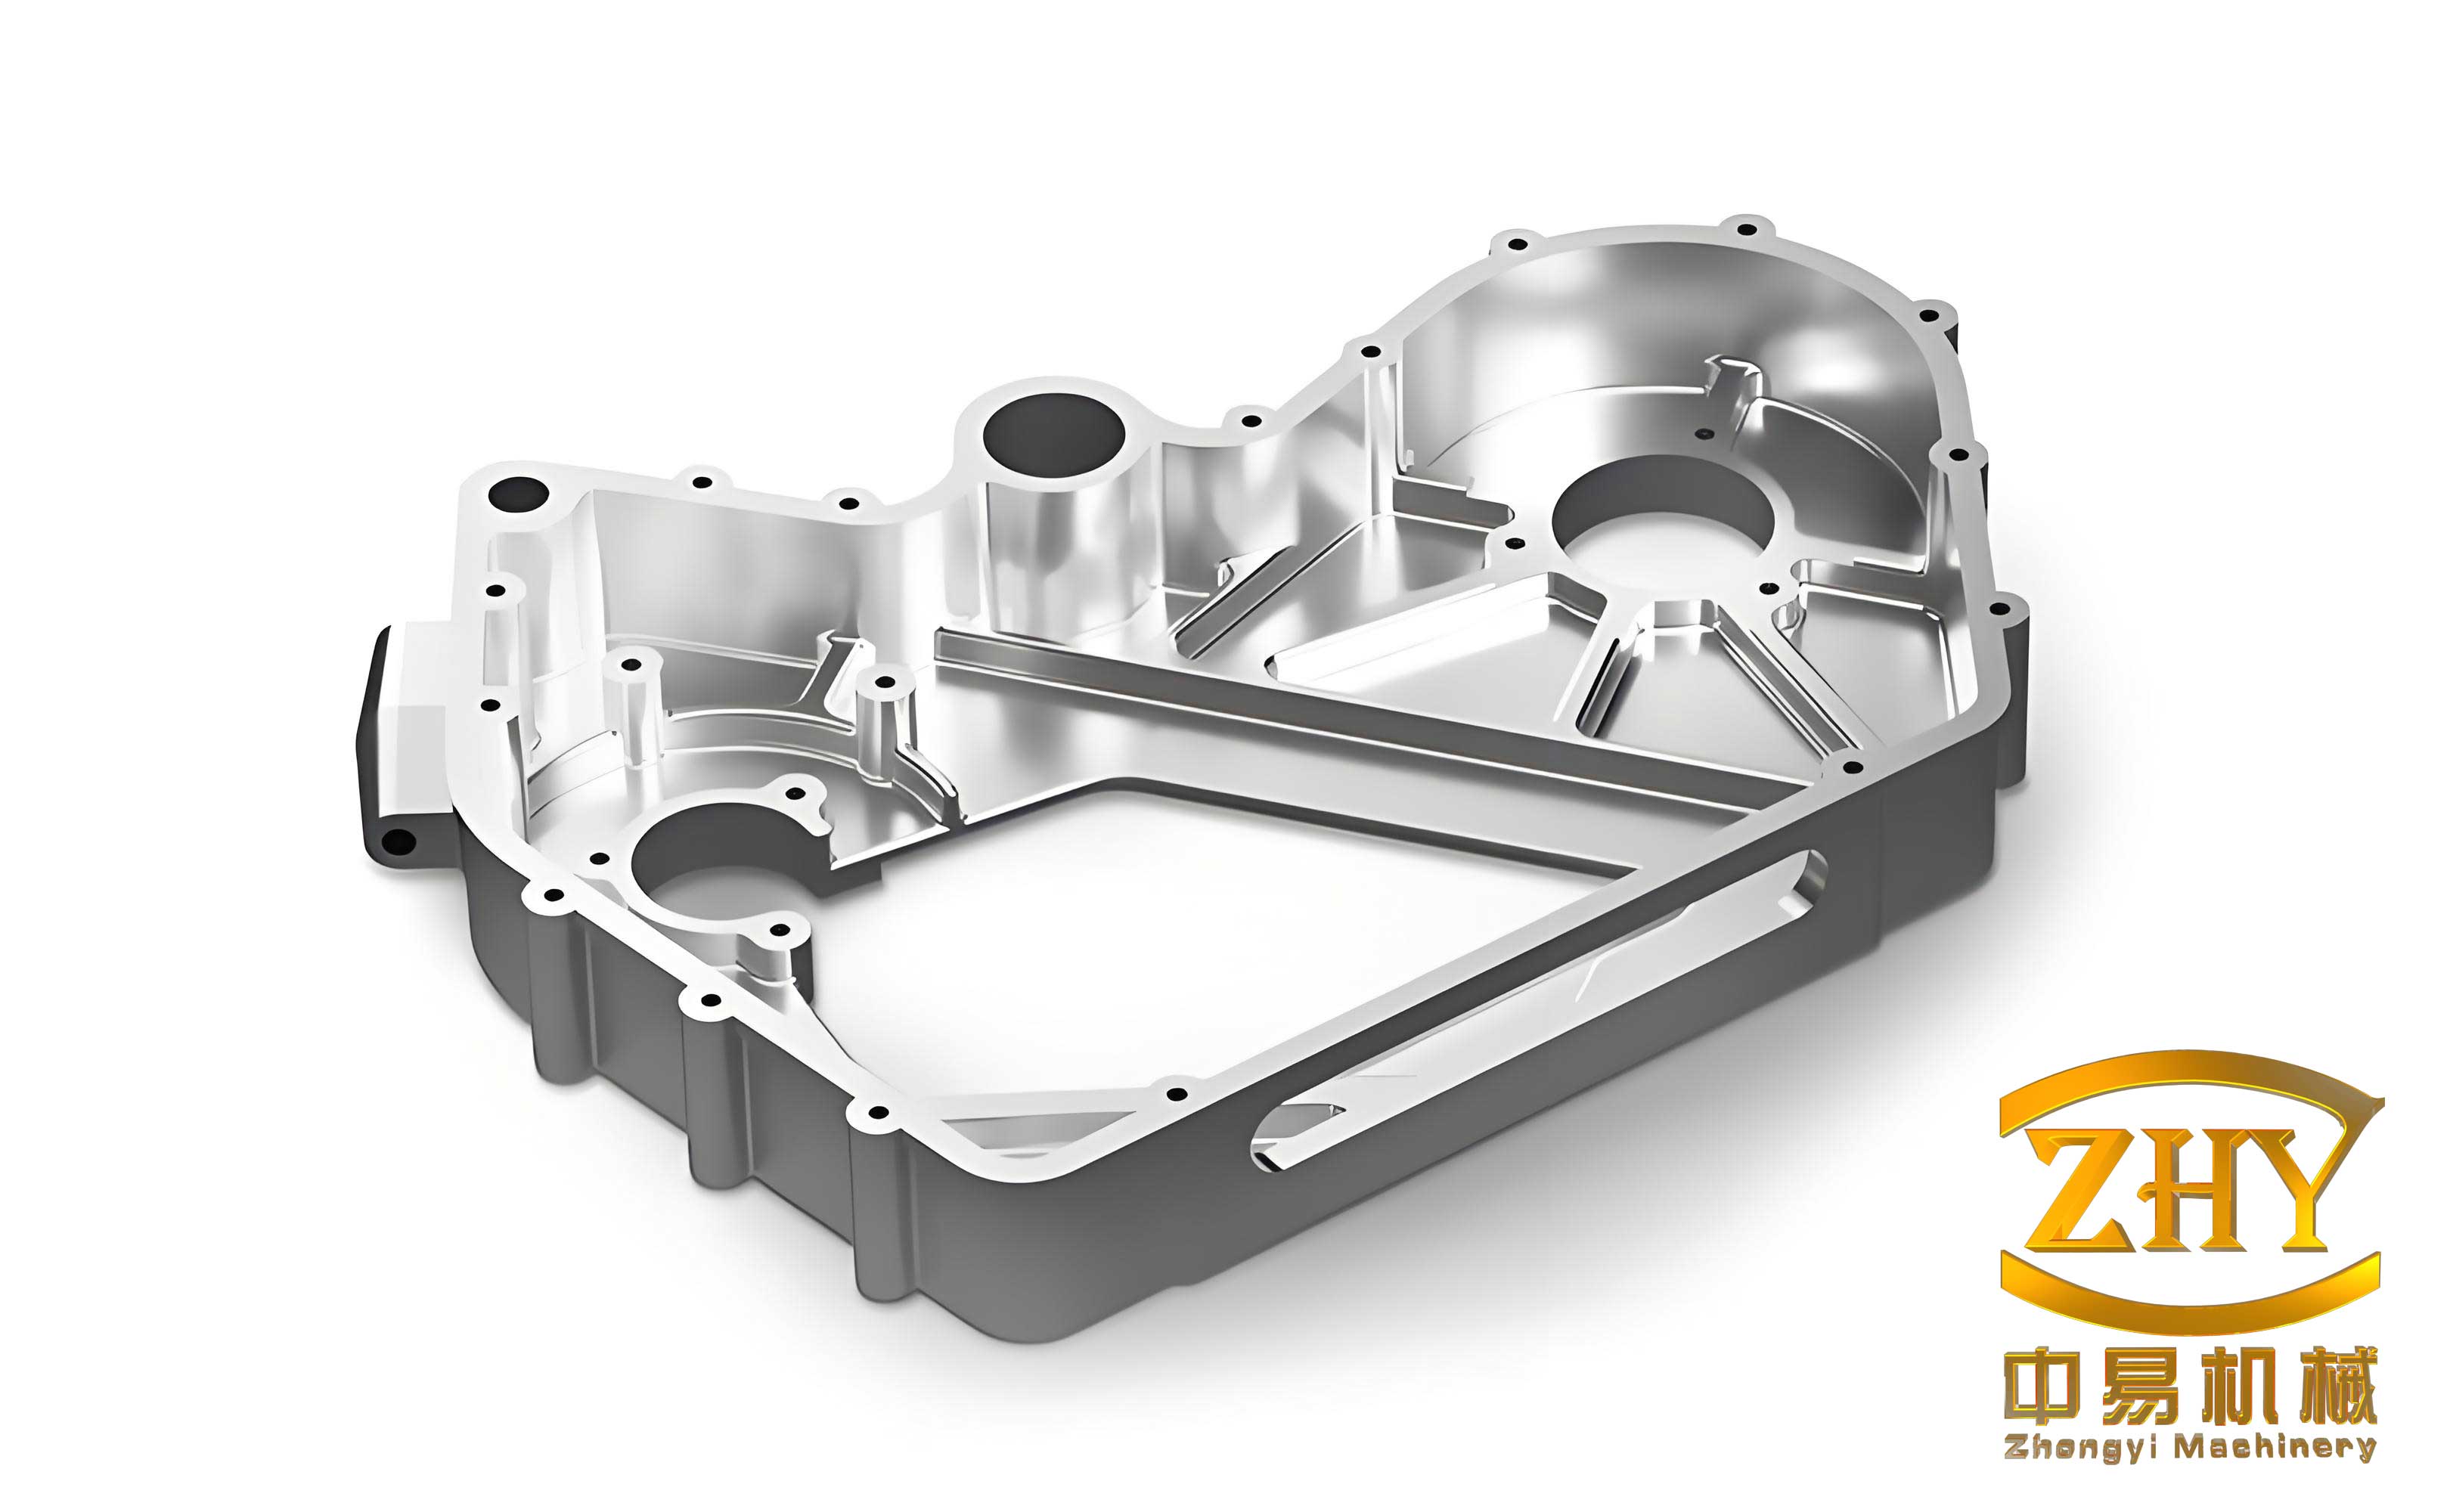
Initial production runs of these shell castings revealed several quality issues that compromised their performance. The most critical problem was failure in hydraulic pressure testing, with leakage points often clustering in specific areas of the housing, indicating micro-porosity or lack of densification. Additionally, visible defects such as slag inclusions and cold shuts were observed on the casting surfaces, as illustrated in defect superposition analyses. These defects not only affected the pressure integrity but also posed risks for machining and service life. The rejection rates were unacceptably high, prompting a comprehensive investigation into the root causes, which I traced to suboptimal gating system design, improper molding orientation, inadequate negative pressure, low pouring temperature, and inappropriate chemical composition.
To address these issues, I embarked on a multi-faceted optimization program using orthogonal experimental methods. The key factors studied included gating system design, molding orientation (burial scheme), negative pressure degree, carbon equivalent (CE), and pouring temperature. Each factor was systematically varied while monitoring the response in terms of hydraulic test pass rate and defect incidence. The goal was to establish a robust process window for producing high-quality shell castings consistently.
Gating System and Molding Orientation Optimization
The initial gating systems for these shell castings were based on conventional bottom and side gating with single sprue configurations. For the larger housing, a combined bottom and middle gating with a radial “star” pattern was used, featuring a 50 mm diameter sprue, four 30 mm × 20 mm runners, and eight 40 mm × 10 mm ingates. The area ratios (sprue:runner:ingate) were approximately 1:1.3:1.7. The molding orientation placed the non-pressure-bearing region downward. Similarly, for the other shell castings, single-side stepped gating systems were employed. However, these designs led to prolonged filling times and inadequate metal distribution, contributing to cold shuts and slag entrapment.
I redesigned the gating systems to promote rapid and uniform filling, essential for thin-wall shell castings. The new designs incorporated open gating principles with increased cross-sectional areas, multiple ingates, and stepped configurations to ensure simultaneous filling from bottom, middle, and top. For the larger housing, I implemented a double-sprue system with 70 mm diameter sprues, six 35 mm × 20 mm runners per pattern, and twelve 50 mm × 10 mm ingates, resulting in an area ratio of 1:1.1:1.5. The molding orientation was reversed to position the pressure-bearing region downward, which improved feeding and solidification patterns. For the medium housing, a double-sprue system with 70 mm sprues, five 40 mm × 20 mm runners, and seven 50 mm × 15 mm ingates (area ratio 1:1.2:1.4) was adopted, maintaining the non-pressure-bearing region downward. The small housing utilized a top-gating radial system with double sprues of 50 mm diameter, four 30 mm × 20 mm runners, and six 40 mm × 10 mm ingates (area ratio 1:1.3:1.3). These modifications significantly reduced filling times and improved metal flow dynamics for the shell castings.
The effectiveness of different gating system configurations was evaluated through experimental trials, with results summarized in Table 1. The optimized systems showed marked improvements in defect reduction, validating the importance of fast pouring and multi-point entry for thin-wall shell castings.
| Shell Casting Type | Sprue Diameter (mm) | Runner Dimensions (mm) | Ingate Dimensions (mm) | Number of Ingates | Area Ratio (Sprue:Runner:Ingate) | Filling Time (s) | Defect Rate Reduction (%) |
|---|---|---|---|---|---|---|---|
| Initial Design – Large | 50 | 30×20 | 40×10 | 8 | 1:1.3:1.7 | 50 | Baseline |
| Optimized Design – Large | 70 (double) | 35×20 | 50×10 | 12 | 1:1.1:1.5 | 35 | 45 |
| Initial Design – Medium | 50 | 30×20 | 30×15 | 6 | 1:1.3:1.4 | 58 | Baseline |
| Optimized Design – Medium | 70 (double) | 40×20 | 50×15 | 7 | 1:1.2:1.4 | 40 | 50 |
| Initial Design – Small | 50 | 30×20 | 30×10 | 8 | 1:1.3:1.3 | 40 | Baseline |
| Optimized Design – Small | 50 (double) | 30×20 | 40×10 | 6 | 1:1.3:1.3 | 30 | 40 |
The filling time for shell castings can be estimated using fluid flow principles. For an open gating system, the theoretical filling time \( t \) is related to the total ingate area \( A_i \), the head height \( h \), and the casting volume \( V \). A simplified model is:
$$ t = \frac{V}{A_i \cdot \sqrt{2gh}} $$
where \( g \) is acceleration due to gravity. Optimizing the ingate area reduces \( t \), which is critical for thin-wall shell castings to prevent premature freezing.
Negative Pressure Degree Optimization
In vacuum-assisted LFC, negative pressure plays a crucial role in maintaining mold stability, removing pyrolysis gases, and enhancing metal feeding. I investigated the impact of negative pressure degree on the quality of shell castings by varying it from 0.040 MPa to 0.052 MPa in increments of 0.001 MPa, while keeping other parameters constant (pouring temperature at 1470°C, initial gating design). For each setting, two boxes containing 16 shell castings were evaluated for hydraulic test pass rate and slag inclusion defects.
The results, plotted in Figure 1, show that as negative pressure increased, defect rates initially decreased, reaching an optimum at around 0.049 MPa. Beyond this point, further increases yielded diminishing returns. The relationship between negative pressure \( P \) and defect density \( D \) can be approximated by a quadratic function:
$$ D = aP^2 + bP + c $$
where \( a \), \( b \), and \( c \) are coefficients derived from experimental data. For these shell castings, the optimal negative pressure minimizes defects while avoiding excessive gas evolution or mold distortion.
| Negative Pressure (MPa) | Hydraulic Test Pass Rate (%) | Slag Inclusion Defect Rate (%) | Overall Defect Rate (%) |
|---|---|---|---|
| 0.040 | 65 | 15 | 35 |
| 0.043 | 70 | 12 | 30 |
| 0.046 | 78 | 10 | 22 |
| 0.049 | 85 | 5 | 15 |
| 0.052 | 83 | 6 | 17 |
The negative pressure enhances the permeability of the sand bed, which is vital for the escape of gases from the decomposition of the foam pattern during pouring of shell castings. The Darcy’s law can be applied to model gas flow:
$$ Q = \frac{kA \Delta P}{\mu L} $$
where \( Q \) is the gas flow rate, \( k \) is the permeability of the sand, \( A \) is the cross-sectional area, \( \Delta P \) is the pressure difference, \( \mu \) is the gas viscosity, and \( L \) is the flow path length. Optimizing \( \Delta P \) ensures efficient removal of gases without causing turbulence in the metal flow for shell castings.
Pouring Temperature Optimization
Pouring temperature is a critical parameter for thin-wall shell castings, as it affects fluidity, filling ability, and solidification behavior. Initially, based on experience with thicker castings, the pouring temperature was set at 1470°C. However, this led to cold shuts and incomplete filling in the thin sections of the shell castings. I systematically increased the pouring temperature from 1470°C to 1525°C in steps of 5°C, using the optimized gating system and a constant carbon equivalent of 3.8%. For each temperature, two boxes of shell castings were evaluated.
The data revealed a clear trend: as pouring temperature rose, defect rates dropped significantly. Cold shuts disappeared above 1500°C, and both leakage and slag inclusion rates reached minima at around 1520°C. The relationship between pouring temperature \( T \) and defect rate \( D \) can be described by an exponential decay function:
$$ D = D_0 e^{-k(T – T_0)} $$
where \( D_0 \) is the initial defect rate, \( k \) is a constant, and \( T_0 \) is a reference temperature. For these shell castings, a pouring temperature above 1510°C is essential to ensure proper fluidity and avoid premature solidification.
| Pouring Temperature (°C) | Cold Shut Defect Rate (%) | Hydraulic Test Pass Rate (%) | Slag Inclusion Defect Rate (%) |
|---|---|---|---|
| 1470 | 20 | 70 | 12 |
| 1480 | 15 | 75 | 10 |
| 1490 | 10 | 80 | 8 |
| 1500 | 5 | 85 | 6 |
| 1510 | 0 | 88 | 5 |
| 1520 | 0 | 90 | 4 |
| 1525 | 0 | 90 | 4 |
The superheat degree, defined as the difference between pouring temperature and liquidus temperature, is crucial for shell castings. The liquidus temperature \( T_L \) for gray iron can be estimated using the carbon equivalent:
$$ T_L = 1536 – 90 \cdot \text{CE} $$
where CE is in wt%. Maintaining sufficient superheat ensures adequate fluidity for filling thin sections in shell castings.
Carbon Equivalent Optimization
Carbon equivalent (CE) is a key factor influencing the microstructure and mechanical properties of gray iron shell castings. It affects graphitization, shrinkage tendency, and pressure tightness. I varied the CE from 3.6% to 4.3% in increments of 0.1%, while keeping pouring temperature at 1515–1525°C and using the optimized gating system. For each CE level, two boxes of shell castings were assessed.
The results indicated that increasing CE improved the hydraulic test pass rate and reduced slag inclusions, with optimal performance around CE = 4.1%. Beyond this, improvements plateaued. The CE is calculated as:
$$ \text{CE} = \%C + \frac{\%Si}{3} $$
For these shell castings, a CE of 4.1% (corresponding to 3.5% C and 1.8% Si) provided a balance between fluidity, graphitization, and strength, minimizing micro-porosity and enhancing pressure tightness.
| Carbon Equivalent (%) | Carbon Content (%) | Silicon Content (%) | Hydraulic Test Pass Rate (%) | Slag Inclusion Defect Rate (%) |
|---|---|---|---|---|
| 3.6 | 3.2 | 1.2 | 75 | 10 |
| 3.8 | 3.3 | 1.5 | 80 | 8 |
| 4.0 | 3.4 | 1.8 | 88 | 5 |
| 4.1 | 3.5 | 1.8 | 92 | 3 |
| 4.2 | 3.6 | 1.8 | 92 | 3 |
| 4.3 | 3.7 | 1.8 | 91 | 4 |
The relationship between CE and defect rate can be modeled using a polynomial fit. For these shell castings, the optimal CE maximizes graphitization, which reduces shrinkage and improves densification. The volume fraction of graphite \( V_g \) can be estimated as:
$$ V_g = k_1 \cdot \text{CE} – k_2 $$
where \( k_1 \) and \( k_2 \) are material constants. Higher \( V_g \) enhances pressure tightness in shell castings by accommodating solidification shrinkage.
Integrated Process Optimization
Based on the individual factor studies, I conducted final validation trials using the optimized parameters collectively. The process conditions for producing high-quality thin-wall shell castings are summarized as follows:
- Gating System: Open design with double sprues, stepped runners, and multiple ingates to ensure rapid filling. Area ratios tailored to each shell casting type.
- Molding Orientation: Pressure-bearing region oriented downward to improve feeding and solidification control.
- Negative Pressure: Maintained at 0.049 MPa during pouring and solidification to stabilize the mold and remove gases efficiently.
- Pouring Temperature: Set above 1510°C, ideally between 1515°C and 1525°C, to ensure fluidity and prevent cold shuts.
- Carbon Equivalent: Controlled at 4.1% (3.5% C, 1.8% Si) to promote graphitization and reduce shrinkage defects.
These optimized parameters were applied to batch production of the shell castings, resulting in significant quality improvements. The hydraulic test pass rate increased from an initial 65–70% to over 90%, and visible defects like slag inclusions and cold shuts were reduced to less than 5%. The consistency and reliability of the shell castings were enhanced, meeting the stringent requirements for pressure-tight applications.
The success of this optimization underscores the importance of a holistic approach in lost foam casting for thin-wall shell castings. Each parameter interacts with others, and fine-tuning them in concert is essential. For instance, higher pouring temperature requires adequate negative pressure to handle increased gas evolution, while proper CE ensures good fluidity without compromising mechanical properties. The gating system must be designed to leverage these conditions for optimal metal flow and solidification in shell castings.
Conclusion
Through systematic experimentation and analysis, I have established an optimized lost foam casting process for thin-wall gray iron shell castings, specifically transmission housings. Key findings include the necessity of a high pouring temperature above 1510°C, a carbon equivalent of 4.1%, a negative pressure of 0.049 MPa, along with a pressure-bearing-down molding orientation and an open, multi-ingate gating system with double sprues for rapid filling. These measures collectively ensure complete filling, dense microstructure, and excellent pressure tightness in the shell castings. The methodologies developed here can be extended to other thin-wall castings produced via lost foam casting, contributing to advancements in lightweight and high-integrity casting manufacturing.
The ongoing evolution of lost foam technology promises further improvements in shell castings production. Future work may explore advanced simulation tools to predict flow and solidification patterns, as well as the integration of real-time monitoring for process control. By continuing to refine these parameters, the quality and efficiency of shell castings can be enhanced, supporting the growing demand for reliable components in automotive and industrial sectors.