
Lost foam casting is recognized as a near-net-shape manufacturing technology with excellent dimensional accuracy, low surface roughness, reduced machining allowance, and simple operation. In recent years, the application of computer aided engineering (CAE) in casting process optimization has become increasingly widespread. In particular, numerical simulation of the filling and solidification stages can provide critical insight into defect formation mechanisms and enable the design of reliable gating systems. The present work focuses on a ductile iron casting of a long fork component, commonly used as a lifting arm in agricultural tractor hydraulic systems. This component was originally produced by conventional sand casting with significant defects. To overcome the problems, the lost foam casting process was adopted, and the gating system was optimized using ProCAST software. The study demonstrates that numerical simulation is a powerful tool for improving the quality of ductile iron casting.
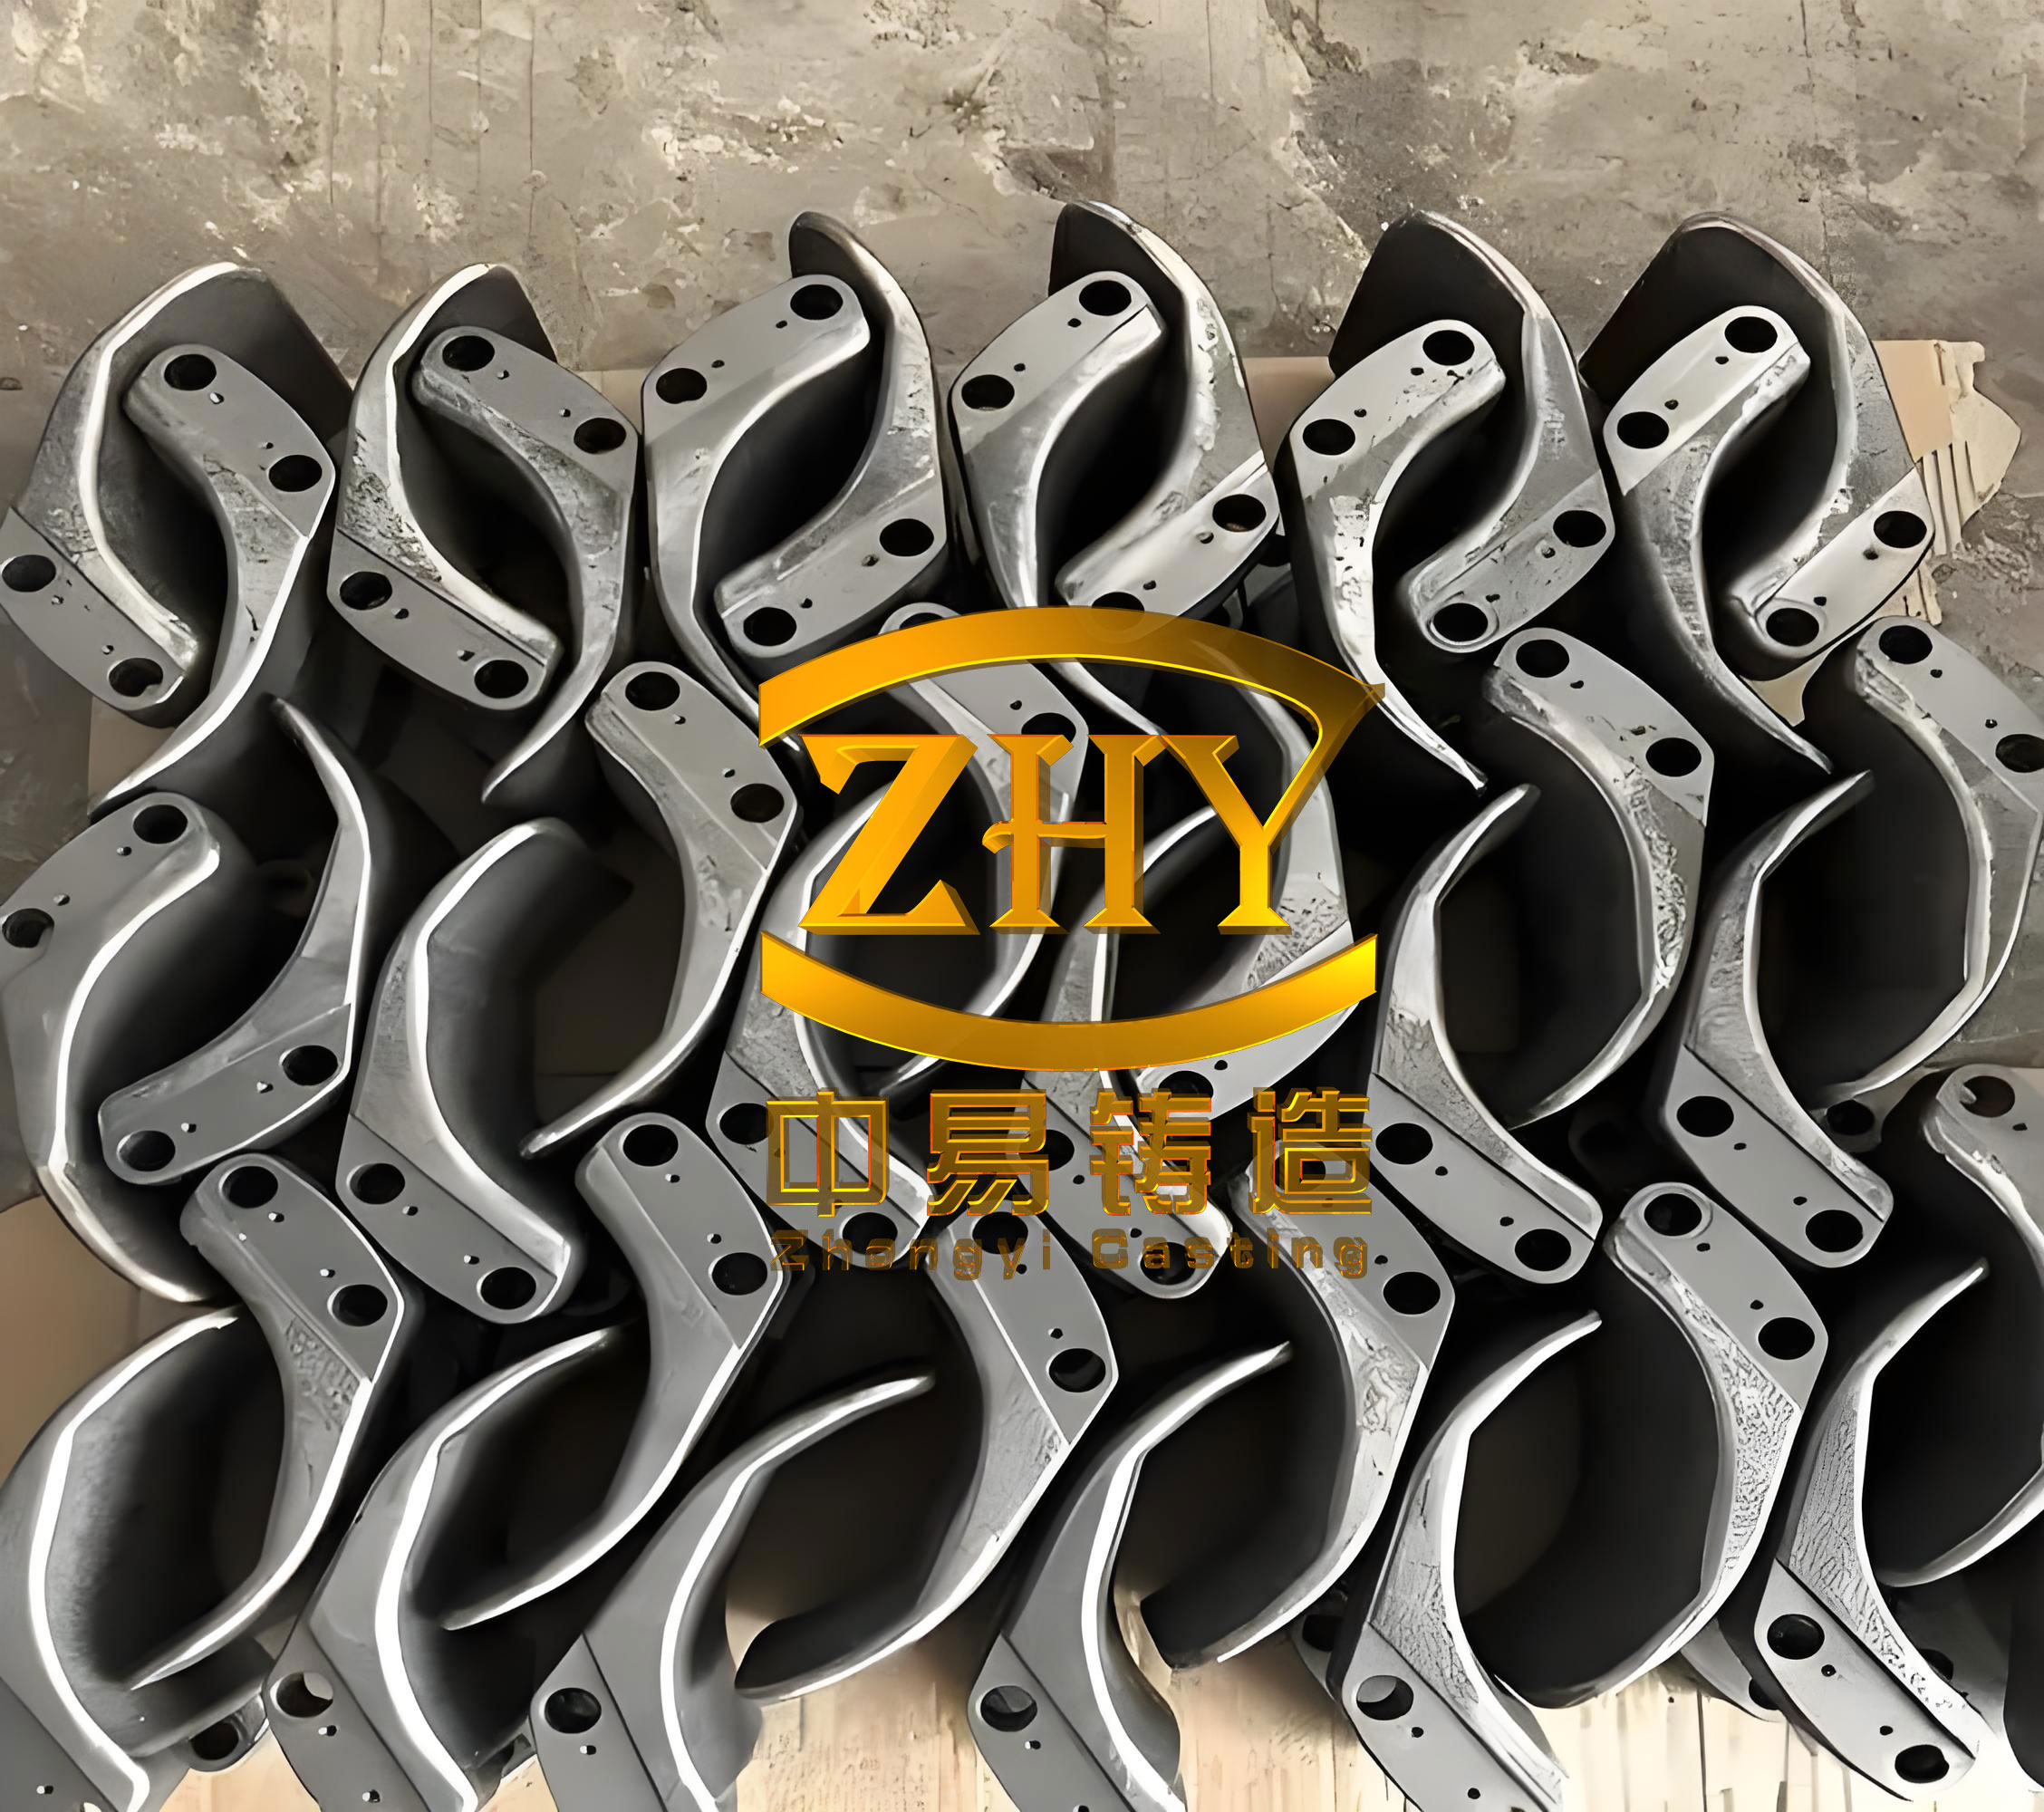
In this research, both bottom gating and top gating configurations were initially designed for the ductile iron casting. The filling and solidification processes of these two schemes were simulated, and severe shrinkage cavities and porosity were predicted in both cases. Based on the simulation results, an improved stepped gating system was proposed. The modified design was then simulated and verified by actual production trials. The results confirmed that the stepped gating system effectively eliminated the internal shrinkage defects. This paper presents a comprehensive investigation of the ductile iron casting process, including the thermal physical model, governing equations, simulation parameters, defect prediction, and practical validation.
Component Description and Material Properties
The ductile iron lift arm has a three-dimensional envelope size of 375 mm × 142 mm × 552 mm and a single-piece mass of approximately 30 kg. The material is QT600-3, which is a pearlitic ductile iron. The component has a complex geometry with multiple bosses, recesses, fillets, and holes. The cylindrical sleeve contains a stepped through-hole. The wall thickness varies significantly, resulting in dispersed hot spots. The middle section of the cylindrical sleeve has a relatively thin wall. The through-hole on the fork arm is machined in a later operation, so it is not cast in the raw blank. As a load-bearing component, strict requirements are imposed on internal soundness and surface quality. The ductile iron casting must be free from severe porosity, sand holes, slag inclusions, and wrinkled skin.
The chemical composition of the QT600-3 ductile iron is listed in Table 1. The magnesium content is controlled to promote spheroidization of graphite, and copper is added to strengthen the pearlite matrix.
| Element | C | Si | Mn | P | S | Cr | Ni | Cu | Mg | Fe |
|---|---|---|---|---|---|---|---|---|---|---|
| Content | 3.7 | 2.2 | 0.45 | 0.055 | 0.02 | 0.25 | 0.15 | 0.45 | 0.055 | Balance |
Thermal Physical Model and Governing Equations
The simulation of the ductile iron casting was carried out using ProCAST, a finite element based software for casting process simulation. The finite element mesh of the long fork casting used an element size of 4 mm for complex curved surfaces, 15 mm for the gating system and risers, and 100 mm for the sand mold. The interface between the hollow sprue and the foam pattern was defined as “EQUIV” while all other interfaces were set as “COINC”. The interface heat transfer coefficient was set to 150 W/(m²·K). The initial temperature of the sand mold and foam pattern was 25 °C, and the pouring temperature was 1480 °C.
The fluid flow and heat transfer in the lost foam casting process can be described by the continuity equation, the Navier-Stokes momentum equations, and the energy equation. The continuity equation is written as:
$$ \frac{\partial \rho}{\partial t} + \nabla \cdot (\rho \mathbf{u}) = 0 $$
The momentum equation for incompressible or weakly compressible liquid metal is:
$$ \rho \frac{\partial \mathbf{u}}{\partial t} + \rho (\mathbf{u} \cdot \nabla) \mathbf{u} = -\nabla p + \mu \nabla^2 \mathbf{u} + \rho \mathbf{g} $$
Here, \(\rho\) is the density of the liquid metal, \(\mathbf{u}\) is the velocity vector, \(p\) is the pressure, \(\mu\) is the dynamic viscosity, and \(\mathbf{g}\) is the gravitational acceleration. In lost foam casting, the decomposition of the foam pattern introduces a gas pressure that influences the flow behavior. The pressure boundary condition was set to 0.05 MPa under vacuum at the mold walls and 1.05 MPa at the sprue top, while the external surface of the flask was set to 1.0 MPa.
The energy conservation equation used for the temperature field calculation is:
$$ \rho c_p \frac{\partial T}{\partial t} + \rho c_p \mathbf{u} \cdot \nabla T = \nabla \cdot (k \nabla T) + \rho L \frac{\partial f_s}{\partial t} $$
In this equation, \(T\) is the temperature, \(c_p\) is the specific heat, \(k\) is the thermal conductivity, \(L\) is the latent heat of solidification, and \(f_s\) is the solid fraction. The term on the right-hand side accounts for latent heat release during solidification. For ductile iron casting, the solidification path is complicated by graphite precipitation and austenite formation. The graphite expansion produces self-feeding, which reduces shrinkage tendencies. To capture this effect, the solidification simulation was coupled with a micro-model. In ProCAST, the parameters \(POROS = 1\), \(GRAPHITE = 0.8\), and \(FADING = 0.8\) were set to model the graphite expansion behavior.
Because the coating layer on the foam pattern plays an important role in gas permeability and heat transfer, appropriate parameters were added in the data file to account for the coating effect. The filling simulation was performed using the gravity filling mode with coupled flow and temperature fields. The solidification simulation used the gravity thermal mode with the micro-model enabled.
Initial Gating System Designs
Bottom Gating System
The bottom gating system consisted of a hollow sprue and a horizontal runner. The hollow sprue had a diameter of 45 mm, and its top was 250 mm above the top of the casting to ensure sufficient metal static pressure. The runner was a solid foam plate with a length and width of 110 mm × 50 mm, and its height transitioned from 40 mm at the sprue side to 10 mm at the ingate. No feeding risers were used, relying on the self-feeding of ductile iron, except for a small slag collecting riser measuring 50 mm × 50 mm × 70 mm placed at the top fork arm. The simulation showed that the bottom gating system filled the mold smoothly without defects such as wrinkled skin, sand adhesion, or gas holes. However, during filling, the liquid metal could entrap foam decomposition products. The slag collecting riser at the top of the cylindrical sleeve helped to expel slag and gas. In the solidification stage, the ingate and sprue solidified too early, which prevented external feeding of the lower part of the casting. As a result, severe shrinkage porosity was predicted near the inner wall of the cylindrical sleeve close to the lower fork arm recess. The actual trial production confirmed this defect, as shown by the dense shrinkage cavities observed in the sectioned casting.
Top Gating System
In the top gating scheme, the sprue was connected to a central top riser, and ingates were arranged on both sides of the central riser to introduce metal into the two arm sections. Additional risers were placed at the upper and lower sides of the cylindrical sleeve and at the front end of the upper arm. The ingate cross-section was 40 mm × 40 mm, the central riser was 80 mm × 80 mm × 170 mm, the sprue diameter was 45 mm, and the height was 250 mm. The upper side riser was 60 mm × 60 mm × 90 mm, the lower side riser was 60 mm × 60 mm × 110 mm, and the front arm riser was 50 mm × 50 mm × 70 mm. The simulation indicated that the top gating system filled progressively from top to bottom, with smooth filling and no flow interruption. The last filled region was the front end of the lower fork arm, which is farthest from the ingate. However, the top gating system was not favorable for slag removal. The risers solidified earlier than the hot spot regions, so they could not provide sufficient liquid feeding. The central large riser kept the gating system molten longer, allowing external feeding to both upper and lower hot spots, but the upper blind riser had a high cooling rate and solidified prematurely, leading to severe shrinkage porosity in the upper hot spot. The trial production result was consistent with the simulation, showing a pronounced shrinkage cavity in that area.
Improved Stepped Gating System
The bottom gating system provided stable filling and easy slag removal but suffered from early solidification of the feeding path. The top gating system kept the ingates molten longer but caused premature solidification of the risers and adverse reverse feeding. To combine the advantages of both approaches, a stepped gating system was designed. The improved gating system consists of a hollow sprue, a vertically oriented solid foam runner acting as a central reservoir, and two levels of ingates connecting the runner to the thick sections of the casting. The pouring position was set at the upper and lower hot spots of the cylindrical sleeve. This arrangement intentionally changes the temperature field during solidification to achieve directional solidification. The final solidification zones remain connected to the gating system, enabling continuous feeding. Small slag collecting risers were placed at the top of the cylindrical sleeve and at the front of the upper fork arm, with dimensions of 30 mm × 50 mm × 20 mm. The hollow sprue had a diameter of 45 mm and a height of 250 mm. The solid foam runner was 60 mm × 60 mm × 240 mm. The ingates had a cross-section of 40 mm × 30 mm with a variable cross-section to prevent reverse feeding.
The stepped gating system significantly reduces the flow distance of the liquid metal because the metal enters from two levels. The filling time was reduced from 24.08 s in the bottom gating system to 16.64 s. This shorter filling time helps to maintain a higher metal temperature during filling, which improves the decomposition of the foam pattern. The final filling regions were the two arm tips. The solidification simulation showed that the improved gating system almost completely eliminated severe shrinkage defects. Only small isolated liquid regions remained in the thick-walled areas at both ends of the cylindrical sleeve, which could cause minor dispersed microporosity. The severe shrinkage cavity was predicted to appear only in the vertical runner adjacent to the ingate, not in the casting itself.
Table 2 summarizes the predicted defect characteristics for the three gating systems.
| Gating System | Filling Time (s) | Predicted Defects in Casting | Validation |
|---|---|---|---|
| Bottom gating | 24.08 | Severe shrinkage porosity in lower sleeve wall | Confirmed by trial |
| Top gating | — | Severe shrinkage porosity in upper hot spot | Confirmed by trial |
| Stepped gating | 16.64 | Only minor microporosity, no severe shrinkage | Confirmed by production |
In the stepped gating system, the connection between the casting and the gating system was maintained during almost the entire solidification process. The vertical runner served as a large feeder, supplying liquid metal to the hot spots through the ingates. The small slag risers solidified within 10 s after filling, which prevented them from drawing metal back from the casting. This behavior is essential for avoiding secondary shrinkage.
Numerical Simulation Settings and Boundary Conditions
To reproduce the experimental conditions as accurately as possible, the following simulation settings were applied. The heat transfer coefficient at the mold-metal interface was set to 150 W/(m²·K). The vacuum pressure during filling was set to 0.05 MPa. The pouring temperature was 1480 °C. The coating permeability was indirectly treated by adjusting the pressure boundary conditions. Table 3 lists the key parameters used in the simulation.
| Parameter | Value |
|---|---|
| Pouring temperature | 1480 °C |
| Initial sand mold temperature | 25 °C |
| Interface heat transfer coefficient | 150 W/(m²·K) |
| Vacuum pressure | 0.05 MPa |
| Pressure at sprue top | 1.05 MPa |
| Pressure at flask external surface | 1.0 MPa |
| Surface mesh size (complex parts) | 4 mm |
| Gating/riser mesh size | 15 mm |
| Sand mold mesh size | 100 mm |
For the micro-model coupling, the porosity model was activated with \(POROS=1\). The graphite expansion model used \(GRAPHITE=0.8\) and \(FADING=0.8\). These values were chosen based on previous studies of ductile iron casting. The Niyama criterion is often used to predict microporosity in castings. The local thermal gradient \(G\) and cooling rate \(R\) are combined in the Niyama criterion as:
$$ \text{Niyama} = \frac{G}{\sqrt{R}} $$
Lower Niyama values indicate higher susceptibility to shrinkage porosity. In this study, the simulation results were evaluated by directly inspecting the porosity contours and the solidification time fields. The predicted shrinkage locations agreed well with the trial production cuts.
Filling and Solidification Analysis
Filling Behavior of the Stepped Gating System
For the final stepped gating design, the filling simulation showed that the liquid metal entered the mold through both upper and lower ingates. At 3.3 s, the metal had filled the sprue and runner. At 5.6 s, the metal began to enter the cavity from both ingates, and the two flow fronts merged without entrapment of foam residues. At 7.5 s, the lower arm and the cylindrical sleeve were being filled. At 11.0 s, the metal reached the front ends of the fork arms. The total filling time was 16.64 s. The filling process was stable and continuous, with no visible cold shuts or misruns. The temperature of the liquid metal at the end of filling was sufficiently high to ensure complete fusion.
Solidification and Shrinkage Prediction
The solidification sequence of the improved ductile iron casting was simulated using the coupled thermal-micro model. The results showed that the liquid metal in the ingates remained molten until the hot spots in the casting had solidified. The vertical runner acted as a central feeder and maintained a continuous liquid channel to the casting. The small slag risers solidified early, as designed, avoiding any reverse feeding. The temperature distribution at the final stage of solidification indicated that the thick sections near the cylindrical sleeve ends were the last to solidify. However, because these regions remained connected to the ingate, the liquid shrinkage could be compensated by the metal from the runner. The shrinkage porosity criterion predicted only negligible microporosity in the casting body. The severe shrinkage cavity observed in the bottom and top gating systems was completely absent in the stepped gating scheme.
The practical production with the improved stepped gating system produced a sound ductile iron casting. The sectioned specimen revealed no significant shrinkage holes, and only a small amount of dispersed microporosity was found in the lower hot spot. This result was consistent with the simulation, confirming the reliability of the ProCAST model for lost foam ductile iron casting.
Conclusion
The numerical simulation of ductile iron casting using ProCAST was successfully applied to optimize the gating system for a long fork lifting arm. The bottom gating and top gating systems were both found to produce severe shrinkage defects due to early freezing of feeding channels or premature riser solidification. The proposed stepped gating system, which combines the benefits of bottom and top feeding, enabled directional solidification and continuous feeding throughout the solidification process. The simulation predicted that the stepped gating system effectively eliminates shrinkage cavities and reduces porosity to an acceptable level. Actual production trials validated the simulation results, demonstrating that the stepped gating system is a feasible solution for producing high-quality ductile iron casting of this type. This study illustrates that CAE-based numerical simulation is an essential tool for the design and optimization of lost foam casting processes for ductile iron components.