
In my years of experience as a casting engineer specializing in advanced foundry processes, I have consistently witnessed the transformative potential of lost foam casting. This innovative technique, often referred to as evaporative pattern casting, has revolutionized the production of complex and large-scale components, particularly in industries demanding high precision and material efficiency. The core principle of lost foam casting involves using a foam pattern—typically made from expandable polystyrene (EPS)—that is embedded in unbonded sand. When molten metal is poured, the foam vaporizes, leaving behind a precise cavity that forms the final casting. My firsthand involvement in numerous projects, including the production of large sinter machine pallets, has solidified my conviction that lost foam casting offers unparalleled advantages in terms of dimensional accuracy, cost reduction, and environmental sustainability. Throughout this article, I will delve deep into the technical intricacies, share practical insights, and underscore why lost foam casting is a cornerstone of modern manufacturing.
The journey of mastering lost foam casting begins with a thorough understanding of its fundamental mechanics. At its heart, the process relies on the controlled degradation of the foam pattern upon contact with molten metal. The pattern, coated with a refractory material, is placed in a flask filled with dry, unbonded sand. As the metal fills the mold, the foam undergoes pyrolysis—a thermal decomposition process that produces gases. These gases must be efficiently vented through the permeable coating and sand to prevent defects. The success of lost foam casting hinges on a delicate balance between pattern density, coating properties, sand compaction, and pouring parameters. I have often emphasized to my teams that optimizing these variables is key to achieving defect-free castings with excellent surface finish and mechanical properties. The following sections will break down each stage, supported by empirical data, formulas, and comparative analyses.
One of the most critical initial steps in lost foam casting is determining the optimal pouring position for the pattern. This decision directly impacts metal flow, solidification dynamics, and final part quality. Based on my practice, I always analyze the component’s geometry, wall thickness variations, and functional requirements. For instance, in producing a large frame-like structure such as a sinter machine pallet—with dimensions around 4180 mm in length, 1500 mm in width, and 460 mm in height—I typically invert the operational orientation by 180 degrees for pouring. This positioning ensures that major planar surfaces rest directly on a leveled sand bed, enhancing stability and minimizing distortion during filling. Moreover, it facilitates easier sand filling in intricate areas like shaft holes and undercuts. The gating system is designed to enable rapid and uniform filling; I often employ top-gating with multiple in-gates along the main beams to promote sequential displacement of foam degradation products upward into vent or riser areas. To quantify this, I use shrinkage allowances specific to the alloy and geometry. For ductile iron castings like QT500-7, I apply differential shrinkage rates: approximately 1.1% in the length direction and 0.9% in the width direction, calculated as:
$$ \text{Final Dimension} = \text{Pattern Dimension} \times (1 + \text{Shrinkage Rate}) $$
Machining allowances are also assigned strategically; for the pallet, I allocate 13 mm on the upper surfaces, 8 mm on bore holes, and 7 mm on sides and bottom surfaces, ensuring that any superficial slag or carbon residues can be removed post-casting. The table below summarizes key pattern design parameters I adhere to for large ductile iron components via lost foam casting:
| Parameter | Typical Value/Range | Remarks |
|---|---|---|
| Pattern Material Density | 18–22 g/L (EPS) | Balances strength and gas evolution |
| Shrinkage Allowance (Length) | 1.1% | For ductile iron (QT500-7) |
| Shrinkage Allowance (Width) | 0.9% | For ductile iron (QT500-7) |
| Machining Allowance (Top) | 13 mm | To remove potential surface defects |
| Machining Allowance (Bore) | 8 mm | For precision finishing |
| Gating System Type | Top-poured, multiple in-gates | Ensures fast filling and gas evacuation |
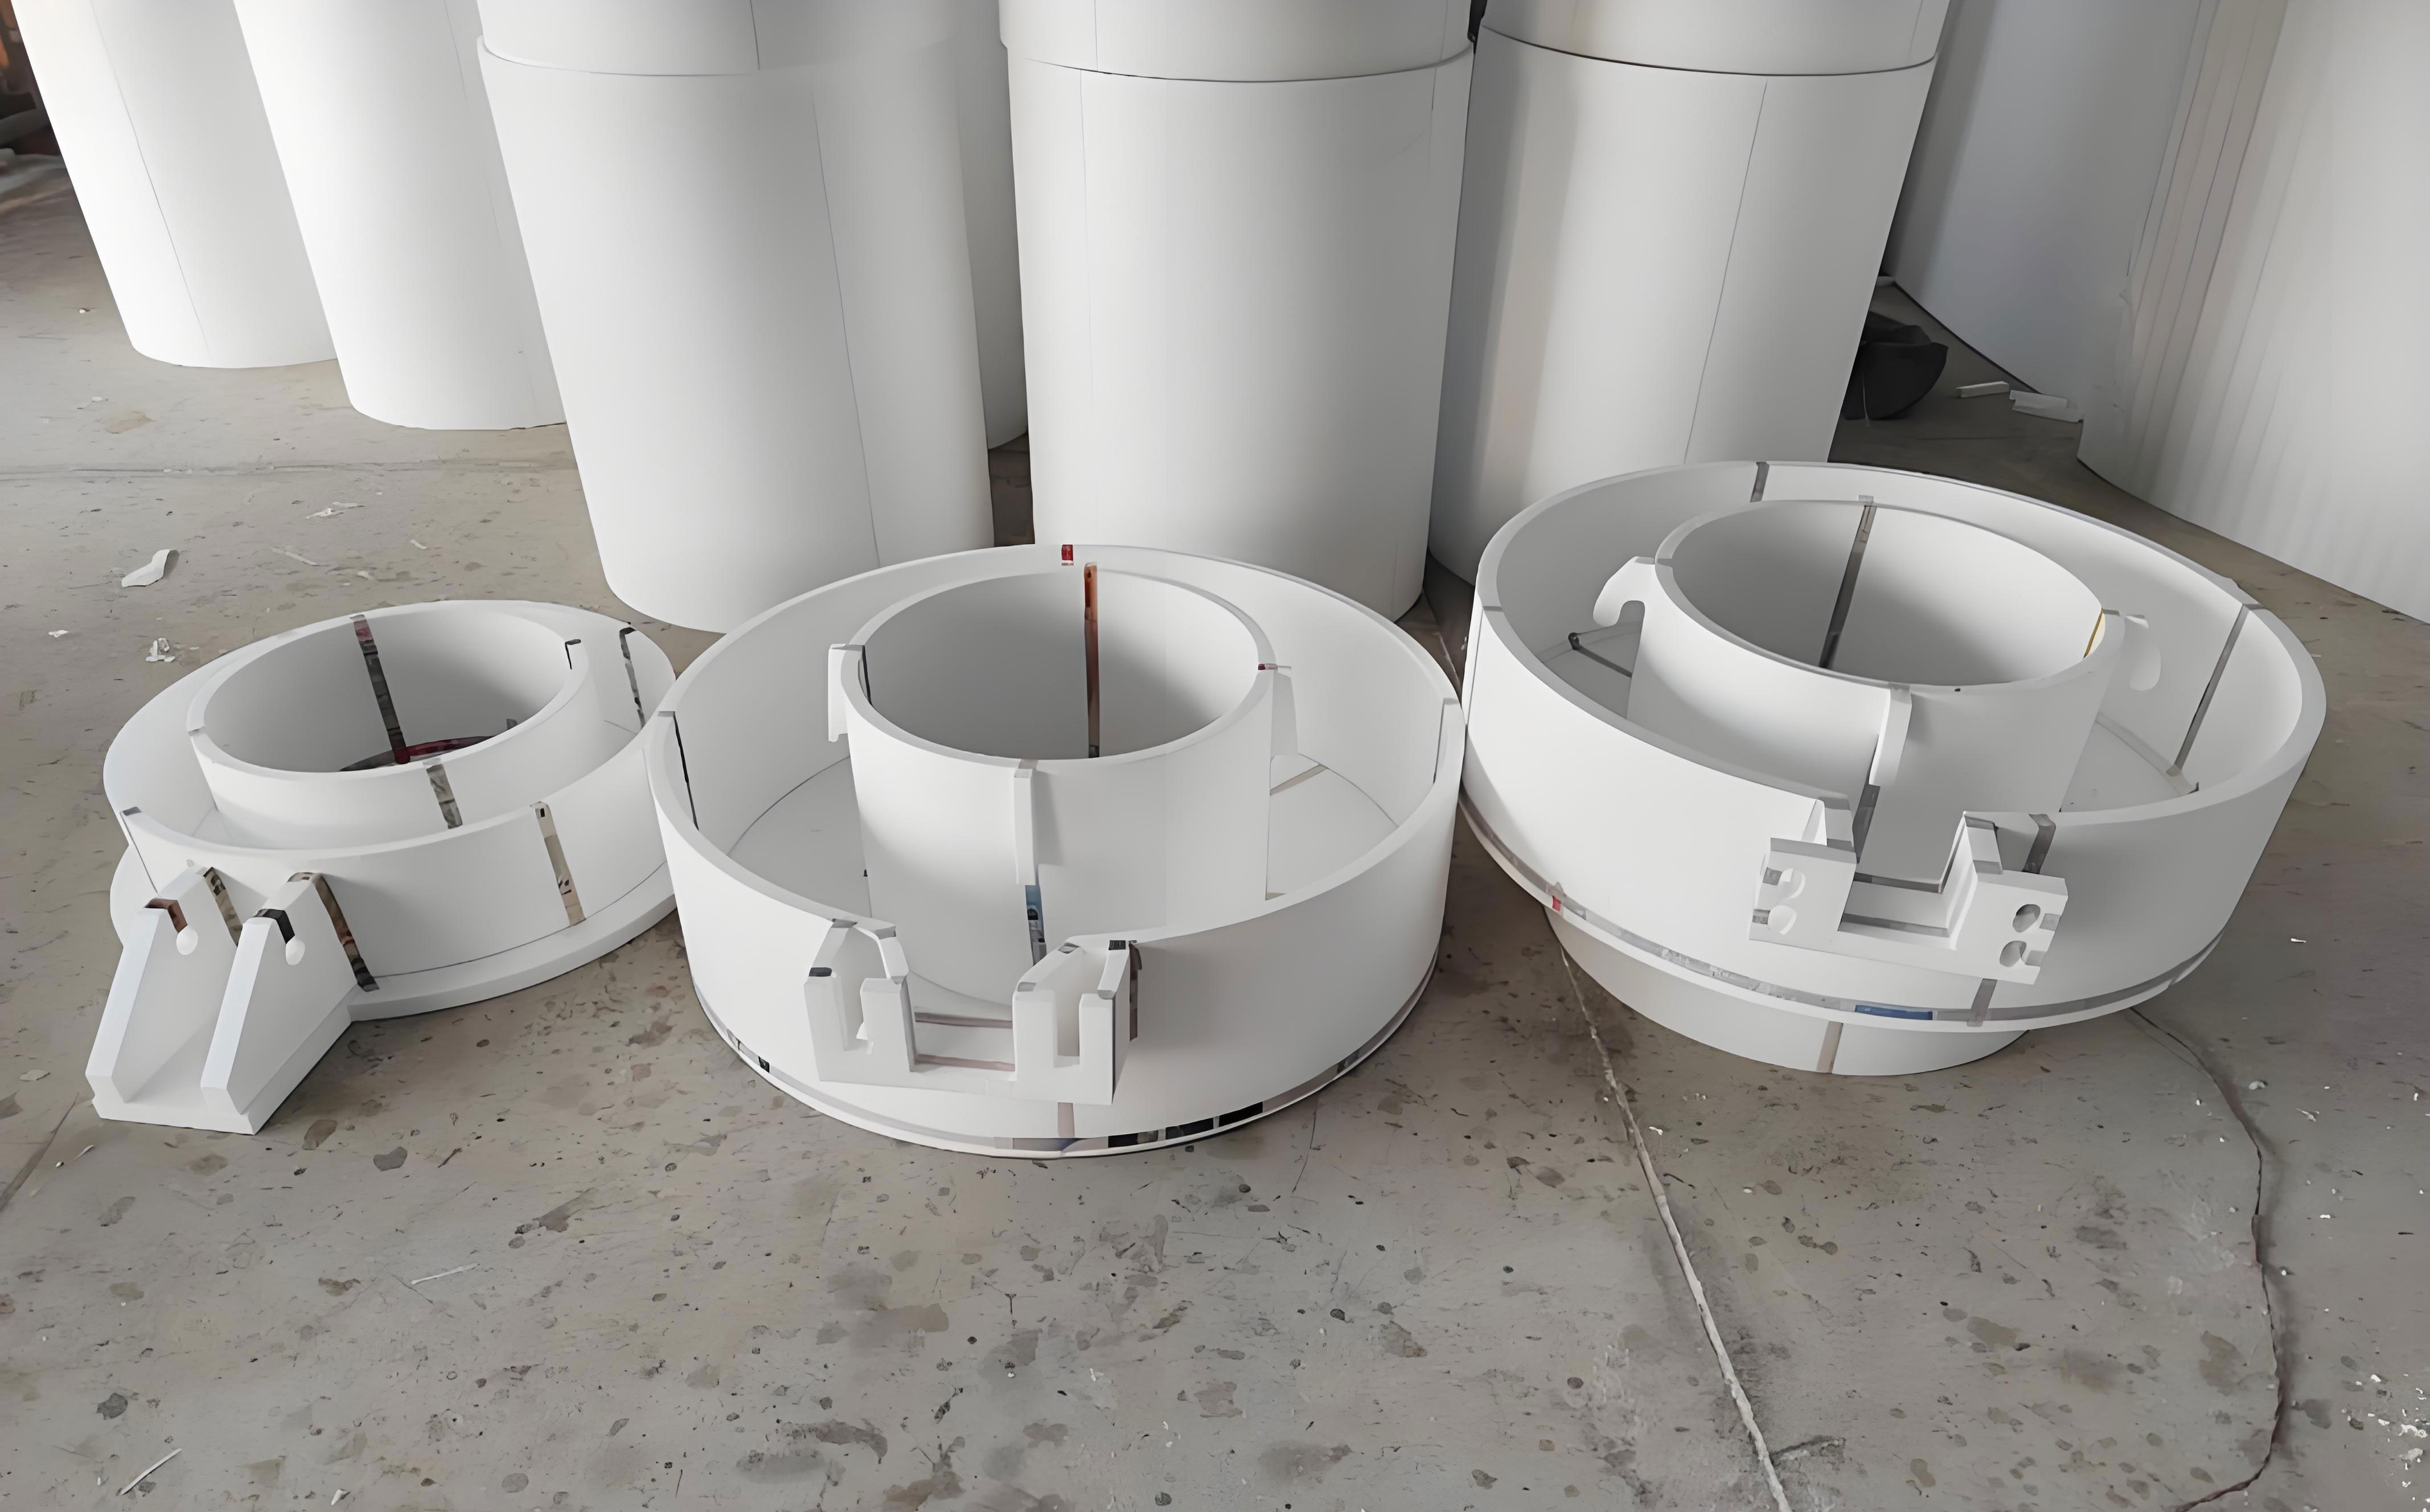
Fabricating the foam pattern is a meticulous art that I have refined over time. For large castings, I prefer using EPS boards with a density of 18–22 g/L and a bead size of 4–5 mm, as they offer a good compromise between detail resolution and structural integrity during handling. The pattern is often segmented for ease of manufacture; for example, the pallet is divided into three sections: two end blocks and a central beam framework. I utilize dedicated profiling hot-wire cutting machines to shape the beam profiles from EPS boards, ensuring dimensional consistency. Assembly is performed on precision jigs and fixtures to maintain straightness and parallelism, with cold-cure adhesives providing strong bonds without causing pattern distortion. It is crucial to verify all critical dimensions, such as shaft hole locations, before proceeding. The integrity of the foam pattern directly influences the final casting’s accuracy, so I implement rigorous inspection protocols at this stage. The use of lost foam casting here eliminates the need for complex core assembly and mold parting lines, streamlining the entire process.
Coating application is arguably the most vital aspect of lost foam casting, acting as the barrier between the degrading foam and the invading metal. In my work, I formulate two distinct coating layers to address different needs. The primary or face coat, about 0.5 mm thick, is designed for high refractoriness and surface finish. It typically consists of 50–55% amorphous graphite and 30–35% flake graphite, suspended with 3% white latex and 1% carboxymethyl cellulose (CMC) in water. This composition ensures good thermal resistance and minimizes metal penetration. The secondary or backup coat, applied in two layers to a total thickness of around 4 mm, focuses on permeability and strength. I use 100% silica flour (70–200 mesh) with 3% white latex, 2% CMC, and 4% sodium bentonite as a binder. The coating viscosity is adjusted to achieve a uniform slurry that penetrates pattern details without bridging. I often immerse the pattern using a dipping machine with rotational capabilities to ensure complete coverage, followed by brushing or flowing for touch-ups. Drying is conducted in a controlled oven to prevent cracking or warping; the coating must be thoroughly dry to withstand sand compaction and metal pouring. The coating thickness \( t_c \) can be related to the pattern surface area \( A \) and slurry properties via an empirical relation:
$$ t_c = k \cdot \left( \frac{\eta \cdot V}{A} \right)^{0.5} $$
where \( \eta \) is the slurry viscosity, \( V \) is the volume applied, and \( k \) is a material constant. Proper coating is essential for achieving the desired surface quality and preventing defects like veining or burn-on, which I have mitigated through iterative formulation testing.
Molding in lost foam casting involves embedding the coated pattern in dry, unbonded sand and compacting it uniformly. I select rounded-grain silica sand with a size distribution of 20–70 mesh for its excellent flowability and permeability. The sand is free of binders, which simplifies reclamation and reduces environmental impact—a hallmark advantage of lost foam casting. The pattern is placed on a pre-leveled sand bed in a flask, and sand is added gradually using a rain-style filler to avoid pattern displacement. For complex geometries like the pallet’s shaft holes and under-beam areas, I pre-fill sand manually to ensure complete packing. Compaction is achieved via a three-dimensional vibration table with an excitation force exceeding twice the total mass of the flask-sand-pattern system. I control the amplitude to about 1 mm and vibration time to roughly 1 minute per layer to achieve optimal density without pattern deformation. The sand’s compaction density \( \rho_s \) influences mold stability and can be expressed as:
$$ \rho_s = \rho_0 \cdot (1 + \epsilon_v) $$
where \( \rho_0 \) is the loose sand density and \( \epsilon_v \) is the volumetric strain induced by vibration. Maintaining a consistent and adequate vacuum throughout pouring is critical; I employ a system with dual vacuum pumps and稳压 tanks to sustain a negative pressure of -0.06 to -0.07 MPa initially, tapering to no less than -0.03 MPa at the end of pouring. This vacuum assists in removing pyrolysis gases and preventing mold collapse, which is especially important for large-scale lost foam casting operations.
Melting and pouring constitute the final act where theory meets practice. For ductile iron castings like the sinter pallet, I use medium-frequency induction furnaces with a melting capacity of 3 tons per hour. Charge materials include high-purity pig iron and selected returns, aiming for a low sulfur and phosphorus content to meet QT500-7 specifications. The target chemical composition, which I meticulously control, is summarized below:
| Element | Target Range (wt%) | Importance in Ductile Iron |
|---|---|---|
| Carbon (C) | 3.3–3.7 | Promotes graphitization, affects fluidity |
| Silicon (Si) | 2.4–2.7 | Strengthens ferrite, influences eutectic temperature |
| Manganese (Mn) | 0.25–0.40 | Enhances hardenability, neutralizes sulfur |
| Phosphorus (P) | <0.06 | Minimized to prevent embrittlement |
| Sulfur (S) | <0.02 | Low level crucial for effective nodulization |
| Residual Magnesium (Mg) | ~0.038 | Ensures spheroidal graphite formation |
| Residual Cerium (Ce) | ~0.02 | Suppresses deleterious carbide formation |
Inoculation and nodularization are performed in the ladle: I add 1.2–1.6% of a rare-earth-bearing magnesium alloy (e.g., ReMg7-8) via the sandwich method, followed by two-stage inoculation with ferrosilicon (75% Si). The melt temperature is maintained at 1430–1460°C during tapping, with a pouring temperature of 1360–1380°C to balance fluidity and reduced gas generation. Pouring is executed swiftly—within 60 seconds for a 3.2-ton casting—using a pressurized gating system that ensures rapid and progressive replacement of the foam. The relationship between pouring time \( t_p \), metal head height \( h \), and gating cross-sectional area \( A_g \) can be approximated by:
$$ t_p = \frac{V_m}{\mu \cdot A_g \cdot \sqrt{2 g h}} $$
where \( V_m \) is the metal volume, \( \mu \) is the discharge coefficient, and \( g \) is gravitational acceleration. A pouring cup made from sodium silicate-bonded sand is placed atop the foam sprue to maintain a molten metal seal and prevent air ingress. The synergy of these parameters results in castings with high integrity, minimal shrinkage porosity, and consistent nodular graphite formation exceeding 85% spheroidization—a testament to the efficacy of lost foam casting.
The advantages of lost foam casting are multifold and deeply resonate with my operational philosophy. Firstly, it drastically simplifies pattern and mold making by eliminating cores, parting lines, and draft angles. This reduction in process steps translates to shorter lead times and lower labor costs. Secondly, the precision afforded by the foam pattern yields near-net-shape components, reducing machining allowances and material waste. For instance, the pallet’s weight reduction through optimized design can be quantified using the specific yield \( Y \):
$$ Y = \frac{W_c}{W_m} \times 100\% $$
where \( W_c \) is the casting weight and \( W_m \) is the molten metal weight; in lost foam casting, \( Y \) often exceeds 85%, compared to 70–75% in conventional green sand casting. Thirdly, the dry sand system is fully recyclable, minimizing disposal issues and fostering a greener foundry environment. However, challenges exist, such as controlling foam decomposition products to avoid carbon defects and ensuring pattern rigidity during sand filling. Through iterative process refinement, I have mitigated these by optimizing coating permeability and vacuum levels. The table below contrasts lost foam casting with traditional green sand casting for large ductile iron parts:
| Aspect | Lost Foam Casting | Traditional Green Sand Casting |
|---|---|---|
| Pattern Complexity | High; intricate geometries possible | Limited by core-making and draft |
| Dimensional Accuracy | ±0.3% of dimension | ±0.5–0.7% of dimension |
| Surface Finish (Ra) | 6.3–12.5 μm | 12.5–25 μm |
| Material Utilization | 85–90% | 70–80% |
| Sand Disposal | Negligible (dry, reusable sand) | Significant (clay-bonded sand) |
| Typical Lead Time | 30–40% shorter | Longer due to core/mold making |
My extensive engagement with lost foam casting has also revealed its versatility across alloys. While ductile iron is a common candidate, the process is equally adept for aluminum and steel components. The key lies in tailoring the foam density, coating composition, and pouring parameters to the alloy’s thermal characteristics. For aluminum, I use lower-density EPS (16–18 g/L) and coatings rich in zirconia to withstand higher thermal shock. The pyrolysis gas volume \( V_g \) generated during pouring can be estimated using the ideal gas law and foam properties:
$$ V_g = \frac{m_f \cdot R \cdot T}{M_f \cdot P} $$
where \( m_f \) is the foam mass, \( R \) is the gas constant, \( T \) is the decomposition temperature, \( M_f \) is the average molar mass of decomposition products, and \( P \) is the pressure. Controlling \( V_g \) via pattern design is crucial to avoid turbulence or gas entrapment.
Looking ahead, the future of lost foam casting is bright, driven by advancements in pattern materials (e.g., polymethylmethacrylate for reduced carbon residue), automated coating systems, and real-time process monitoring. I am actively exploring the integration of simulation software to predict metal flow and solidification, further minimizing trial runs. The economic and environmental benefits of lost foam casting make it a sustainable choice for the foundry industry. In conclusion, my hands-on experience confirms that lost foam casting is not merely a manufacturing process but a strategic enabler for producing high-quality, complex castings efficiently. By embracing its principles and continuously innovating, foundries can achieve significant competitive edge. The journey of perfecting lost foam casting is ongoing, and I am committed to pushing its boundaries for years to come.