
I have focused on the mass production of HT300 gray cast iron machine tool castings through lost foam casting because this near-net-shape process is widely used in automotive and machinery industries, yet it still suffers from high scrap rates and quality fluctuations. In my experience, the main difficulties are carburization, burn-on, gas porosity, cold shut, shrinkage, distortion, and surface roughness. The machine tool sector requires castings that account for more than 80% of total machine weight, and HT300 is a common material because of its high strength and wear resistance, but its strong chilling tendency and poor castability make it sensitive to process variation. I therefore developed a systematic material-process-defect cooperative control method for lost foam casting mass production. The integrated strategy includes low-carbon STMMA copolymer foam, optimized coating with graphite or carbon fiber, dynamic negative pressure control, bottom-gated open gating systems, and instantaneous FeSi75 inoculation. The result on a 20,000 t/y production line was a reduction of scrap from 12% to below 2%, a burn-on area below 1%, a carburized layer below 0.2 mm, and a surface roughness of Ra ≤ 25 µm.
Lost foam casting has significant advantages for machine tool castings: no pattern extraction, no parting line, and no sand core. It improves dimensional accuracy and surface quality, permits flexible design, and enables complex structures. In mass production, lost foam casting can be automated and intelligent, giving high efficiency and low cost with stable quality and low rejection. My research on the process control of HT300 machine tool castings by lost foam casting is therefore important for machine tool manufacturing. Overseas research started early and achieved notable results in the United States, Germany, and Japan, where optimized processes improved HT300 machine tool castings. Domestic research began in the 1980s and has progressed, but gaps remain in fundamental research, equipment development, and process stability. Few deep studies exist on the application of lost foam casting. I have therefore addressed these gaps with deeper research into the process control of HT300 machine tool castings in lost foam casting mass production.
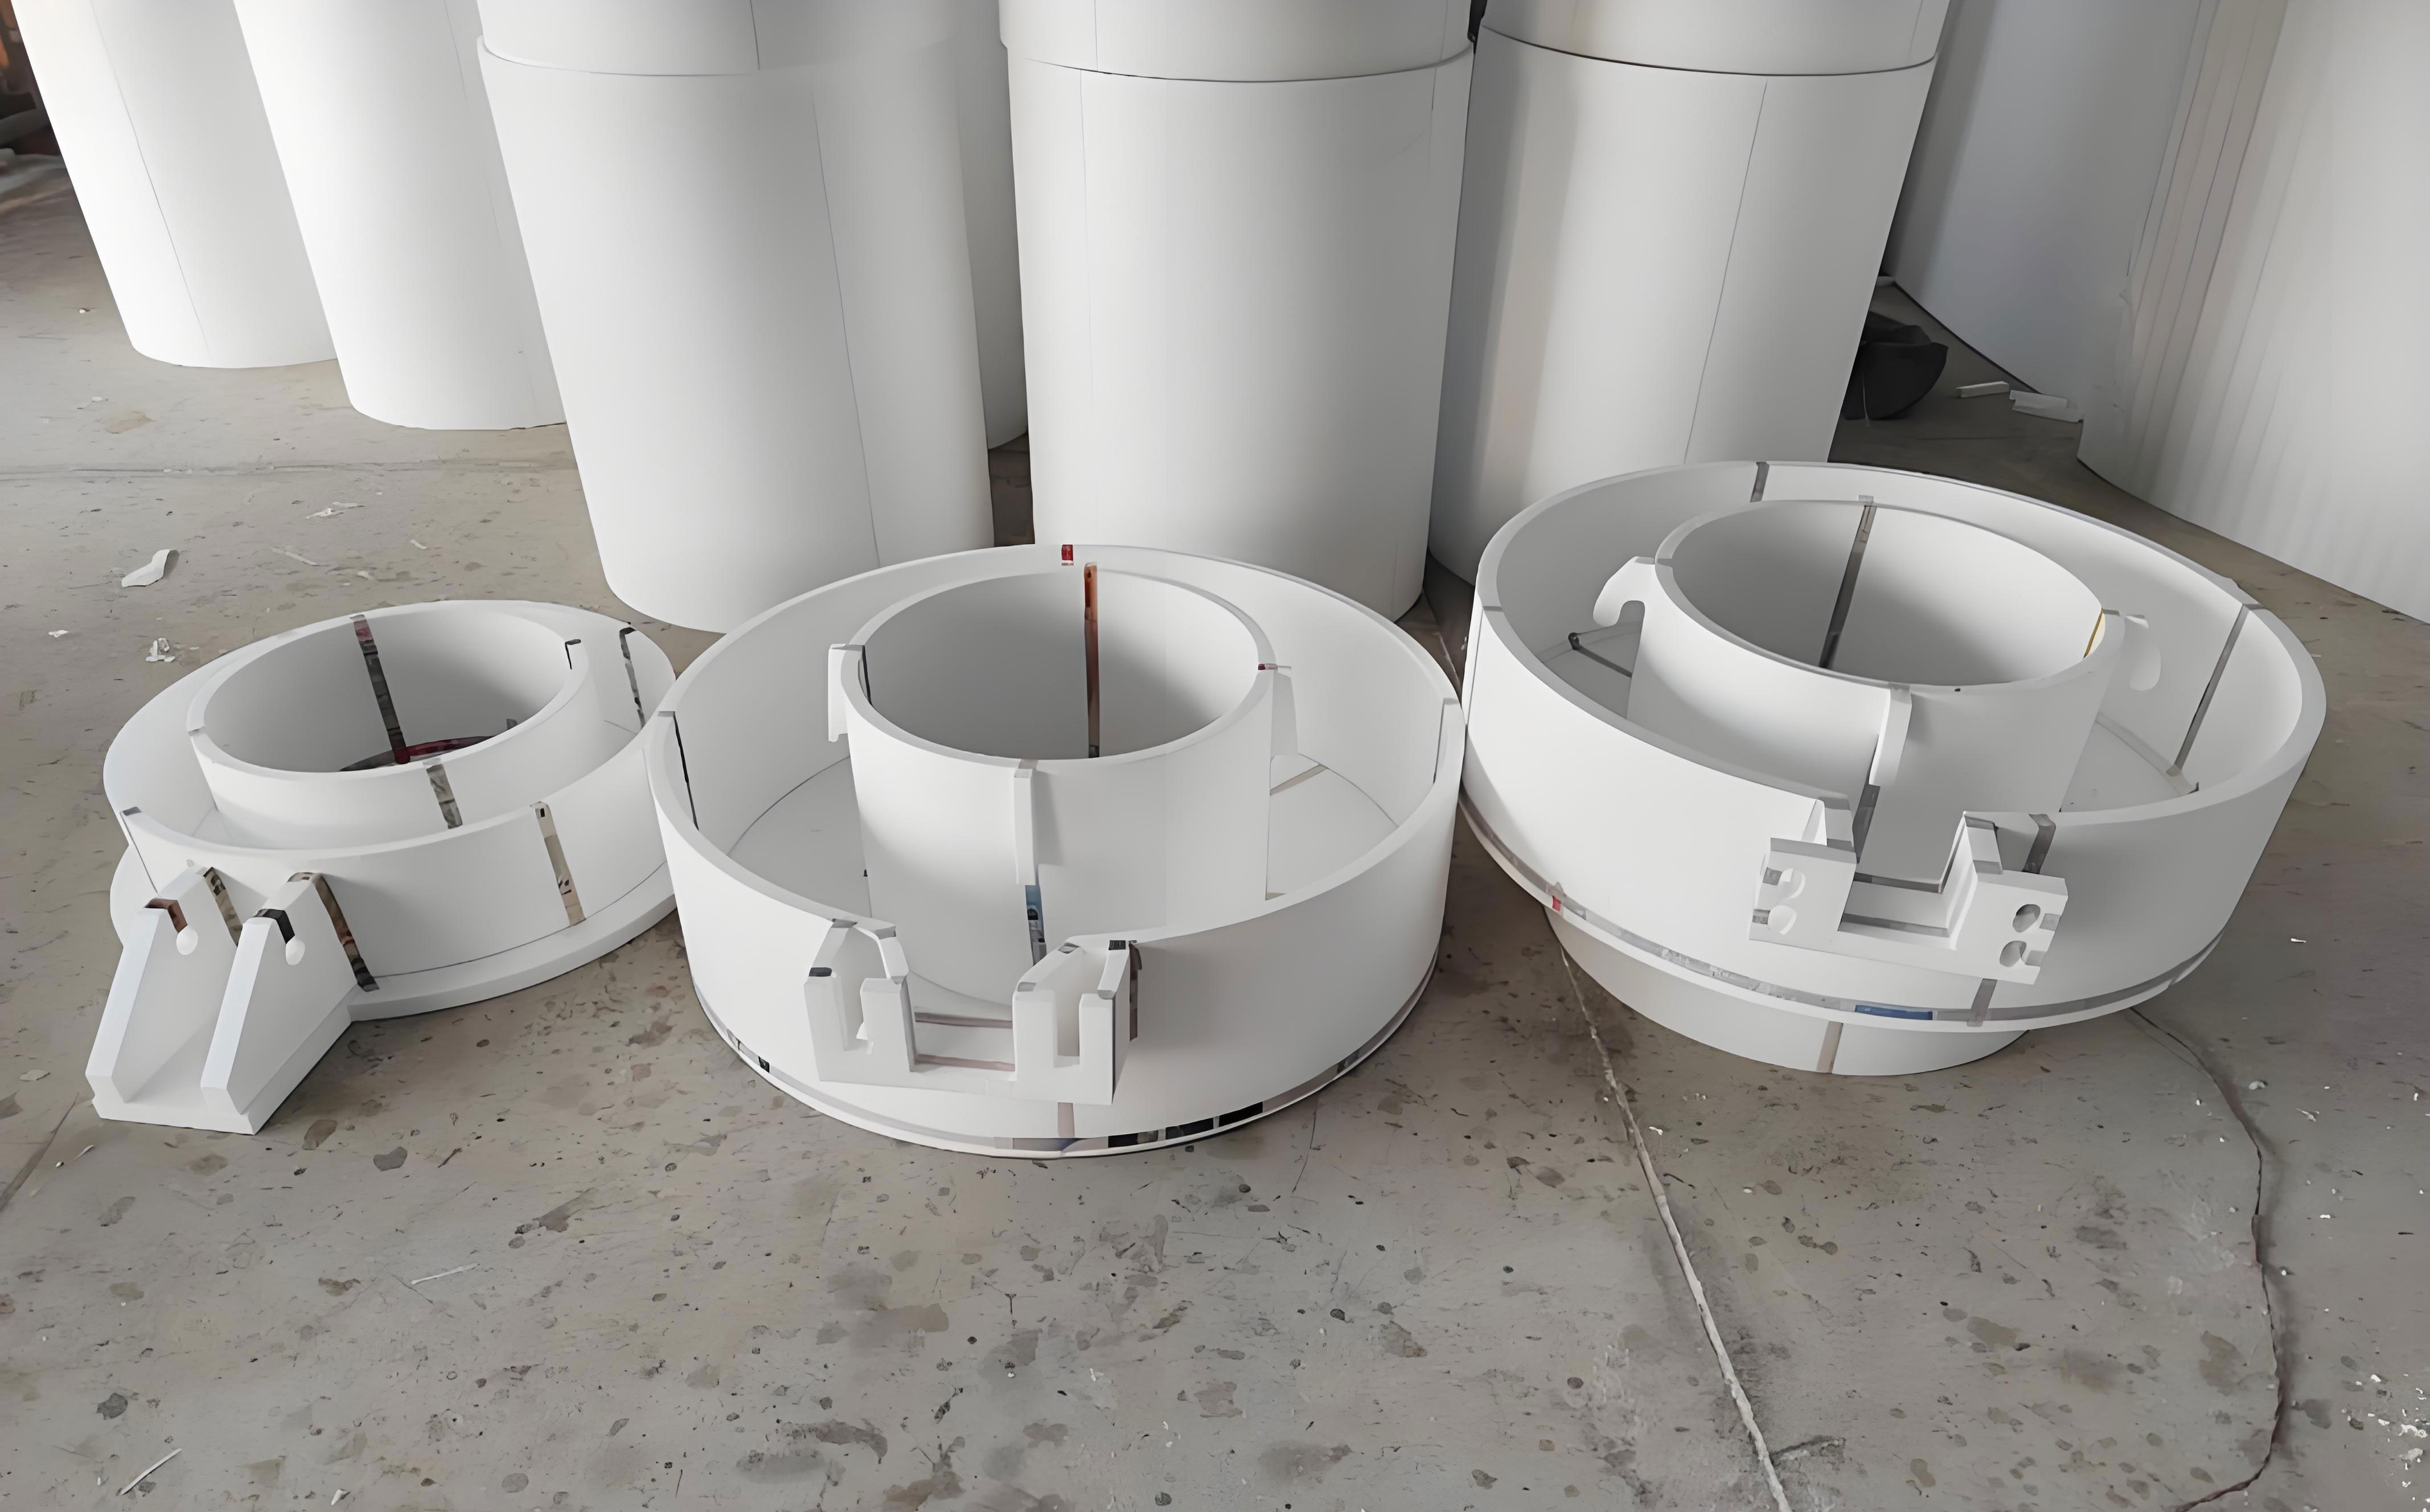
1. Key Process Analysis of Lost Foam Casting in Mass Production
1.1 Pattern Preparation and Pretreatment
In my lost foam casting mass production line, the foam pattern is the source of many defects. The carbon content and density of the foam pattern affect the pyrolysis products during pouring. EPS material depolymerizes at 600–800 °C, and each gram of pattern generates 800–1,000 mL of gas. I select low-density beads at 17–19 kg/m³ and low residual carbon to reduce free carbon, and I use precise weighing tools to control the pre-expanded bead density to prevent local carburization or back-spraying. The gas evolution can be estimated by the following relationship:
$$
V_{gas} = \alpha \cdot m_{foam} \cdot (T_p – T_{dep})
$$
where alpha is the gas yield coefficient, m is the foam mass, Tp is the pouring temperature, and Tdep is the depolymerization temperature. For STMMA copolymer, the gas evolution is about 25% lower than that of EPS. Pre-expanded beads need maturation. For EPS I use 4–16 h, and for STMMA I use 5–10 days to balance pressure. After maturation, the beads are molded with steam pressure adjusted by time. For large machine tool castings, I optimize the feed inlet to avoid incomplete filling. Complex castings are divided into blocks and bonded; I control adhesive amount and curing time to prevent carbon-rich zones at bonded areas. In mass production, I use 3D modeling to optimize gating and riser layout, ensuring a smooth filling path and reducing dead-zone carbon deposition. For pattern assembly, multiple foam patterns are clustered by bonding or mechanical connection. Before bonding, I polish and apply adhesive under pressure. For mechanical connection, I reserve holes in the mold design and control tolerance within ±0.5 mm.
| Parameter | EPS | STMMA | Recommended Range |
|---|---|---|---|
| Density | 17–20 kg/m³ | 17–19 kg/m³ | 18 ± 1 kg/m³ |
| Residual carbon | Higher | About 15% lower | ≤ 0.3% |
| Maturation time | 4–16 h | 5–10 days | Balance internal pressure |
| Gas evolution | 800–1,000 mL/g | About 25% lower | ≤ 150 mL/g |
| Depolymerization temperature | 600–800 °C | 600–800 °C | Match pouring temperature |
| Pattern assembly tolerance | — | — | ±0.5 mm |
1.1.1 Foam Material Selection and Density Control
I prefer STMMA copolymer foam over EPS because its carbon content is about 15% lower. I strictly control the density at 18 ± 1 kg/m³. Before entering the warehouse, I sample and test the pyrolysis residual carbon, which must be ≤ 0.3%. This is critical for HT300 gray iron because the base carbon is already 3.0%, and even a small amount of surface carburization can raise hardness above 230 HBW and make machining difficult. Therefore, zero-tolerance control of foam carbon residue is necessary in lost foam casting.
1.1.2 Maturation and Molding
Pre-expanded beads must be matured. EPS requires 4–16 h, while STMMA requires 5–10 days to balance pressure. After maturation, the mold is formed, and steam pressure is adjusted with time as an auxiliary control. For large machine tool castings, I optimize the feed inlet to avoid insufficient filling. The pattern density influences both gas evolution and dimensional stability, so I monitor it as a critical variable in lost foam casting.
1.1.3 Mold Structure Design and Combination Process
For complex castings, I use block bonding and control the adhesive amount and curing time to prevent carbon-rich zones at bonded areas. In mass production, 3D modeling is used to optimize the gating and riser layout, ensuring a smooth filling path and reducing dead-zone carbon deposition. This step is essential because improper gating increases the risk of burn-on, cold shut, and carbon defects in lost foam casting.
1.1.4 Pattern Assembly Technology
For complex castings, I combine multiple foam patterns into clusters by bonding or mechanical connection. Before bonding, I polish the surfaces, apply adhesive, and press them together. For mechanical connection, I reserve holes in the mold design and control the tolerance within ±0.5 mm. This practice stabilizes the pattern cluster during sand filling and vacuum application, which is important for dimensional accuracy in lost foam casting mass production.
1.2 Coating Preparation and Coating Process
1.2.1 Coating Formula Optimization
The refractory aggregate, such as quartz powder or zircon powder, must have a particle size distribution that matches the casting wall thickness. Coarse particles at 70–140 mesh improve permeability, while fine particles above 200 mesh enhance burn-on resistance. The binder, such as silica sol or bentonite, must balance coating strength and peelability to prevent residual coating after pouring. I add 0.5%–1% flake graphite at 325 mesh or 0.3% short carbon fiber to raise the thermal conductivity to 1.0–1.5 W/(m·K), accelerating foam vaporization and reducing high-temperature pyrolysis carbon retention. The Baume degree is controlled at 65–70 °Bé. The coating thermal resistance can be expressed as:
$$
R_{coat} = \frac{t_c}{k_c}
$$
where tc is the coating thickness and kc is the coating thermal conductivity. For lost foam casting, the coating must allow gas to escape while resisting metal penetration.
| Component | Function | Content or Range |
|---|---|---|
| Quartz, zircon, or bauxite | Refractory aggregate | Match wall thickness |
| Coarse particles | Permeability | 70–140 mesh |
| Fine particles | Burn-on resistance | Above 200 mesh |
| Flake graphite | Thermal conductivity | 0.5%–1% |
| Short carbon fiber | Thermal conductivity | 0.3% |
| Silica sol or bentonite | Binder | Balance strength and peelability |
| Baume degree | Coating consistency | 65–70 °Bé |
| Thermal conductivity | Heat transfer | 1.0–1.5 W/(m·K) |
1.2.2 Coating and Drying Control
I use dipping or spraying to ensure a uniform coating. The coating thickness is controlled at 0.8–1.5 mm for general castings, and the upper limit is used for thick-walled castings. The drying room temperature is controlled at 50–55 °C for at least 12 h to prevent foam softening, deformation, and back-spraying during pouring. In my lost foam casting process, coating thickness directly affects gas permeability, surface roughness, and burn-on resistance.
1.3 Sand Compaction and Negative Pressure System Regulation
1.3.1 Vibration Compaction Parameter Optimization
The vibration table frequency is 30–50 Hz, and the amplitude is 0.5–1.0 mm, adjusted according to the casting structure. For complex cavities, I use low-frequency and high-amplitude vibration to ensure uniform filling of dry sand at 70/140 mesh quartz sand and to avoid mold collapse. I use a hardness tester to check compaction and control the sand mold surface hardness to at least 85 B-type. In lost foam casting mass production, vibration parameters influence sand filling density and dimensional stability.
1.3.2 Dynamic Control of Negative Pressure System
Before pouring, I pre-evacuate to 0.04–0.06 MPa. During pouring, the vacuum is dynamically adjusted according to casting size: small castings maintain stable negative pressure, while large castings briefly increase to 0.07 MPa during filling to promote pyrolysis gas discharge and avoid porosity and carburization. After filling, I maintain pressure for 8–12 min because HT300 has a longer solidification time than cast steel. The gas evacuation rate can be approximated by:
$$
Q_{evac} = \frac{\Delta P \cdot A}{\mu \cdot (R_{coat} + R_{sand})}
$$
where ΔP is the pressure difference, A is the flow area, μ is the gas viscosity, Rcoat is the coating resistance, and Rsand is the sand resistance. This relationship guides my vacuum setting in lost foam casting.
| Stage | Small Castings | Large Castings | Duration |
|---|---|---|---|
| Pre-evacuation | 0.04–0.06 MPa | 0.04–0.06 MPa | About 6 min |
| Filling | Stable negative pressure | Briefly up to 0.07 MPa | During filling |
| Holding | 0.045–0.055 MPa | 0.05–0.06 MPa | 8–12 min |
| Fluctuation | ≤ 0.005 MPa | ≤ 0.005 MPa | Whole cycle |
1.4 Melting, Pouring, and Filling Control
1.4.1 Iron Composition and Temperature Control
HT300 is a high-strength gray cast iron, and I strictly control the carbon equivalent (CE) at 3.7%–3.9% to ensure castability and mechanical properties. I use medium-frequency induction furnace melting with ladle inoculation. The carbon content is controlled at 2.9%–3.2%, silicon at 1.6%–1.8%, and 0.3%–0.5% FeSi75 is added for instantaneous inoculation to refine graphite and improve strength. Sulfur and phosphorus are controlled at ≤ 0.08% to avoid hot tearing. The carbon equivalent is calculated as:
$$
CE = C + \frac{Si + P}{3}
$$
Pouring temperature is controlled at 1,400–1,460 °C to ensure fluidity. Insufficient superheat causes incomplete filling and cold shut, while excessive temperature causes graphite coarsening, increased shrinkage tendency, and inoculation fade. My process checks include a triangular test piece for white iron depth, which should be 1–3 mm; thermal analysis before pouring to confirm CE; and control of the time from tapping to pouring at no more than 15 min to prevent inoculation fade. Superheat is estimated by:
$$
\Delta T_{super} = T_p – T_{liquidus}
$$
where Tp is the pouring temperature and Tliquidus is the liquidus temperature of HT300. In lost foam casting, superheat must be balanced against foam pyrolysis and gas evolution.
| Element or Parameter | Range |
|---|---|
| C | 2.9%–3.2% |
| Si | 1.6%–1.8% |
| Mn | 0.6%–1.0% |
| P | ≤ 0.08% |
| S | ≤ 0.08% |
| CE | 3.7%–3.9% |
| FeSi75 | 0.3%–0.5% |
| Pouring temperature | 1,400–1,460 °C |
| White iron depth | 1–3 mm |
| Tap-to-pour time | ≤ 15 min |
1.4.2 Pouring Speed and Filling Path
Because HT300 has good fluidity and a narrow freezing range, shrinkage and porosity are common. The gating system must balance smooth filling and feeding capacity. I use a bottom-gated open gating system with the area ratio ΣSinner : ΣSrunner : ΣSsprue = 1 : 1.5 : 2 to reduce filling pressure and minimize sand wash and gas defects. A slag-blocking baffle and filter mesh are placed in the runner to remove oxide slag and unmelted inoculant particles. The inner gates follow the principle of near-hot and far-cold: gates are placed near thick sections to promote directional solidification, while thin sections receive metal early to prevent cold shut. A riser or overflow riser is placed in the last filling region to collect initial metal and feed shrinkage. I use graphite chills locally to adjust the temperature gradient and eliminate porosity. The filling time can be estimated by:
$$
t_f = \frac{V_c}{A_g \cdot v_g}
$$
where Vc is the casting volume, Ag is the gate area, and vg is the gate velocity. The Reynolds number helps me judge flow stability:
$$
Re = \frac{\rho \cdot v \cdot D}{\mu}
$$
For HT300 in lost foam casting, I keep the pouring time short and stable, no more than 30 s per box depending on casting size. I maintain continuous and steady pouring to prevent secondary oxidation and gas entrainment. After pouring, I delay shakeout for at least 2 h to prevent hot tearing and deformation.
| Gating Parameter | Value or Range |
|---|---|
| Gating type | Bottom-gated open system |
| Area ratio | 1 : 1.5 : 2 |
| Filling speed | 1.5–2.5 cm/s |
| Front speed | 6–10 cm/s |
| Pouring time per box | ≤ 30 s |
| Delay before shakeout | ≥ 2 h |
2. Mass Production Quality Defects and Control Strategies
2.1 Material-Side Control
2.1.1 Foam Pattern
I select STMMA copolymer foam, which has about 15% lower carbon content than EPS. The density is strictly controlled at 18 ± 1 kg/m³. Before use, I sample and test the pyrolysis residual carbon, which must be ≤ 0.3% to prevent carbon deposition on the casting surface and local carburization. In HT300, even slight carburization can increase surface hardness above 230 HBW and make machining difficult, so foam carbon residue must be controlled with zero tolerance in lost foam casting.
2.1.2 Adhesive
I use a low-carbon cold adhesive specially designed for lost foam casting, such as a polyvinyl alcohol-starch-based adhesive. The adhesive amount is ≤ 0.3 g/cm² to reduce organic carbon sources. I strictly prohibit adhesives containing benzene-based solvents.
2.1.3 Pattern Drying
After bonding, the pattern is dried with hot air at 60 °C for at least 2 h to remove moisture and volatiles, reducing gas evolution and carbon residue. This step is important for stable lost foam casting mass production.
2.1.4 Special Attention
HT300 gray cast iron itself contains about 3.0% carbon, so it is more sensitive to carburization. Even a small amount of surface carburization may raise hardness above 230 HBW and cause machining difficulty. Therefore, I apply zero-tolerance control to foam carbon residue in my lost foam casting process.
2.2 Process-Side Optimization
2.2.1 Coating Modification
I add 0.5%–1% flake graphite at 325 mesh or 0.3% short carbon fiber to the refractory coating to raise the thermal conductivity to 1.0–1.5 W/(m·K). This accelerates foam vaporization and reduces high-temperature pyrolysis carbon retention. The coating must also maintain adequate permeability and strength.
2.2.2 Negative Pressure System Management
Before pouring, I pre-evacuate to 0.045–0.055 MPa. During filling, I keep the fluctuation within 0.005 MPa. After filling, I maintain pressure for 8–12 min because HT300 has a longer solidification time than cast steel. This ensures that residual hydrocarbon gas is removed and prevents gas porosity or carbon black inclusions caused by blocked graphitization expansion. The pressure differential is:
$$
\Delta P = P_{pre} – P_{mold}
$$
where Ppre is the pre-evacuation pressure and Pmold is the pressure inside the mold. This control is central to my lost foam casting strategy.
2.2.3 Pouring Temperature and Speed
I control the pouring temperature at 1,400–1,450 °C to avoid excessive foam pyrolysis. The filling speed is kept at 1.5–2.5 cm/s to reduce thermal shock and extend the foam vaporization window. In lost foam casting, this balance is essential for defect prevention.
2.3 Sand Inclusion and Burn-On Control
2.3.1 Sand Requirements
I use high-purity quartz sand with SiO2 ≥ 98% and a grain size of 40/70 mesh. The mud content is less than 0.3%. I screen the sand daily to remove fines below 200 mesh. The loss on ignition is less than 0.5% to prevent gas generation from organic impurities.
2.3.2 Coating Performance Optimization
The aggregate system uses bauxite and 5%–8% flake graphite to balance refractoriness and lubricity. The room-temperature strength is at least 0.8 MPa, and the high-temperature strength at 1,000 °C is at least 1.0 MPa. The permeability is at least 600×10⁻⁶ m²/(Pa·s), which favors gas discharge. The thermal conductivity is 0.9–1.3 W/(m·K), close to that of cast iron, reducing chill-induced burn-on. The coating thickness is 0.8–1.2 mm; too thick and it cracks, too thin and burn-on resistance is insufficient.
2.4 Gating System Improvement
2.4.1 Sprue
I use a hollow ceramic tube or hollow foam structure for the sprue to reduce gas evolution volume by more than 30%. This reduces the gas load in lost foam casting.
2.4.2 Pouring Cup
The pouring cup capacity is increased by 25%, and a buffer baffle is installed to reduce the impact velocity of the molten iron.
2.4.3 Filling Speed Control
I use high-speed photography to observe the metal front. The optimal filling speed is 6–10 cm/s. A speed above 12 cm/s tends to wash away the coating and cause mechanical burn-on. A speed below 5 cm/s may cause cold shut or wrinkle because HT300 has good fluidity but low temperature tolerance.
2.4.4 Negative Pressure Assisted Slag Removal
I add a suction side pipe above the pouring cup to form a slight negative pressure, which promotes slag flotation and adsorption on the filter mesh. This improves cleanliness in lost foam casting.
2.5 Distortion and Dimensional Accuracy Control
2.5.1 Cooling and Shakeout Process
The in-box cooling time is at least 120 min for a wall thickness of 20 mm, and it is extended by 30 min for every additional 10 mm of wall thickness. Insufficient cooling can cause stress distortion or dimensional growth in gray cast iron. The shakeout temperature is controlled below 180 °C to prevent volume changes. The free linear shrinkage of HT300 is 0.8%–1.1%, and I set the mold shrinkage at 1.0% for length, width, and height. Ribs and bosses are set at 0.6%–0.8%. After shakeout, I use a 3D scanner after 24 h to measure and feed back corrections to the mold. For large flat castings, I place high-temperature ceramic support columns in the sand box to prevent gravity distortion. The cooling time can be estimated by:
$$
t_{cool} = 120 + 30 \left( \frac{w – 20}{10} \right)
$$
where w is the wall thickness in mm. The shrinkage is calculated as:
$$
\epsilon = \frac{L_m – L_c}{L_m} \times 100\%
$$
where Lm is the mold dimension and Lc is the casting dimension. These equations help me set pattern allowance in lost foam casting.
2.5.2 Automated Inspection and Closed-Loop Control
I use machine vision with a high-resolution industrial camera and an AI defect recognition model to detect multiple surface defects with 0.1 mm precision in less than 30 s per piece. The data are uploaded to the MES for alarm handling. I also use a coordinate measuring machine for sampling inspection at 5% per batch to measure hole distances and other features. If the deviation exceeds ±0.3 mm, I trace back the parameters and build a correlation database for AI parameter adjustment. The closed-loop control flow is: 3D scanning or CMM → dimensional deviation analysis → AI model diagnosis → adjustment of mold shrinkage and other parameters. This approach stabilizes lost foam casting mass production.
| Defect | Root Cause | Shop-Floor Countermeasure | Long-Term Countermeasure |
|---|---|---|---|
| Burn-on | Insufficient vacuum and coating burn-off or cracking, causing metal penetration and pinning in sand capillaries | Stop the line and check vacuum pump seals to ensure vacuum ≤ 0.055 MPa; brush two additional refractory coating layers on the affected area, dry at 50 °C for 30 min, and then pour | Add 3%–5% white latex and 0.5% fiber to the coating, with a sintering resistance temperature ≥ 1,600 °C; use PID closed-loop control for vacuum zones, with one vacuum gauge per 0.5 m² |
| Gas porosity | Foam density too high or vacuum extraction rate lower than gas generation rate, so gas is trapped by the metal | Reduce foam density to 18 ± 1 kg/m³; pre-evacuate for 6 min to 0.06 MPa; change top gating to bottom gating with stepped gates and filling speed below 25 cm/s | Use STMMA copolymer to reduce gas evolution by 25%; add a condenser tank to the vacuum main line; use CAE simulation of filling-solidification-vacuum coupling to optimize vent positions |
| Wrinkle and carbon deposit | Pyrolysis carbon cannot be discharged under negative pressure and deposits on the upper surface and hot spots | Increase pouring temperature by 30 °C to extend flow time; add an overflow slag-collecting riser on the upper surface to let the carbon film overflow | Add 2% iron oxide powder to the coating to promote carbon combustion; use pulsed negative pressure of 0.05 MPa → 0 → 0.05 MPa with a 3 s cycle to peel off the carbon film |
| Cold shut | Excessive negative pressure causes premature pressure loss at the metal front, and flow velocity drops so two metal streams cannot merge | Reduce vacuum to 0.04 MPa; add a choke plate to the pouring cup to maintain a 30 mm metal head; raise foam pattern temperature to 45 °C to reduce chilling | Increase runner cross-sectional area by 20%; wrap the runner with a heat-insulating sleeve so metal temperature loss is less than 15 °C |
| Inclusions | Vacuum suction draws loose sand and coating fragments into the mold cavity | Place a 200-mesh ceramic filter at the bottom of the sprue; blow away floating dust after coating drying and prohibit dry sandpaper grinding | Add a double-layer stainless steel mesh and non-woven fabric filter inside the suction port; install a 0.3 t permanent magnetic drum in the sand circulation system with iron removal rate ≥ 95% |
| Distortion | Foam pattern undergoes secondary expansion and contraction during 60 °C drying and under vacuum, causing casting growth or twisting | Cool the foam setting frame to ≤ 35 °C before demolding; let the white pattern stand for 24 h after bonding to release stress | Use a foam pattern pre-shrinkage process and CNC machine the foam according to casting linear shrinkage plus 0.8%; use five-point spot welding support and resin sand backing to prevent box wall displacement under vacuum |
| Shrinkage and porosity | Lost foam casting under vacuum has no riser feeding, and the feeding channel at hot spots closes prematurely | Attach an exothermic riser sleeve of ϕ40/50 mm above the hot spot with exothermic time ≥ 90 s; add cooling ribs at the end to create directional solidification | Introduce vacuum differential pressure process: reduce vacuum from 0.05 MPa to 0.02 MPa within 0.3 s after pouring to establish feeding pressure; use solidification simulation to control porosity level ≤ 2 |
| Rough surface | Uneven coating thickness below 0.3 mm, sand grain size too coarse at 40/70 mesh, and vacuum suction pulls coating through | Use primary dipping and secondary flow coating, with wet thickness 1.2 mm and dry thickness 0.6 mm; screen sand to AFS fineness 55–60 to reduce surface sand marks | Add 1% nano-Al2O3 to the coating to improve suspension and keep brush marks below 5 µm; use zoned vacuum control with 0.04 MPa near the casting and 0.06 MPa far from the casting to reduce coating penetration |
3. Batch Production Practice for Machine Tool Castings
3.1 Current Production Status
The lost foam casting line I studied produces 20,000 tons per year of HT300 gray iron castings. The initial scrap rate was 12%. After applying the integrated strategy, the burn-on area on HT300 castings is less than 1%, Ra is ≤ 25 µm, and there is no penetrating burn-on. Cleaning labor is reduced by 40%. Under the same conditions, the STMMA foam plus graphite coating plus holding process gives a surface carburized layer of less than 0.2 mm and a hardness increase of no more than 15 HBW, with good machinability. I also apply four-stage management of defect → root cause → shop-floor countermeasure → long-term countermeasure to control quality defects in parallel.
3.2 Casting Improvement Measures and Effects
The defects I encounter most often in lost foam casting mass production are burn-on, gas porosity, wrinkle and carbon deposit, cold shut, inclusions, distortion, shrinkage, and rough surface. Through systematic countermeasures, each defect can be suppressed to an acceptable level. The key is to link foam quality, coating performance, vacuum control, gating design, and cooling practice into one closed loop. Because HT300 is highly sensitive to carbon and chilling, the foam pattern must be low in residual carbon, the coating must balance permeability and strength, and the vacuum must be dynamically adjusted rather than held at a single level. The pouring temperature must remain within 1,400–1,460 °C, and the time from tapping to pouring must not exceed 15 min. In my experience, these measures are most effective when they are applied together rather than individually.
For burn-on, the most important shop-floor action is to stop the line and confirm vacuum tightness. The long-term solution is to modify the coating with white latex and fiber and to use PID zone control for the vacuum system. For gas porosity, lowering foam density and using pre-evacuation reduces the gas load. For wrinkle and carbon deposit, increasing pouring temperature and adding an overflow riser helps to discharge the carbon film. For cold shut, reducing vacuum and increasing the metal head are effective. For inclusions, filtration and magnetic separation are necessary. For distortion, pattern pre-shrinkage and stress relief are key. For shrinkage, exothermic risers and vacuum differential pressure are useful. For rough surface, coating thickness control and fine sand are essential.
4. Conclusion and Outlook
4.1 Conclusion
The key to lost foam casting mass production is multi-process cooperative control. Pattern preparation must balance density and structure. The coating process must balance permeability and strength. Sand compaction and pouring must precisely regulate vibration, negative pressure, and filling parameters. Through material selection, process optimization, and targeted defect prevention, casting quality stability can be improved. The main key parameters are listed in the following tables. These values have been validated in my lost foam casting production and provide a practical basis for HT300 machine tool casting manufacturing.
| No. | Parameter Category | Control Item | Recommended Value or Range |
|---|---|---|---|
| 1 | Coating | Thickness for general castings | 1.5–2.0 mm |
| 2 | Coating | Baume degree | 65–70 °Bé |
| 3 | Dry sand | Mohs hardness | ≥ 7.5 |
| 4 | Vacuum | Negative pressure range | 0.04–0.06 MPa |
| 5 | Foam pattern | Density | 17–19 kg/m³ |
| 6 | Pre-expansion | Temperature | 90–105 °C |
| 7 | Foam | Gas evolution | ≤ 150 mL/g |
| 8 | Pouring | Pouring temperature | 1,400–1,460 °C |
| 9 | Coating | Thickness for thin-walled castings | 0.8–1.2 mm |
| 10 | Coating | Thickness for thick-walled castings | 1.5–2.0 mm |
| Control Item | Foam Density | Drying Temperature | Drying Time | Moisture Content |
|---|---|---|---|---|
| Parameter Requirement | (18 ± 1) kg/m³ | 30–40 °C | 24–48 h | ≤ 0.3% |
| Control Item | Vibration Frequency | Vibration Time | Dimensional Accuracy | Joint Gap Requirement |
|---|---|---|---|---|
| Parameter Requirement | 25–30 Hz | 30–60 s | ±0.2 mm by CMM | ≤ 0.5 mm |
4.2 Outlook
In the future, I plan to develop a multi-sensor fusion system that tracks foam pyrolysis, molten iron filling, and negative pressure changes in real time so that process parameters can be adjusted adaptively. I also intend to explore degradable foam materials and environmentally friendly coatings to further reduce carbon emissions and promote low-carbon upgrading of lost foam casting. The combination of AI-based closed-loop control and green materials will make lost foam casting more stable, more efficient, and more sustainable for HT300 machine tool castings.
Overall, my work shows that lost foam casting can achieve low scrap rate, low burn-on, low carburization, and good machinability in HT300 machine tool castings when the material, process, and defect-control loops are tightly coupled. The method is practical for mass production and can be transferred to other gray iron castings with similar wall thickness and quality requirements. The most important lesson is that no single parameter controls quality; the success of lost foam casting depends on the coordinated control of foam density, coating permeability, vacuum dynamics, gating design, pouring temperature, and cooling time.