
As a practitioner in the foundry industry, I have extensively worked on optimizing casting processes for complex components, particularly shell castings. The torque converter shell for forklift trucks represents a classic example of such shell castings, where traditional resin sand casting methods often fall short due to intricate geometries and high precision requirements. In this article, I will delve into the transition to lost foam casting for these shell castings, sharing insights from my firsthand experience. The goal is to achieve near-net-shape production, minimize machining allowances, and enhance overall quality. Throughout this discussion, I will emphasize the critical aspects of shell castings, using tables and formulas to summarize key data and principles.
The lost foam casting process, also known as evaporative pattern casting, involves using foam patterns that vaporize upon contact with molten metal, allowing for precise replication of complex shapes. For shell castings like the torque converter shell, this method offers significant advantages over conventional methods. Historically, resin sand casting was employed, but it required extensive core-making, assembly, and molding steps, leading to inefficiencies and defects such as dimensional inaccuracies and flash. Lost foam casting eliminates the need for cores and mold parting lines, enabling 100% repeatability and reducing post-casting operations. The dimensional tolerances can achieve CT5 to CT7 grades, with surface roughness Ra values as low as 6.3 to 12.5 μm. This makes it ideal for thin-walled shell castings, where maintaining structural integrity and minimizing weight are paramount.
In my work, I focused on the torque converter shell, which is a circular, open-box structure with an average wall thickness of 8 mm. These shell castings feature a thin-shell basin opening, side openings, hollow sections, and a large machined base plane. The complexity arises from the varying wall thicknesses, which range from thin sections prone to distortion to thicker areas susceptible to shrinkage defects. The primary technical challenges included preventing deformation in the basin opening, avoiding internal shrinkage porosity, and ensuring accurate pattern assembly. To address this, the foam pattern was divided into segments—bottom, middle, and upper sections—fabricated separately and then bonded using adhesive. This segmentation reduced complexity and allowed for precise molding. However, pattern distortion during handling and casting remained a concern, necessitating careful design and process adjustments.
The initial trials involved vertical gating systems, as illustrated in previous studies, but this led to significant deformation in the basin opening due to uneven shrinkage during solidification. The differential contraction between longitudinal and transverse directions caused dimensional inconsistencies, even with cross-bracing using wooden supports. This made vertical gating unsuitable for mass production. Consequently, I shifted to a horizontal gating system, where the basin opening was positioned horizontally. This orientation promoted uniform shrinkage across all directions, effectively minimizing distortion. The gating design was optimized by increasing the sprue diameter to enhance filling velocity and reduce mold lifting. Additionally, to mitigate sand sticking—a common issue in shell castings—a secondary coating application was implemented. After initial dip-coating, the patterns were spray-coated again, with manual brushing in narrow internal corners to ensure complete coverage. For remote, narrow oil holes prone to cold shuts, overflow risers were manually attached to facilitate metal flow.
To further refine the process, I utilized computer simulation software to model the filling and solidification stages. This allowed for virtual analysis of temperature gradients, flow patterns, and potential defect formation. Key parameters, such as pouring temperature, gate size, and cooling rates, were simulated to predict outcomes. For instance, the filling time $t_f$ can be estimated using the formula:
$$ t_f = \frac{V}{A \cdot v} $$
where $V$ is the volume of the casting, $A$ is the cross-sectional area of the gating system, and $v$ is the flow velocity. Similarly, solidification time $t_s$ for shell castings can be approximated by Chvorinov’s rule:
$$ t_s = k \left( \frac{V}{A_s} \right)^2 $$
where $k$ is a constant dependent on mold material and metal properties, and $A_s$ is the surface area of the casting. Through iterative simulations, I simplified the gating layout and adjusted riser placements to eliminate shrinkage in the base region. The table below summarizes the optimized process parameters for these shell castings:
| Parameter | Value | Unit |
|---|---|---|
| Pattern Material | Expandable Polystyrene (EPS) | – |
| Pattern Density | 20-25 | kg/m³ |
| Coating Thickness | 0.5-1.0 | mm |
| Pouring Temperature | 1350-1400 | °C |
| Gating System Type | Horizontal | – |
| Sprue Diameter | 40 | mm |
| Simulated Filling Time | 8-10 | s |
| Cooling Time | 120-150 | min |
The simulation results highlighted that proper venting and controlled pouring rates were crucial to avoid gas entrapment and carbon defects, common in lost foam casting of shell castings. By integrating these insights, the process was stabilized for batch production. Below is a visual representation of the final cast shell, illustrating the achieved precision and surface quality for such shell castings.
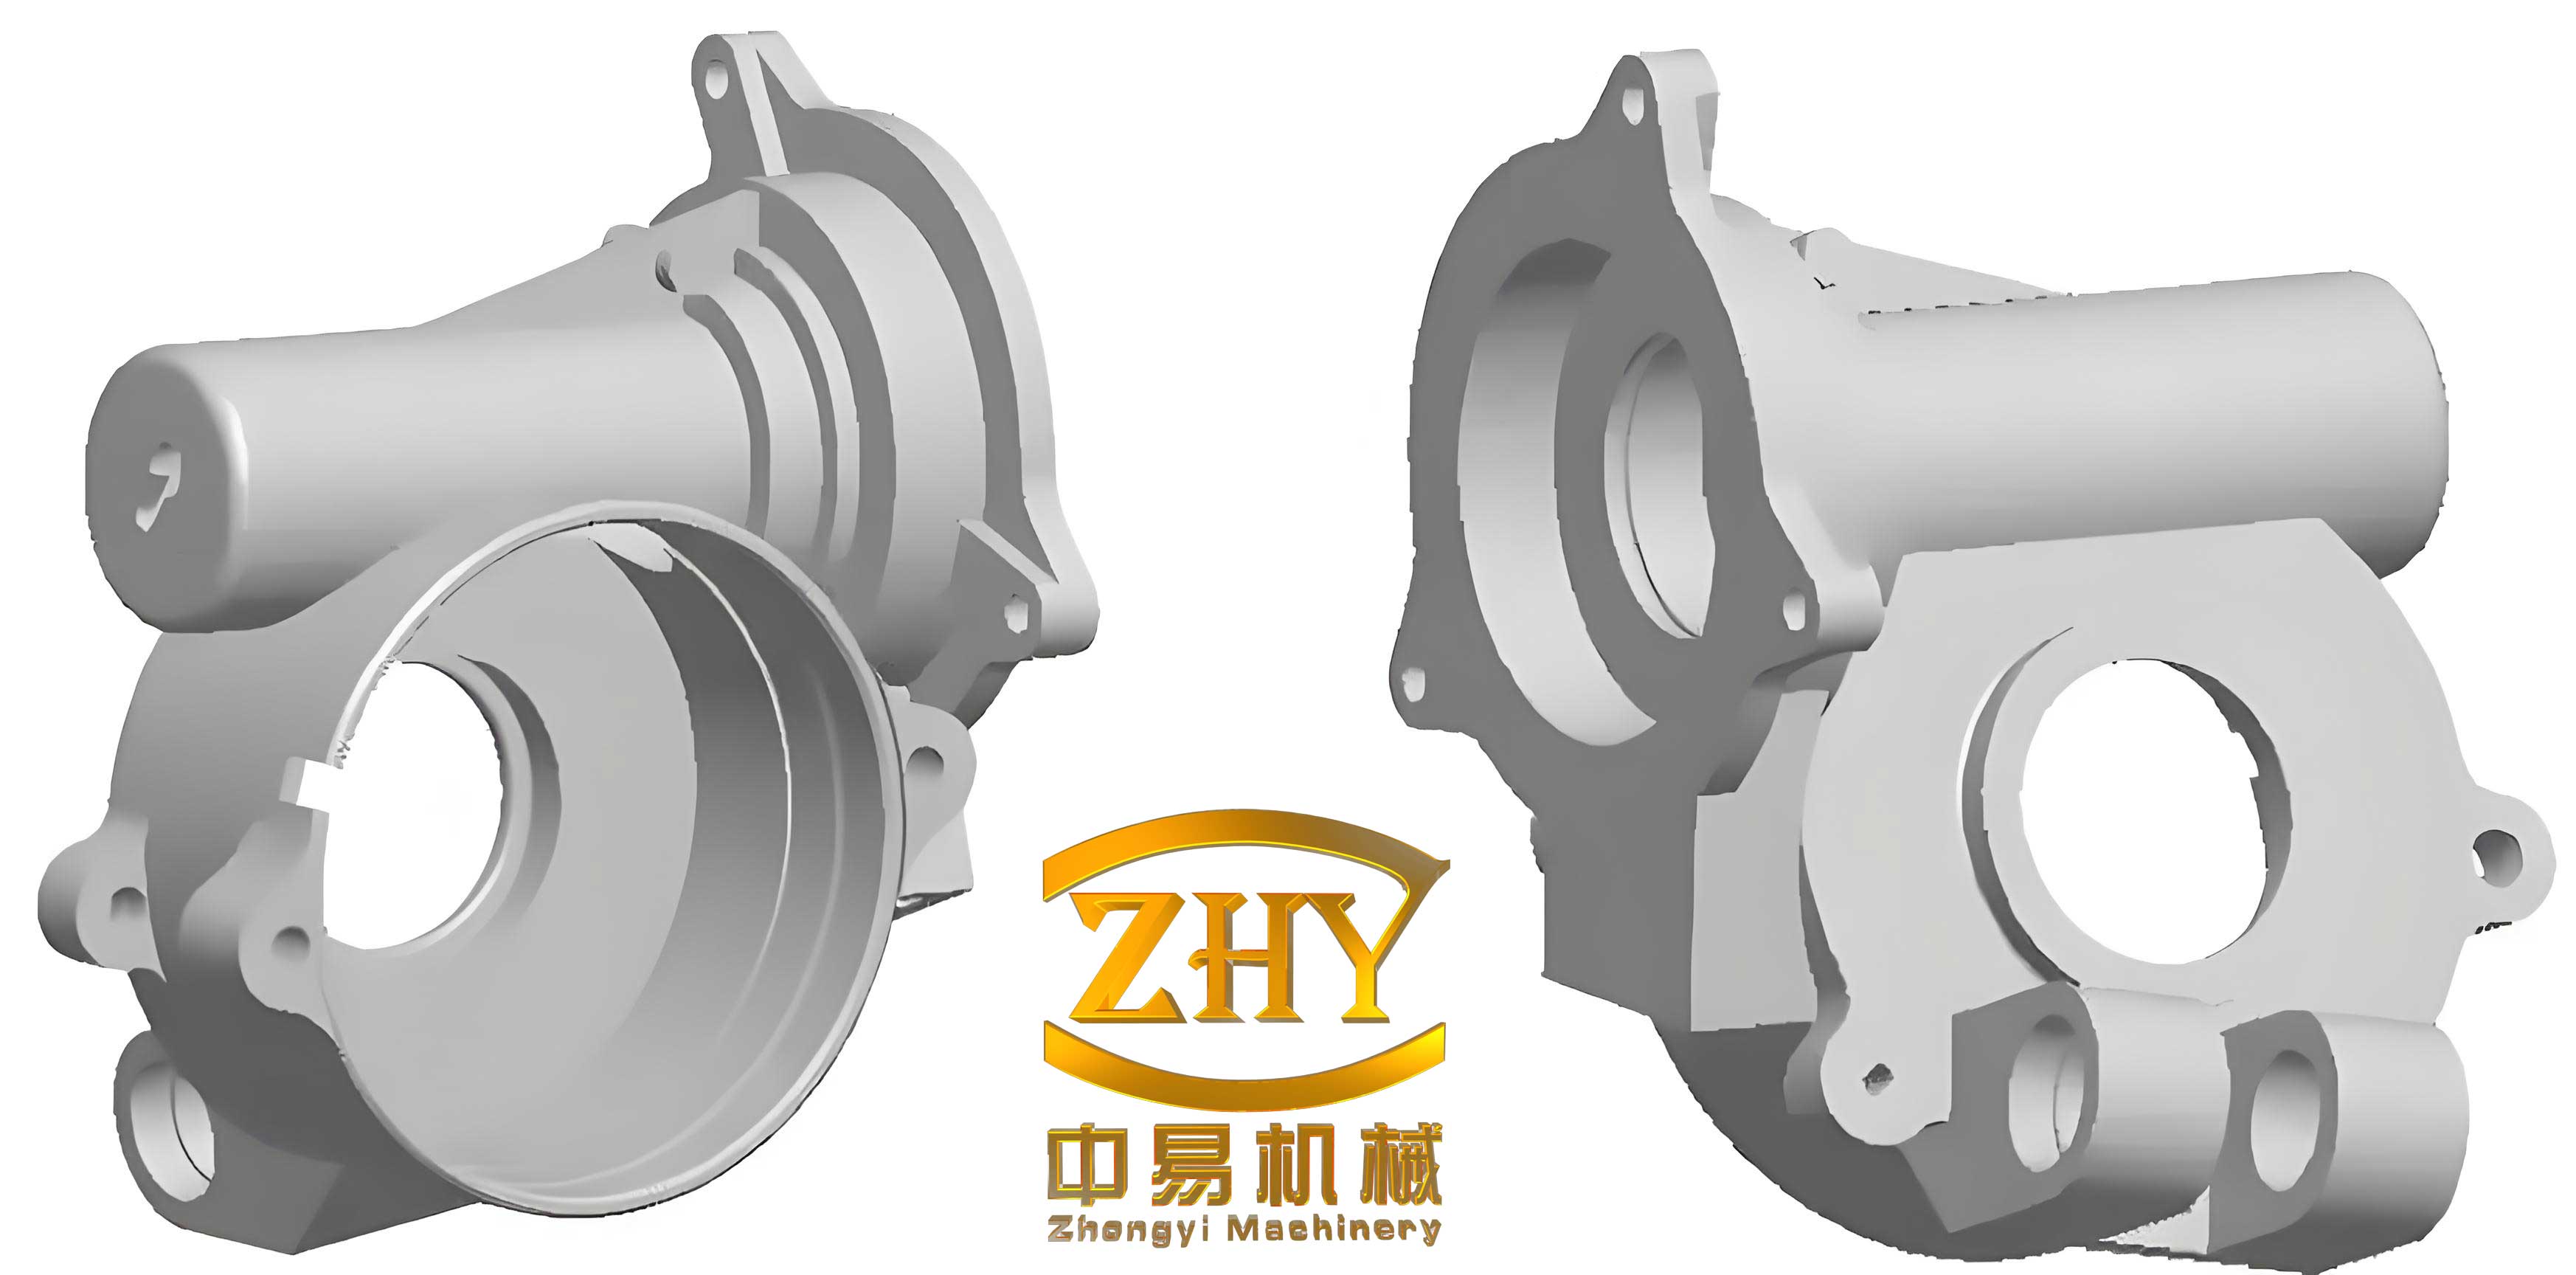
After several iterations of trial production and process adjustments, the lost foam casting method yielded high-quality torque converter shell castings. The performance metrics were rigorously evaluated to ensure compliance with design specifications. The dimensional accuracy was measured using coordinate measuring machines, revealing tolerances within CT6 to CT7 grades. Surface roughness was assessed with profilometers, showing Ra values between 6.3 and 12.5 μm. Machining allowances were reduced to MAE-F levels, and weight tolerances met MT4 to MT5 standards. Chemical composition, microstructure, and mechanical properties were also analyzed. For example, the tensile strength $\sigma_t$ and hardness HB were tested, with results satisfying industrial requirements. The table below provides a comprehensive overview of the key performance indicators for these shell castings:
| Performance Indicator | Target Value | Achieved Value | Standard |
|---|---|---|---|
| Dimensional Tolerance | CT6-7 | CT6-7 | ISO 8062 |
| Surface Roughness (Ra) | ≤12.5 μm | 6.3-12.5 μm | ISO 1302 |
| Machining Allowance | MAE-F | MAE-F | Custom |
| Weight Tolerance | MT4-5 | MT4-5 | ISO 10135 |
| Tensile Strength | ≥250 MPa | 260-280 MPa | ASTM A536 |
| Hardness (HB) | 180-220 | 190-210 | ASTM E10 |
| Defect Rate (Shrinkage) | <1% | 0.5% | Internal |
| Production Efficiency | High | 30% increase | Comparative |
The metallurgical quality was ensured through controlled melting practices, involving precise alloying and degassing. The chemical composition typically included iron with carbon, silicon, manganese, and trace elements, balanced to enhance fluidity and reduce shrinkage. The solidification behavior was modeled using the Fourier heat equation:
$$ \frac{\partial T}{\partial t} = \alpha \nabla^2 T $$
where $T$ is temperature, $t$ is time, and $\alpha$ is thermal diffusivity. This helped predict hot spots and optimize riser design. Additionally, the pattern shrinkage during fabrication was accounted for by adjusting mold dimensions based on empirical data. The linear shrinkage $\epsilon$ of EPS patterns can be expressed as:
$$ \epsilon = \beta \cdot \Delta T + \gamma $$
where $\beta$ is the thermal expansion coefficient, $\Delta T$ is the temperature change, and $\gamma$ is a material-specific constant. By calibrating these factors, the final shell castings met precise dimensional requirements without post-casting distortions.
From an economic perspective, transitioning to lost foam casting for these shell castings resulted in substantial cost savings. Compared to resin sand casting, the overall cost per ton decreased by approximately 1,000 currency units, driven by reduced labor, lower material waste, and fewer machining steps. The elimination of core boxes and mold assembly streamlined production, boosting efficiency by over 30%. Moreover, the environmental benefits were notable, as the process uses unbonded sand, simplifying reclamation and reducing waste disposal. The table below contrasts the key economic and operational factors between the two methods for producing shell castings:
| Aspect | Resin Sand Casting | Lost Foam Casting |
|---|---|---|
| Tooling Complexity | High (cores, molds) | Low (foam patterns only) |
| Production Cycle Time | Long (multi-step) | Short (integrated) |
| Material Utilization | ~60% | ~85% |
| Energy Consumption | Moderate | Low (no binder curing) |
| Scrap Rate | 3-5% | <1% |
| Machining Required | Extensive | Minimal |
| Overall Cost per Ton | Base + 1000 | Base |
Looking ahead, the success of lost foam casting for torque converter shell castings opens avenues for broader applications in automotive and industrial components. The ability to produce complex, thin-walled geometries with high precision makes it suitable for other shell castings, such as pump housings or transmission cases. Future work could involve advanced simulation techniques, like coupled fluid-structure analysis, to further optimize gating and reduce lead times. Additionally, exploring biodegradable foam materials may enhance sustainability. The formula for overall process efficiency $\eta$ can be defined as:
$$ \eta = \frac{Q_{output}}{Q_{input}} \times 100\% $$
where $Q_{output}$ represents the number of defect-free shell castings, and $Q_{input}$ includes resources like time, energy, and materials. By continuously refining these parameters, the foundry industry can achieve higher yields and lower costs for shell castings.
In conclusion, the adoption of lost foam casting for forklift torque converter shell castings has proven transformative. Through meticulous pattern design, horizontal gating, secondary coating, and computer simulation, we overcame challenges related to deformation and internal defects. The resulting shell castings exhibit superior dimensional accuracy, surface finish, and mechanical properties, with a scrap rate below 1%. This process not only improves product quality but also drives down costs and supports sustainable manufacturing. As I reflect on this journey, it underscores the importance of innovation in casting technologies for advancing shell castings production. The lessons learned here can be applied to other complex components, reinforcing lost foam casting as a key enabler for near-net-shape manufacturing in modern foundries.