
The pursuit of efficient, high-quality production of complex metal components, particularly for time-sensitive sectors like automotive prototyping, perpetually drives innovation in foundry practices. Among the most significant challenges is the manufacture of intricate parts like engine cylinder heads, which feature thin walls, complex internal passages, and isolated thermal masses. Traditional methods for prototyping such sand castings are often prohibitively time-consuming and costly due to the need for pattern and core box fabrication. In my experience, the convergence of Rapid Prototyping (RP) technologies with conventional foundry processes has revolutionized this landscape. Specifically, the integration of Stereolithography (SLA) for patternmaking with traditional sand casting techniques enables a rapid, flexible, and highly accurate manufacturing route ideal for low-volume and prototype production. This article delves into the core of this synergy, focusing on the indispensable role of numerical simulation in validating and optimizing the process for critical components like cylinder heads produced via rapid sand castings.
The fundamental principle of rapid sand castings based on SLA patterns is elegantly straightforward yet powerful. It begins with the creation of a precise three-dimensional digital model of the desired casting. This CAD model serves as the foundation not just for the part itself, but for the entire casting system. Advanced CAD systems specifically tailored for foundry applications allow for the agile design of the complete mold assembly, including gating and feeding systems. This digital design phase is crucial; it is where initial decisions on parting lines, core segmentation, and the basic layout of runners and risers are made. The process flow can be summarized as follows:
- 3D CAD Modeling: Creation of the final part geometry.
- Castings Process CAD Design: Virtual design of molds, cores, gating (pouring basin, sprue, runners, ingates), and feeding (risers) systems.
- Numerical Simulation (CAE): Virtual prototyping to analyze mold filling, solidification, and defect formation.
- SLA Pattern & Core Box Fabrication: Physical realization of the mold components using additive manufacturing.
- Mold Assembly & Sand Casting: Traditional molding, core assembly, pouring, and shakeout.
The true power of this workflow is unlocked in Step 3: Numerical Simulation. Before committing resources to producing physical SLA patterns and conducting costly trial pours, simulation software allows us to peer into the future of the casting process. For sand castings, the primary concerns are achieving a smooth, turbulence-free fill to avoid oxide entrapment and ensuring directional solidification towards effective feeders to minimize shrinkage porosity. Software like ProCAST, which is extensively used in both academia and industry, solves the fundamental governing equations of fluid flow, heat transfer, and solidification physics. The core equations underpinning such simulations include:
Conservation of Mass (Continuity):
$$\nabla \cdot \mathbf{u} = 0$$
where $\mathbf{u}$ is the fluid velocity vector.
Conservation of Momentum (Navier-Stokes with Darcy term for mushy zone):
$$\rho \frac{\partial \mathbf{u}}{\partial t} + \rho (\mathbf{u} \cdot \nabla) \mathbf{u} = -\nabla p + \mu \nabla^2 \mathbf{u} + \rho \mathbf{g} – \frac{\mu}{K} \mathbf{u}$$
Here, $\rho$ is density, $p$ is pressure, $\mu$ is dynamic viscosity, $\mathbf{g}$ is gravity, and $K$ is the permeability of the mushy zone, which becomes critically important as the alloy solidifies.
Conservation of Energy (Heat Transfer):
$$\frac{\partial}{\partial t}(\rho h) = \nabla \cdot (k \nabla T)$$
where $h$ is enthalpy, $k$ is thermal conductivity, and $T$ is temperature. The enthalpy formulation elegantly captures the latent heat release during phase change, a dominant factor in sand castings solidification.
The successful application of these principles to a complex geometry requires meticulous setup. Let’s consider a hypothetical but representative case: an aluminum alloy (e.g., A356, similar to ZL105) cylinder head for a prototype engine. The material properties are paramount for accurate simulation. Key properties for the alloy and the mold material (phenolic urethane-bonded silica sand) are typically defined in material databases.
| Material | Property | Value / Function |
|---|---|---|
| Aluminum Alloy (A356) | Liquidus Temperature ($T_L$) | ~615 °C |
| Solidus Temperature ($T_S$) | ~555 °C | |
| Density ($\rho$) | ~2680 kg/m³ | |
| Latent Heat of Fusion ($L$) | ~389 kJ/kg | |
| Phenolic Urethane Sand Mold | Thermal Conductivity ($k_{mold}$) | ~0.6 – 1.0 W/m·K |
| Heat Capacity ($C_p$) | ~1100 J/kg·K | |
| Density | ~1500 kg/m³ |
The interfacial heat transfer coefficient (IHTC) between the casting and the mold is not a constant but a complex function of air gap formation due to shrinkage. It is often modeled as a temperature-dependent parameter, starting high (e.g., 1000 W/m²·K) when the metal is in perfect contact and dropping significantly (to 100-200 W/m²·K) as an air gap forms.
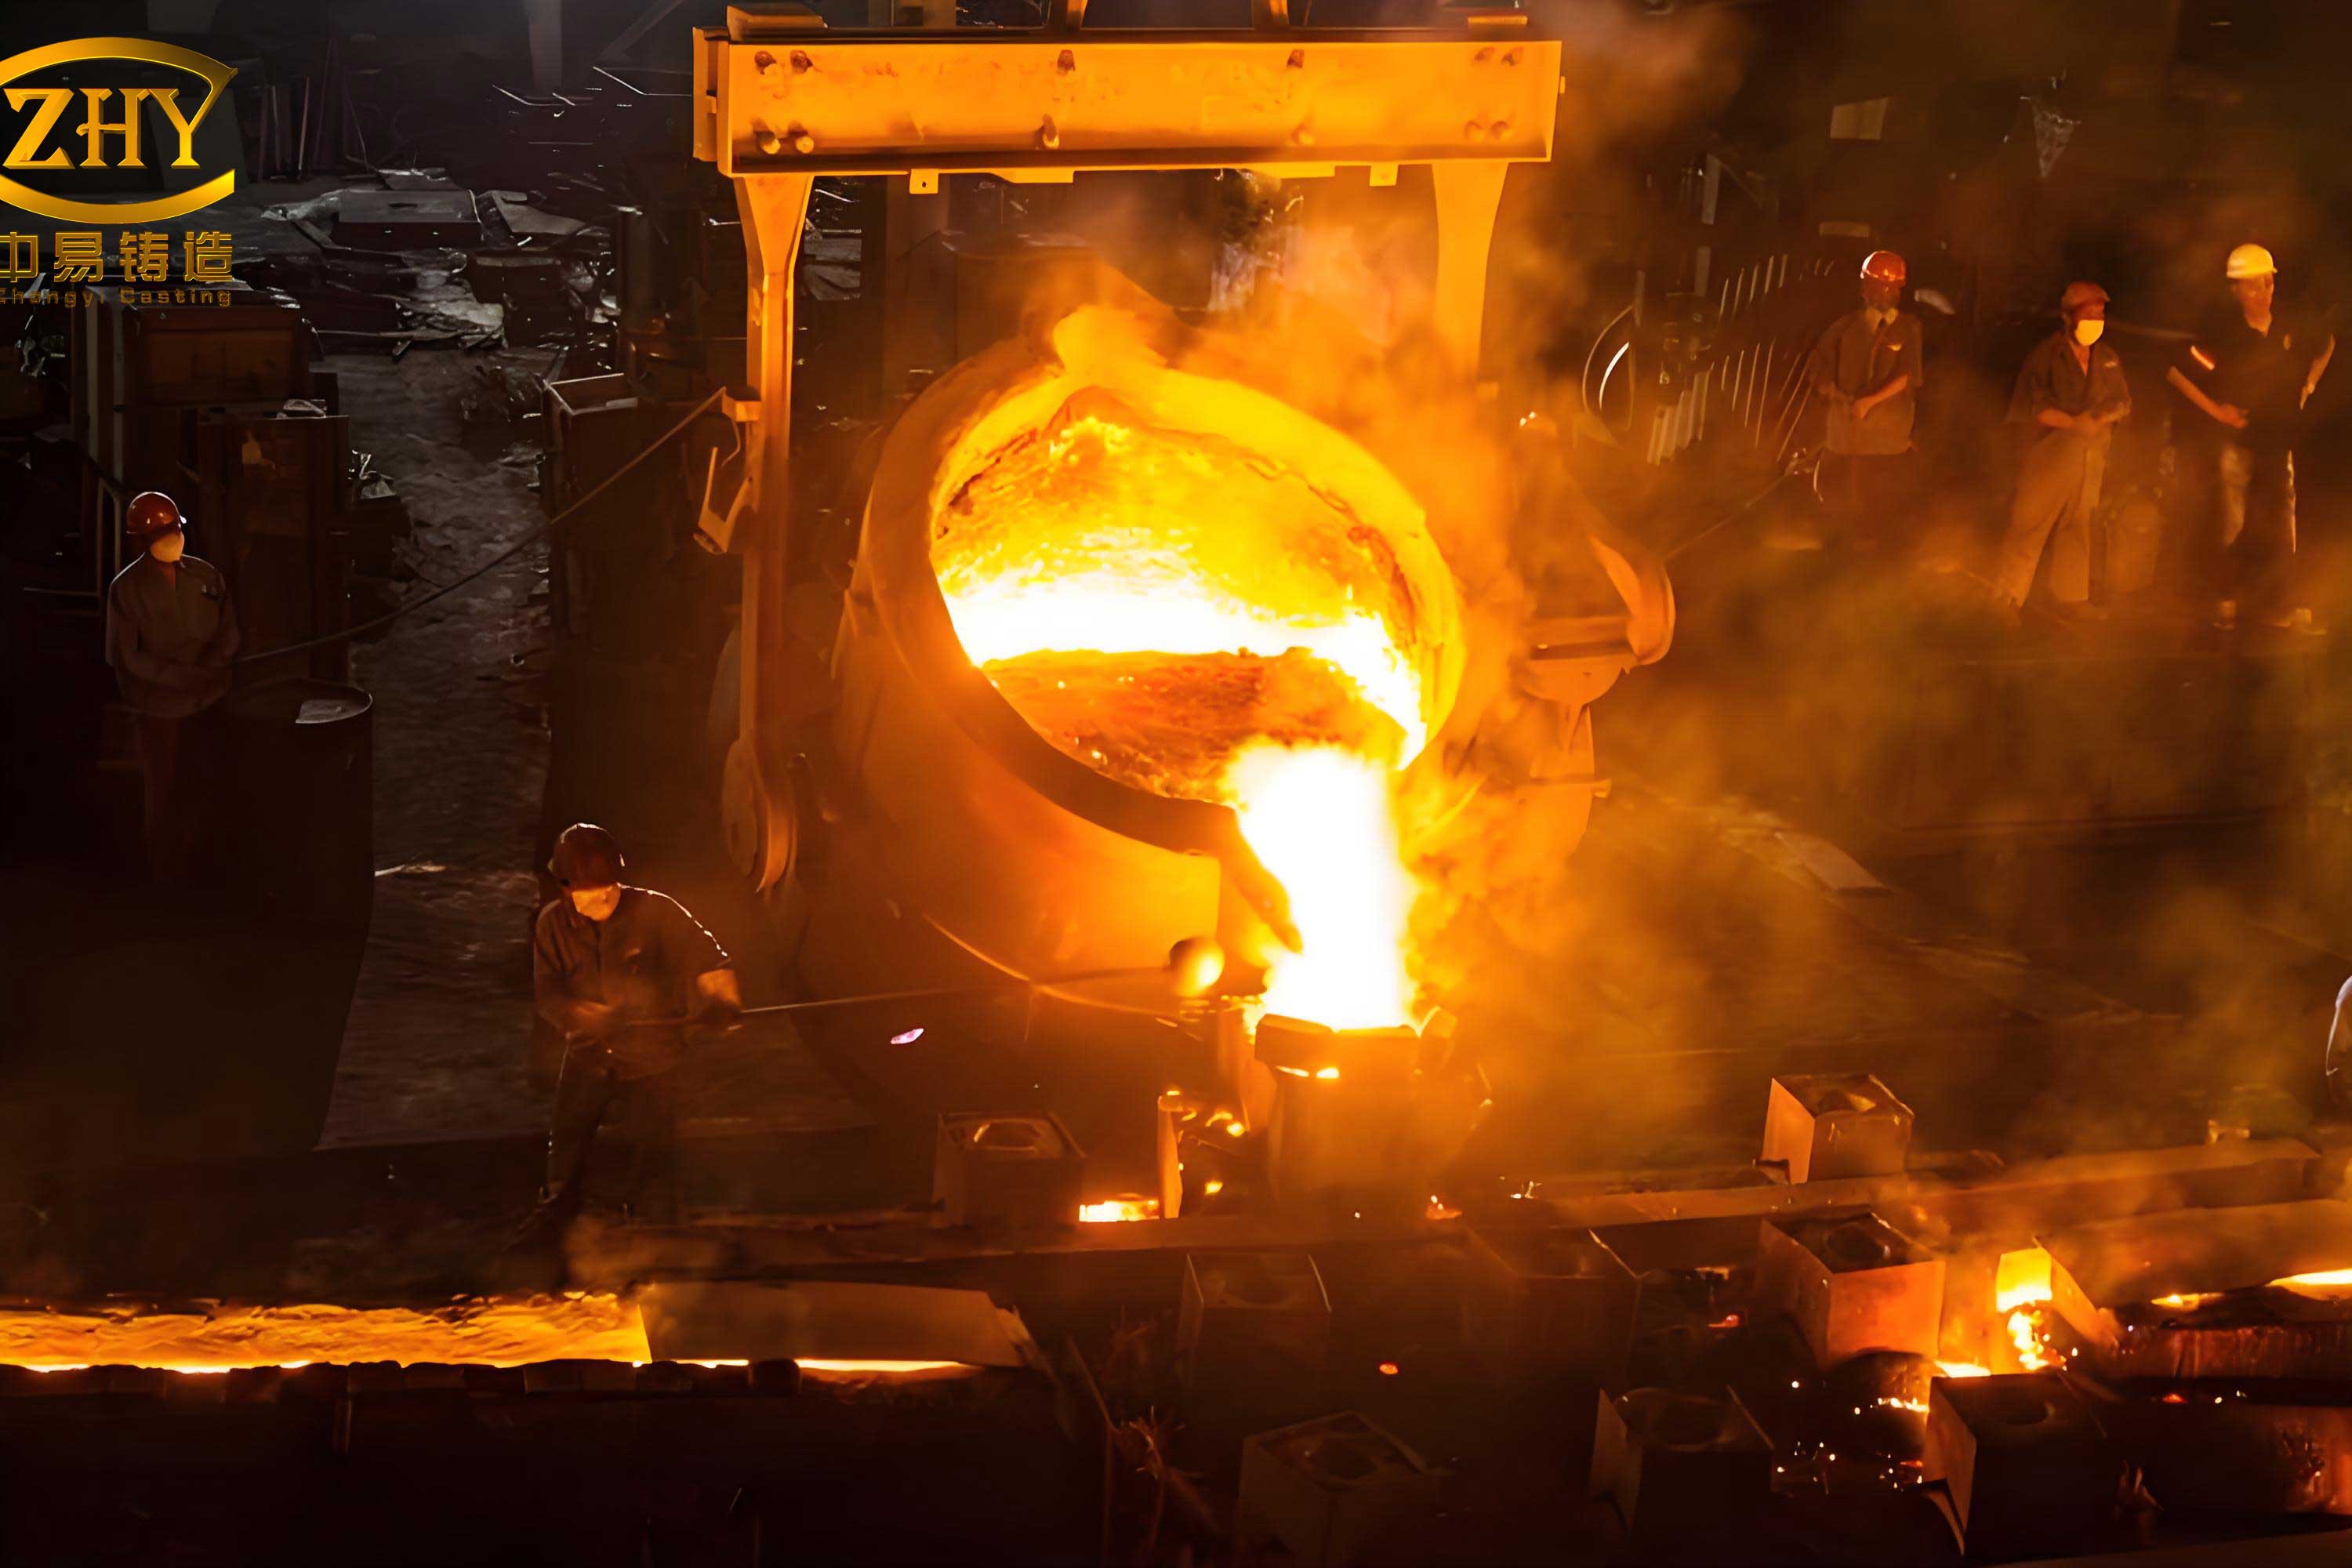
The first critical phase simulated is mold filling. For complex sand castings like a cylinder head, the choice of gating system is vital. A bottom-gating system, where metal enters the mold cavity at its lowest point, is often preferred for aluminum alloys to promote a calm, progressive fill from the bottom up, minimizing turbulence and oxide film entrainment. The simulation outputs, such as fluid front progression and temperature distribution during fill, are examined. An ideal fill shows a steady, upward-moving front without severe splashing or back-flow. The total fill time ($t_{fill}$) can be correlated with the ingate velocity to assess the risk of surface turbulence. A common rule of thumb for aluminum sand castings is to maintain ingate velocities below 0.5 m/s to prevent oxide entrainment.
Following filling, the solidification simulation begins. This is the phase where defects are born. The software calculates the evolution of the solid fraction ($f_s$) from 0 (liquid) to 1 (solid). The primary goal is to achieve directional solidification, where regions closer to the feeders remain liquid longer than remote sections of the casting. This is assessed by analyzing the temperature gradient ($G$) and the local solidification time. Isolated liquid pools, known as “hot spots,” are areas completely surrounded by solid material; they are high-risk zones for macro-shrinkage porosity. The simulation visually identifies these regions by tracking the liquid fraction over time.
The prediction of shrinkage porosity, the most common defect in sand castings, often relies on criteria functions that combine thermal parameters. One of the most widely used is the Niyama criterion ($N_y$), which is calculated post-solidification:
$$N_y = \frac{G}{\sqrt{\dot T}}$$
where $\dot T$ is the cooling rate. Areas with a Niyama value below a critical threshold (e.g., 1 °C¹/²·s¹/² for aluminum alloys) are predicted to be susceptible to microporosity. More advanced models directly solve for pore nucleation and growth based on pressure drop in the mushy zone, described by Darcy’s law and the continuity equation for the liquid phase.
Let’s illustrate with a detailed, simulated case study of our aluminum cylinder head. After CAD design of a one-side bottom gating system with top risers, the model is discretized into a finite element mesh. A mesh sensitivity analysis is performed to ensure results are independent of element size. Typical mesh sizes for such sand castings range from 1-3 mm, resulting in several hundred thousand to millions of elements.
| Simulation Parameter | Setting |
|---|---|
| Pouring Temperature | 700 °C |
| Mold Initial Temperature | 25 °C |
| Interfacial Heat Transfer | Temperature-dependent function |
| Total Number of Elements | ~500,000 |
| Simulated Process Time | Filling + 600s of Solidification |
The filling sequence confirms the benefits of bottom gating. The metal rises smoothly, with the liquid front advancement being nearly horizontal at each time step, as shown in fill fraction contours. The total fill time is approximately 16 seconds, with the final regions to fill being the top risers, confirming adequate metallostatic pressure.
The solidification analysis reveals the thermal history. The thin outer walls and internal fins solidify first, followed by the thicker sections around the valve seats and ports. The temperature gradient vectors clearly show heat extraction moving from the casting center towards the mold walls and, most importantly, towards the risers. A critical output is the “isolated liquid” or “last-to-freeze” map. In a well-designed system, the last points to solidify should be within the risers, not in the casting body. The simulated results for this design show precisely that: the final liquid pools are confined to the feeder necks and risers, indicating they are effectively performing their function.
The porosity prediction module is then activated. The results might show a porosity percentage distribution. Key findings for a successful design would be:
- Maximum porosity concentration located within the risers (which are removed after casting).
- Porosity in the critical casting body below an acceptable threshold (e.g., < 0.1% volume fraction or classified as “dispersed microporosity”).
- No predicted macro-shrinkage cavities in the main casting.
The quantitative analysis can be summarized in a result table for key zones:
| Casting Region | Solidification Time [s] | Min. Niyama Value [°C¹/²·s¹/²] | Predicted Porosity Level |
|---|---|---|---|
| Thin Wall Section | 45 | 4.2 | None |
| Valve Seat (Thick Section) | 210 | 1.5 | Very Low, Dispersed |
| Main Riser | 380 | 0.3 | High (Intentional) |
| Ingate Junction | 180 | 1.8 | Low |
This virtual prototyping cycle is iterative. If the initial simulation reveals a hot spot in the casting or excessive turbulence during filling, the CAD model is modified—perhaps by relocating a riser, adding a chilling pad in the sand mold, or modifying the runner geometry. The simulation is then re-run to verify the improvement. This loop continues until the predicted casting quality meets all specified criteria. Only after this virtual validation is complete are the SLA patterns and core boxes manufactured. This drastically reduces the number of physical trial casts required, saving immense amounts of time, material, and energy.
The benefits of applying numerical simulation to rapid sand castings are profound and multi-faceted:
- Defect Prediction and Mitigation: Early identification of shrinkage, porosity, cold shuts, and inclusions allows for pre-emptive design corrections.
- Optimization of Feeding System: Risers can be sized and placed with precision, minimizing yield loss (ratio of casting weight to total poured weight) while ensuring soundness.
- Reduced Lead Time and Cost: The number of physical prototypes is minimized, accelerating the product development cycle for complex sand castings.
- Process Understanding: It provides deep insight into the thermal and flow behavior that is nearly impossible to obtain experimentally.
In conclusion, the marriage of Rapid Prototyping for patternmaking and advanced numerical simulation represents a paradigm shift for producing complex, high-integrity metal components. For sand castings, particularly in prototyping and small-batch production, this synergy is transformative. The simulation acts as a digital foundry, where designs are tested, optimized, and validated under virtual conditions that closely mirror physics. It empowers foundry engineers to make informed decisions, ensuring that when the first molten metal is poured into the rapid sand mold, the outcome is not left to chance but is the assured result of a comprehensively engineered process. This digital thread—from CAD to CAE to physical SLA pattern—is the cornerstone of agile, responsive, and high-quality manufacturing for the complex sand castings demanded by modern industry.